case packing equipment
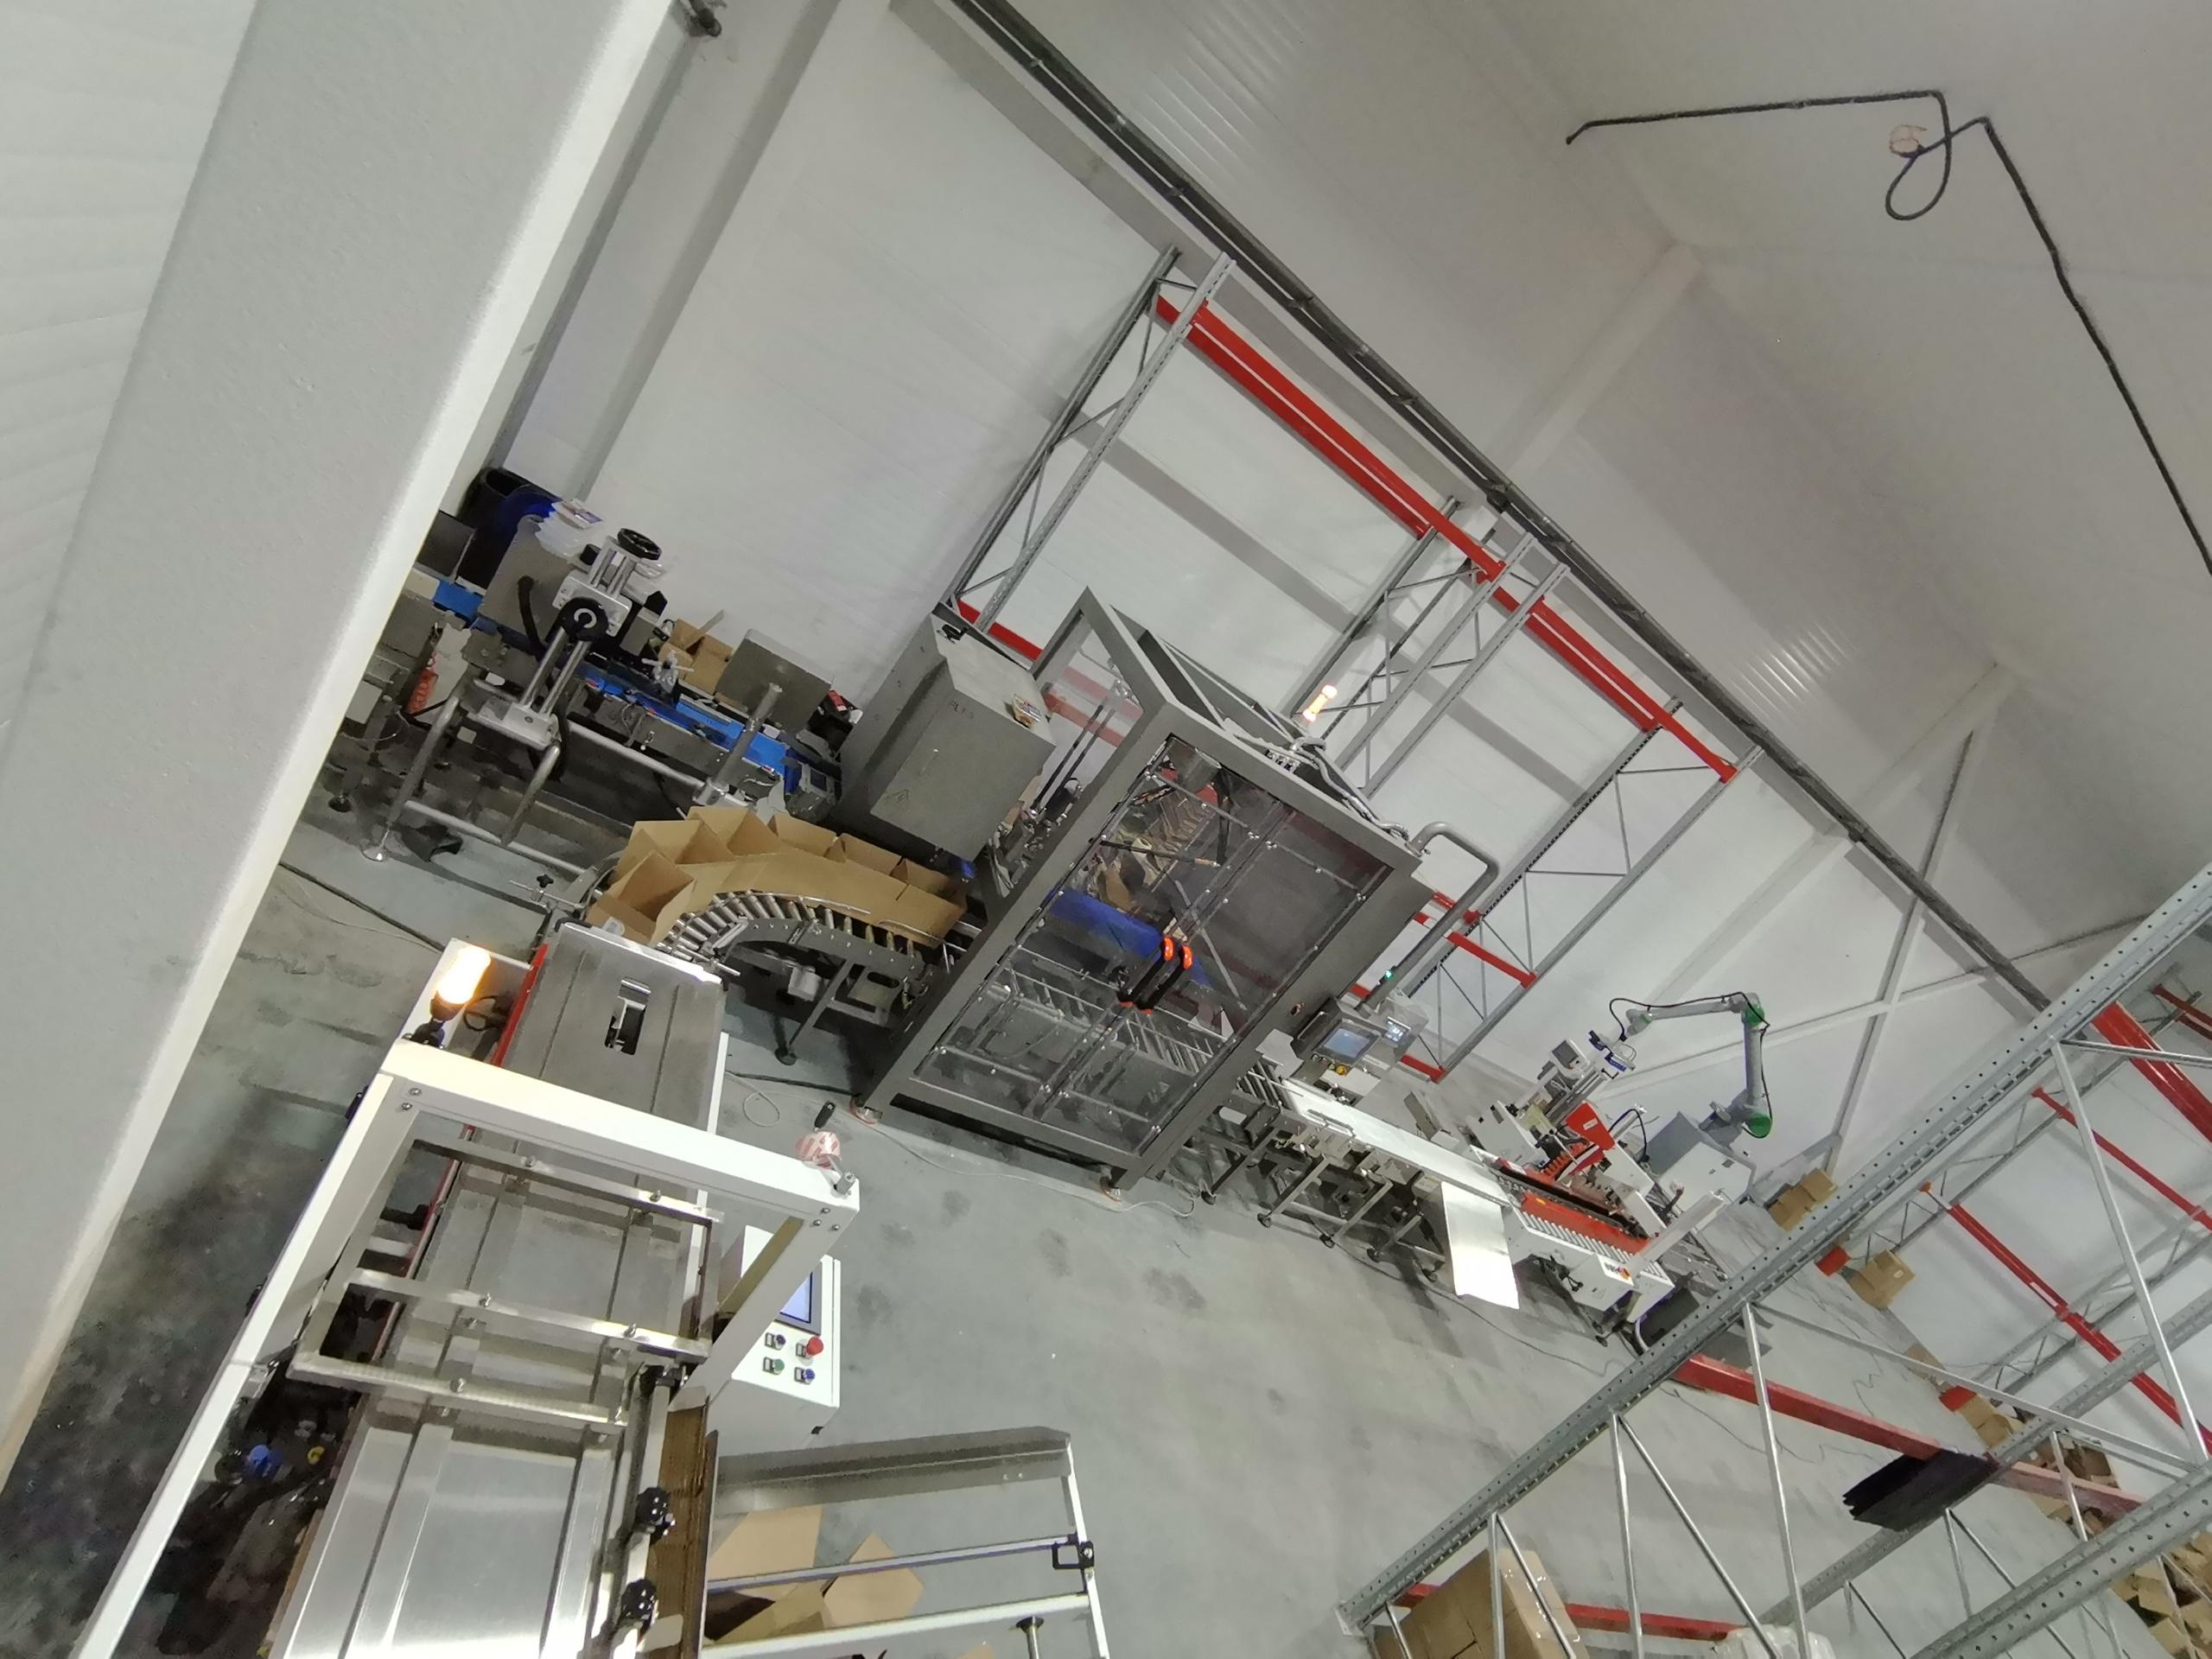
Case packing equipment represents a critical automation solution designed to streamline packaging operations across various industries. This specialized machinery automates the process of placing products into cases or cartons, significantly enhancing production efficiency and consistency. Case packing equipment handles diverse product types, from bottles and cans to boxes and pharmaceutical items, making it an indispensable asset for modern manufacturing facilities.
The primary function of case packing equipment involves automatically grouping individual products into predetermined case configurations. This process includes product detection, alignment, placement, and case closure, all executed with precision timing. Advanced case packing equipment utilizes intelligent sensors and vision systems to ensure accurate product positioning and quality control throughout the packaging cycle.
Technological features integrated into contemporary case packing equipment include servo-driven actuators, programmable logic controllers, and high-speed mechanical systems. These components work harmoniously to achieve throughput rates ranging from dozens to thousands of cases per hour, depending on product specifications and system configuration. Case packing equipment incorporates flexible tooling systems that allow rapid changeovers between different product sizes and case formats.
Applications for case packing equipment span numerous sectors including beverage production, food manufacturing, pharmaceuticals, cosmetics, and consumer goods. The versatility of case packing equipment makes it suitable for both small-scale operations and large-scale industrial production environments. By implementing case packing equipment, manufacturers dramatically reduce labor costs, minimize packaging errors, and optimize warehouse space utilization while maintaining consistent product presentation.

 EN


