case packing system
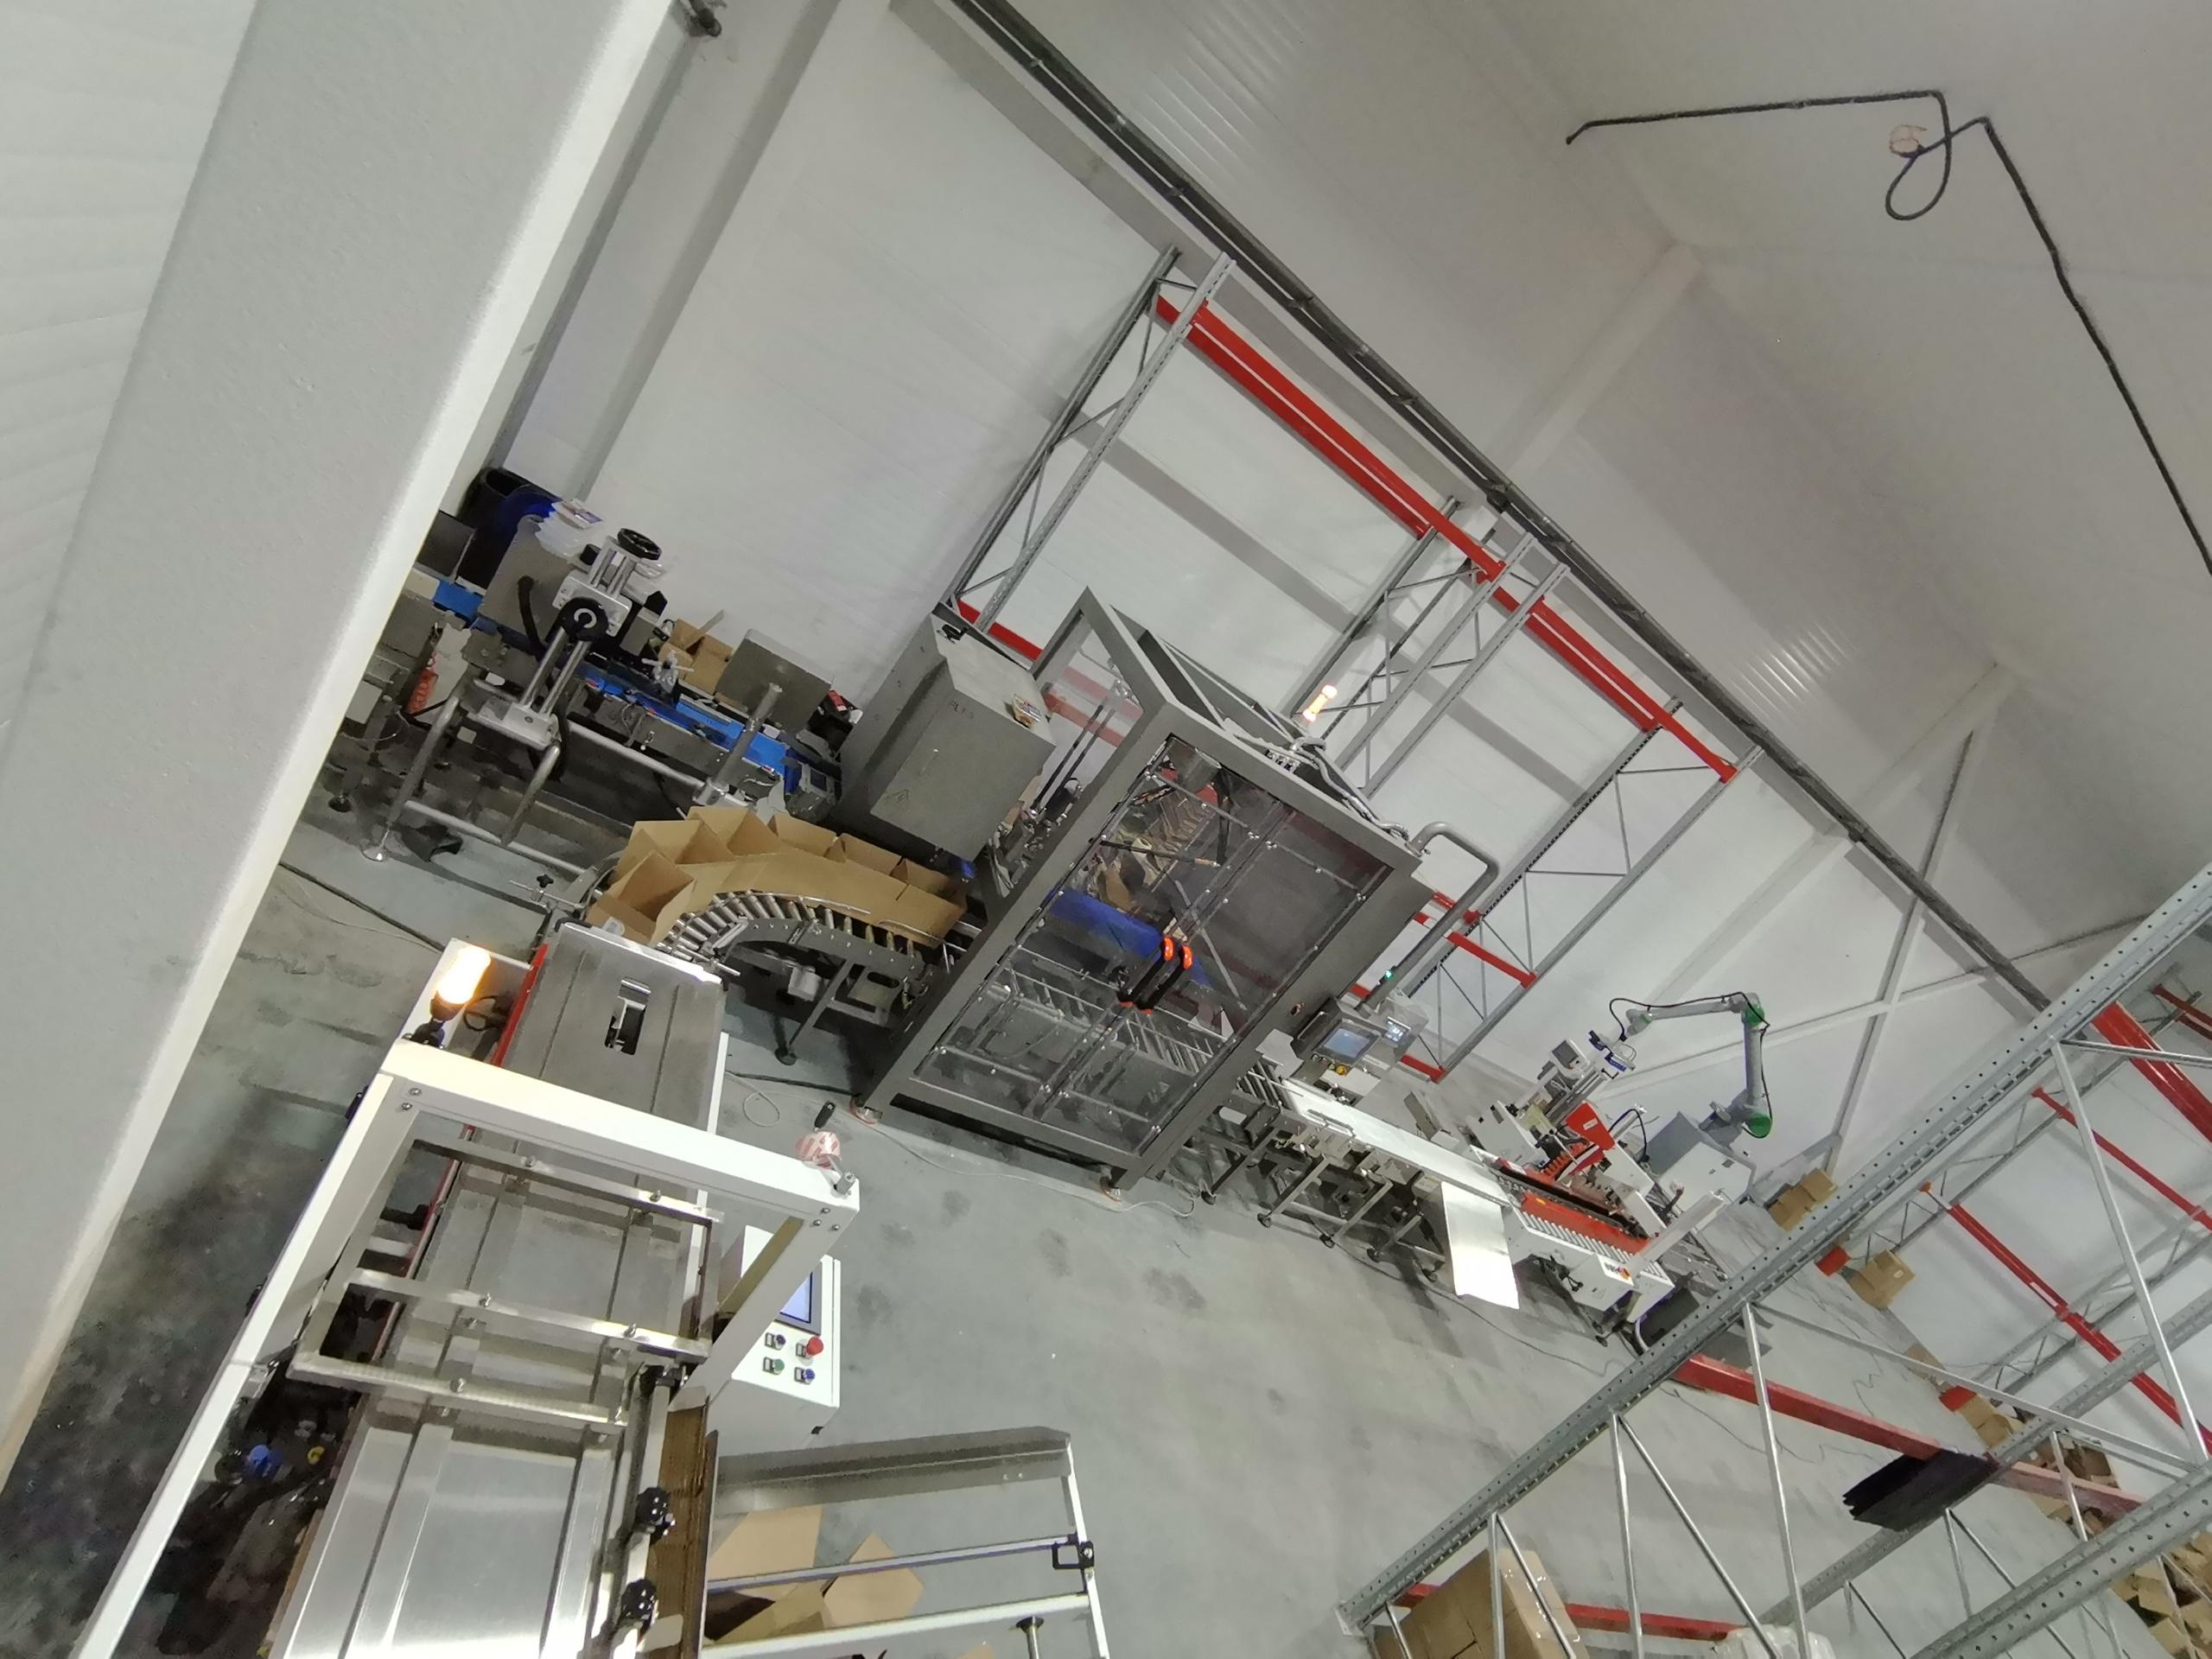
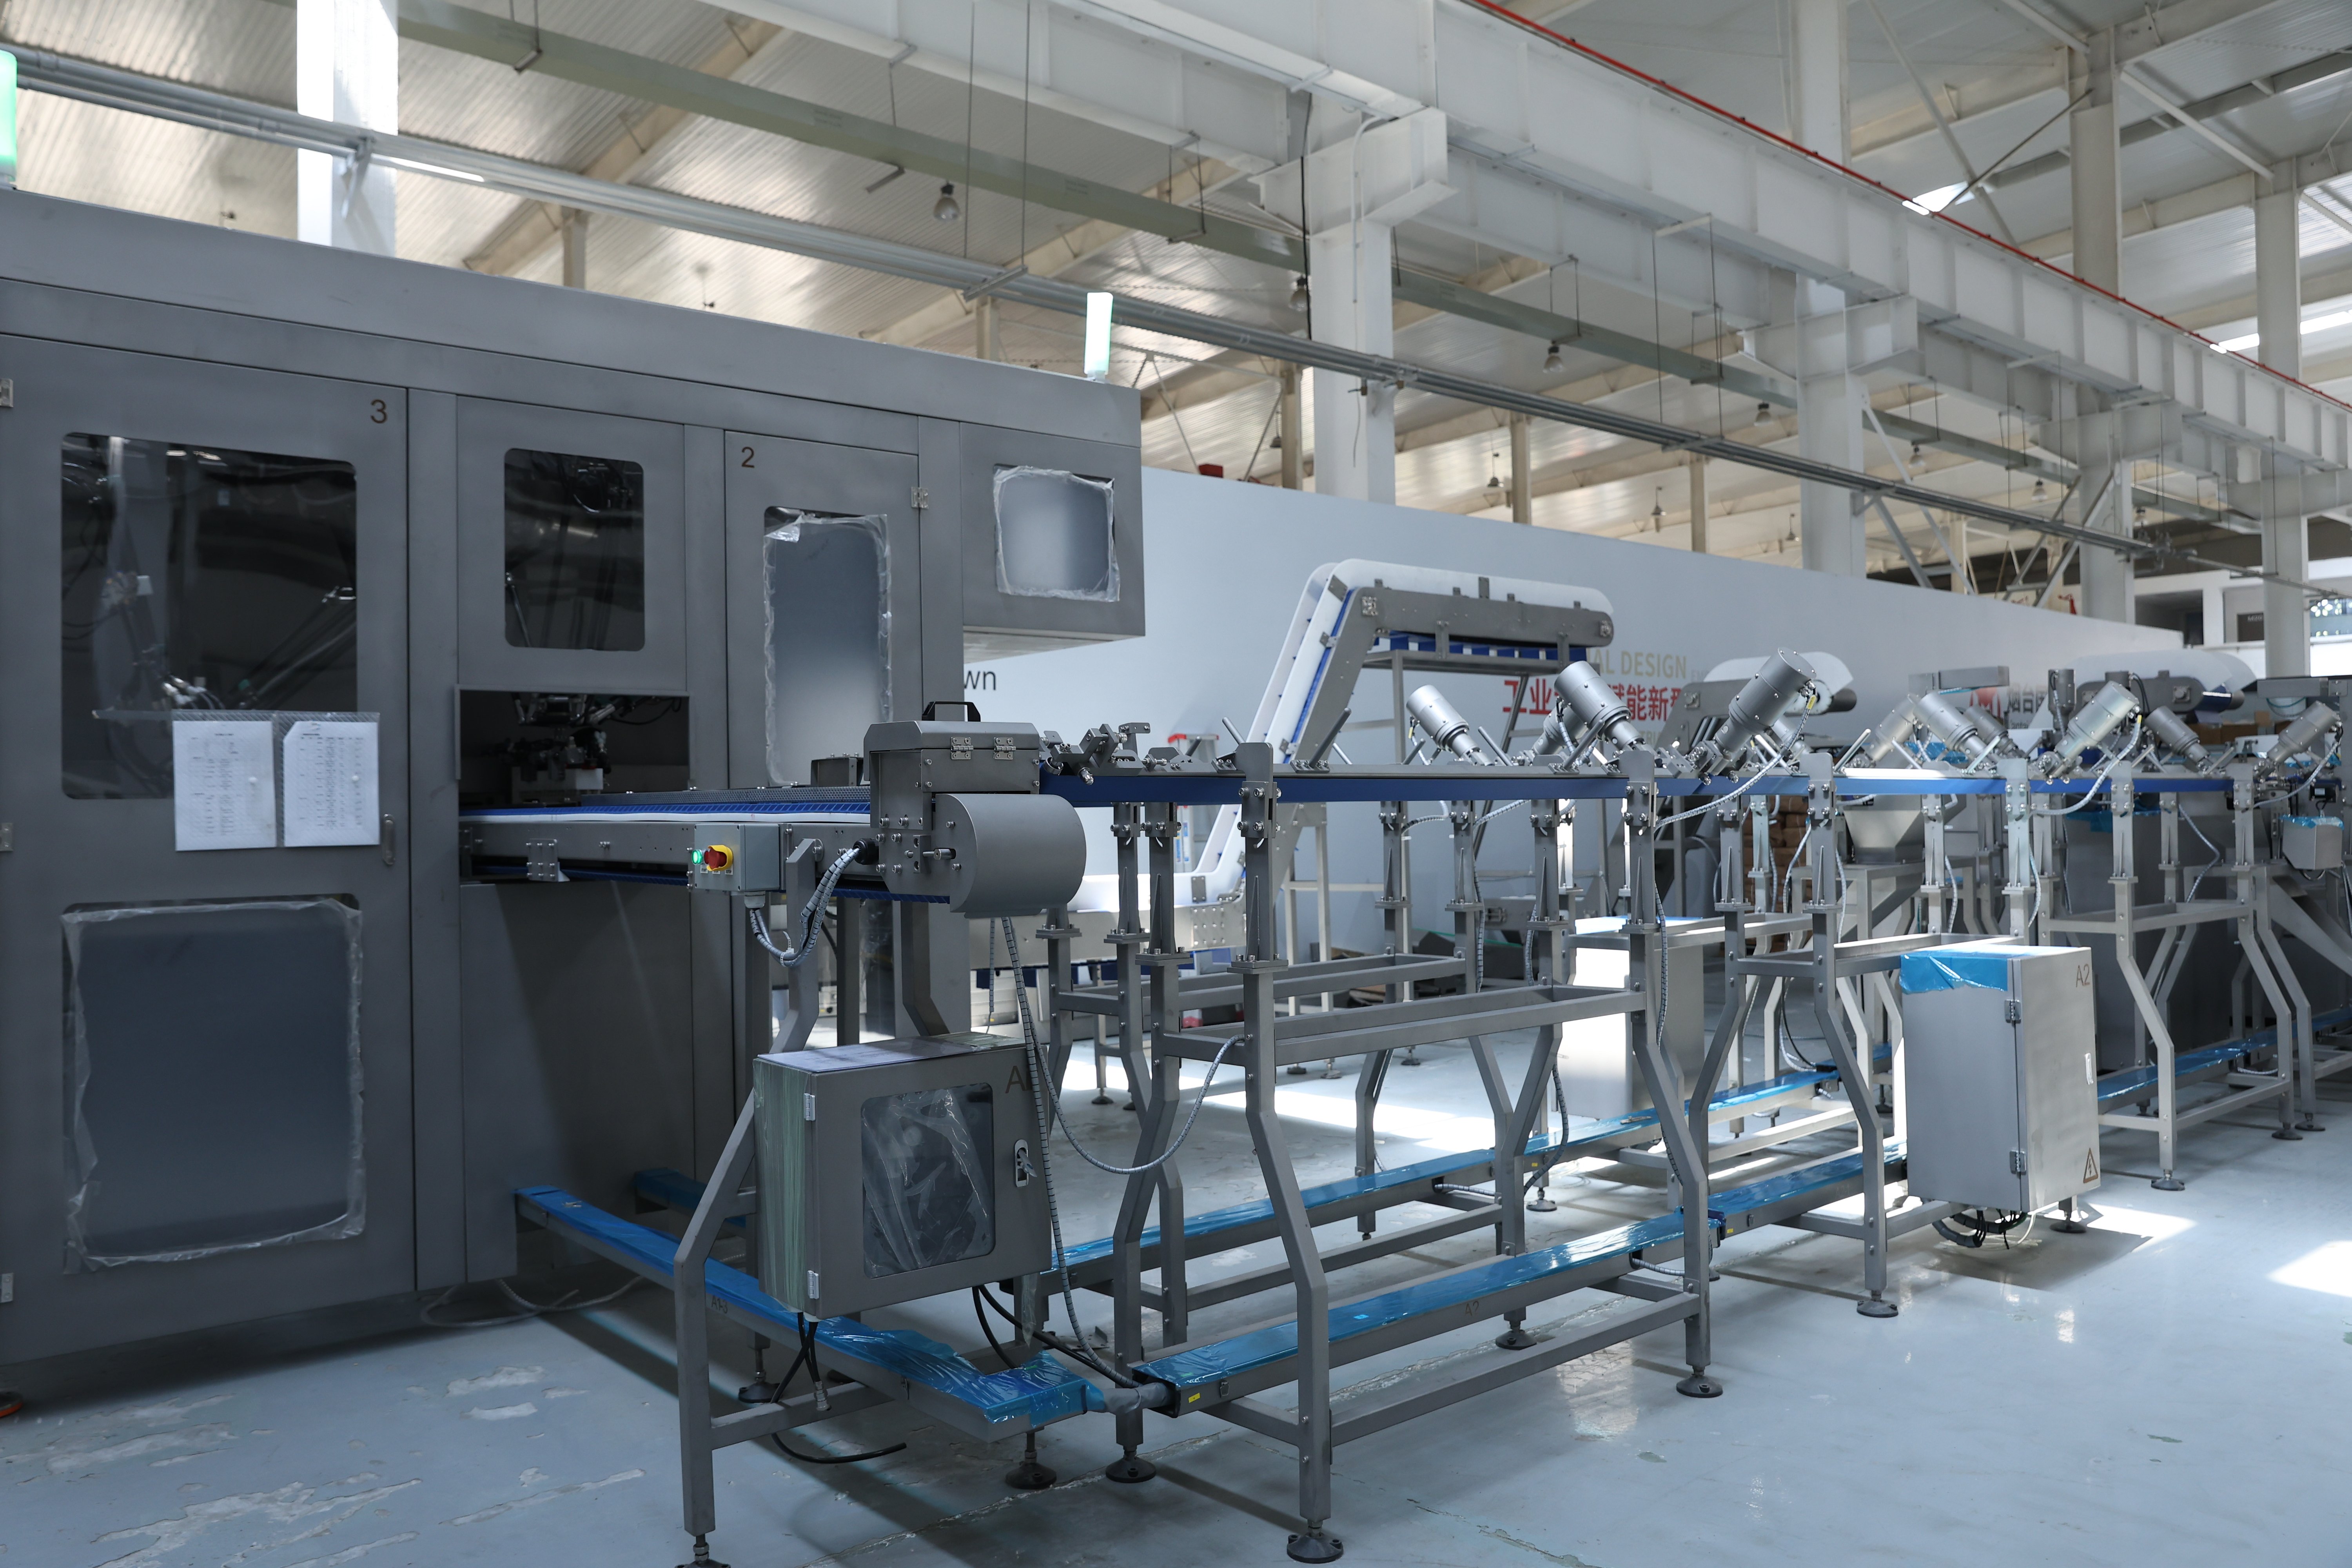
A case packing system represents an automated solution designed to streamline packaging operations by efficiently organizing and packing products into cases for storage and distribution. This case packing system combines mechanical precision with intelligent controls to handle various product types and case sizes seamlessly. The case packing system operates through multiple integrated stages, beginning with product feeding, alignment, and arrangement before final case closure and sealing.
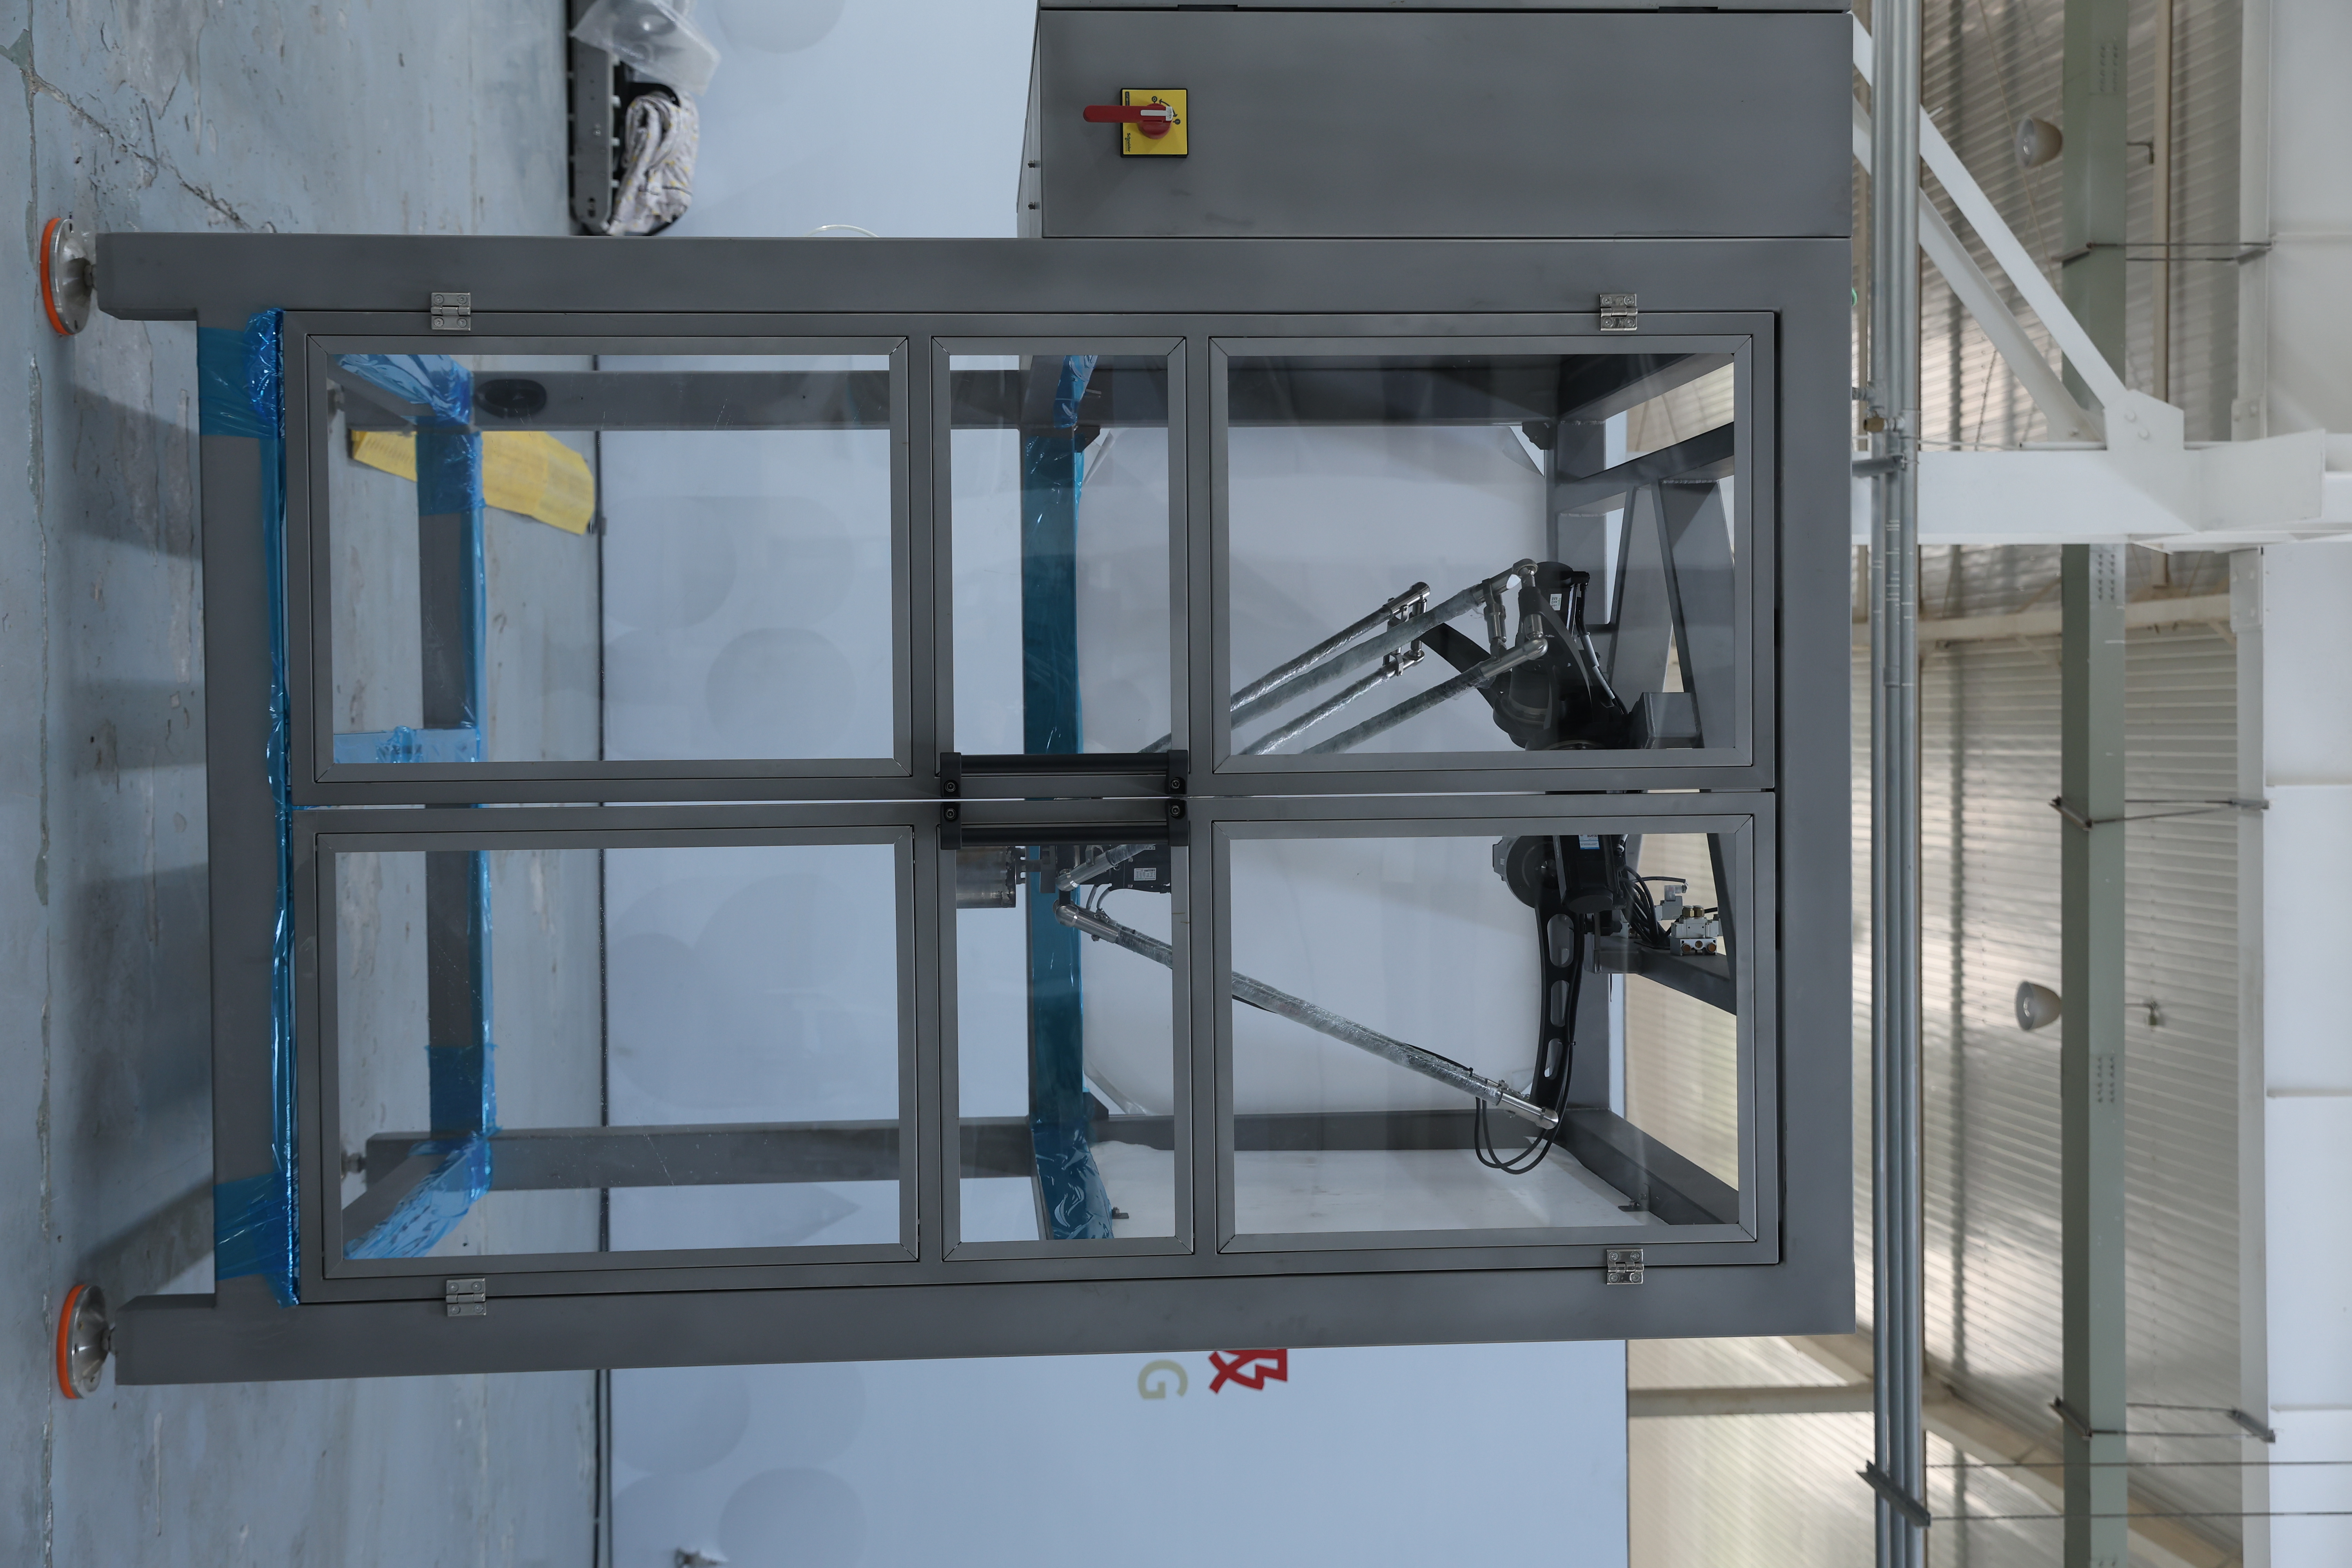
Technologically, a modern case packing system incorporates advanced sensors, programmable logic controllers, and vision systems to ensure accurate product placement and case management. These components work together to minimize errors while maximizing throughput. The case packing system utilizes modular design principles, allowing customization for different packaging requirements without extensive reconfiguration. High-speed conveyor systems integrated into the case packing system transport products smoothly through each processing stage.
Applications for a case packing system span numerous industries including food and beverage, pharmaceuticals, cosmetics, electronics, and manufacturing. The case packing system excels in environments requiring consistent, rapid packaging of uniform or varied products. Businesses implementing a case packing system benefit from increased productivity and reduced labor costs. Whether handling fragile items or bulk goods, the case packing system adapts to specific operational needs while maintaining quality standards and compliance requirements throughout the packaging workflow.

 EN


