carton case packer
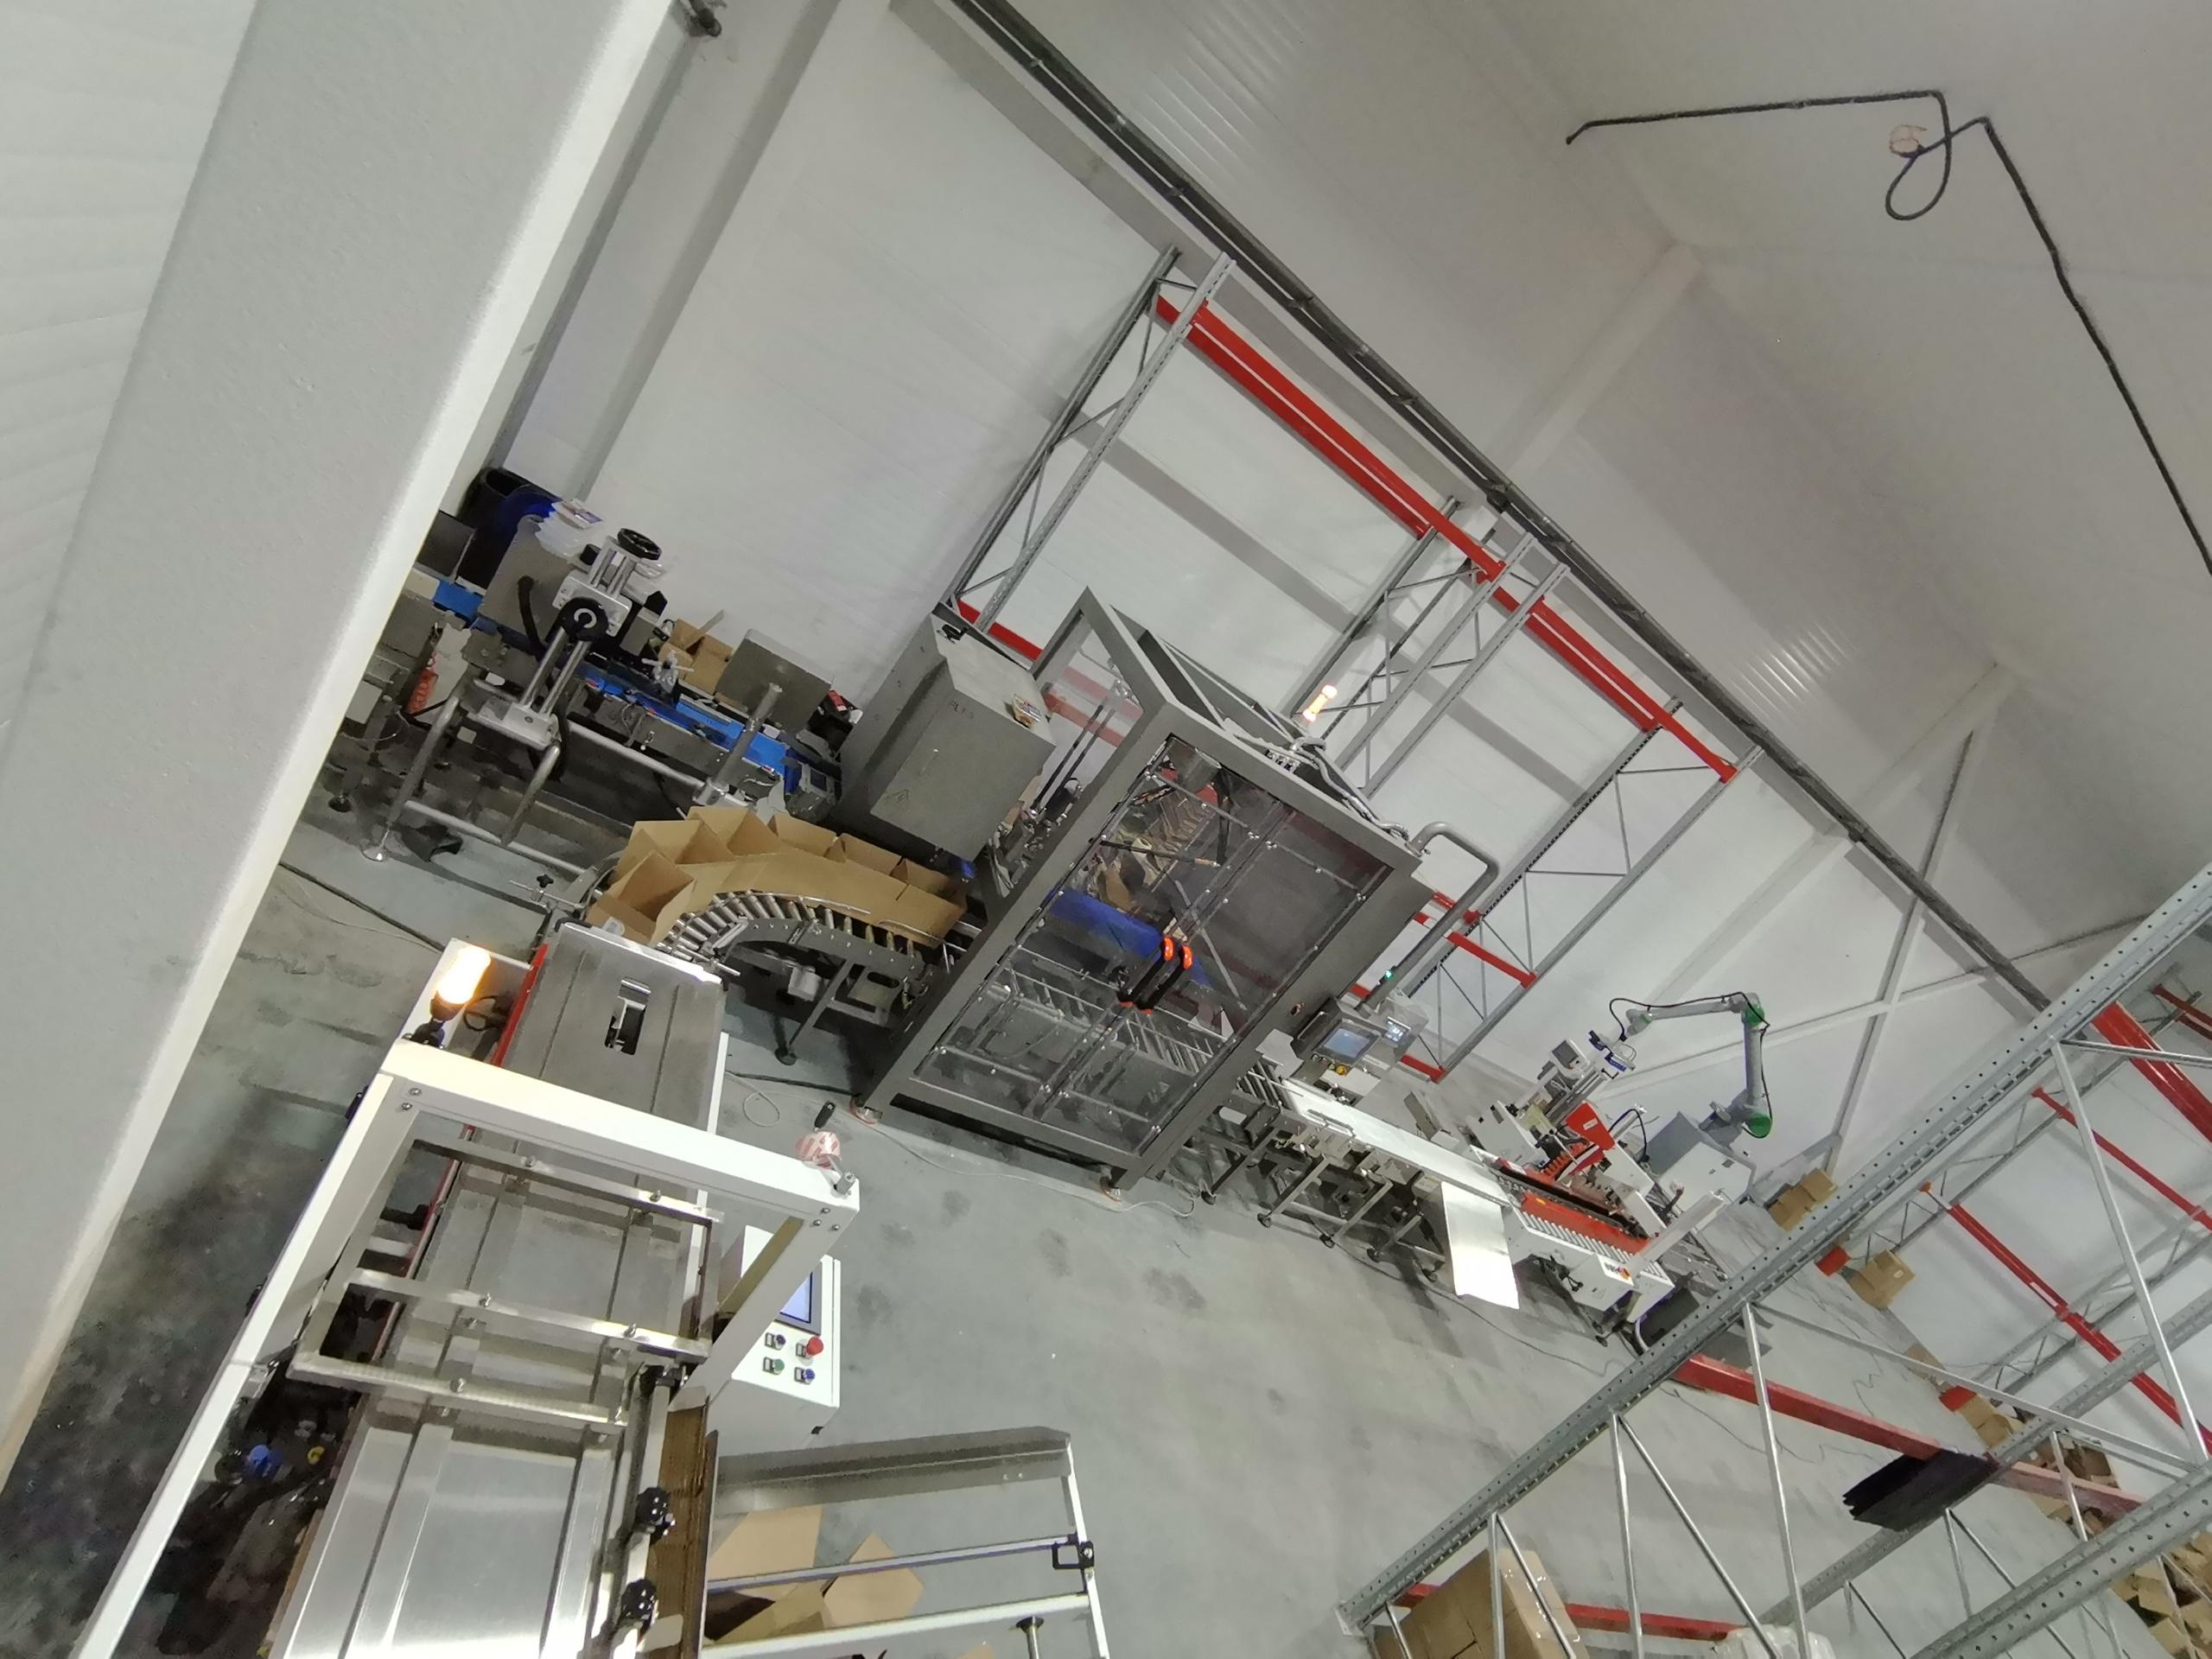
A carton case packer is an automated packaging machine designed to streamline the process of placing products into cartons and cases for storage, shipping, and retail distribution. This innovative equipment serves as a critical component in modern manufacturing and logistics operations across diverse industries including food and beverage, pharmaceuticals, electronics, and consumer goods.
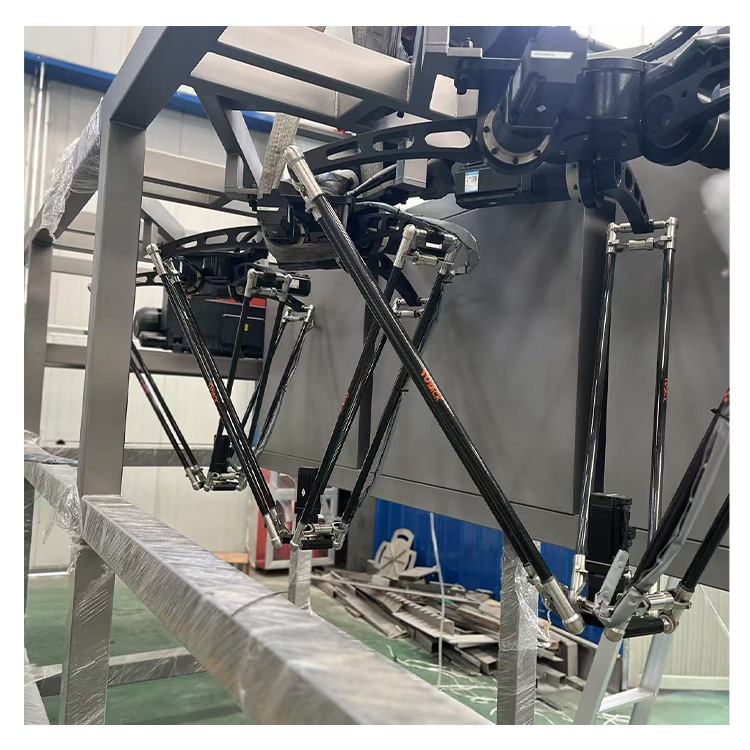
The carton case packer functions by automatically picking items from a production line and precisely positioning them into pre-formed cartons or cases according to programmed specifications. The machine handles various product sizes, shapes, and weights with remarkable accuracy and consistency. Advanced technological features include servo-driven motion systems, intelligent vision recognition technology, and programmable logic controllers that enable flexible operation across multiple product types.
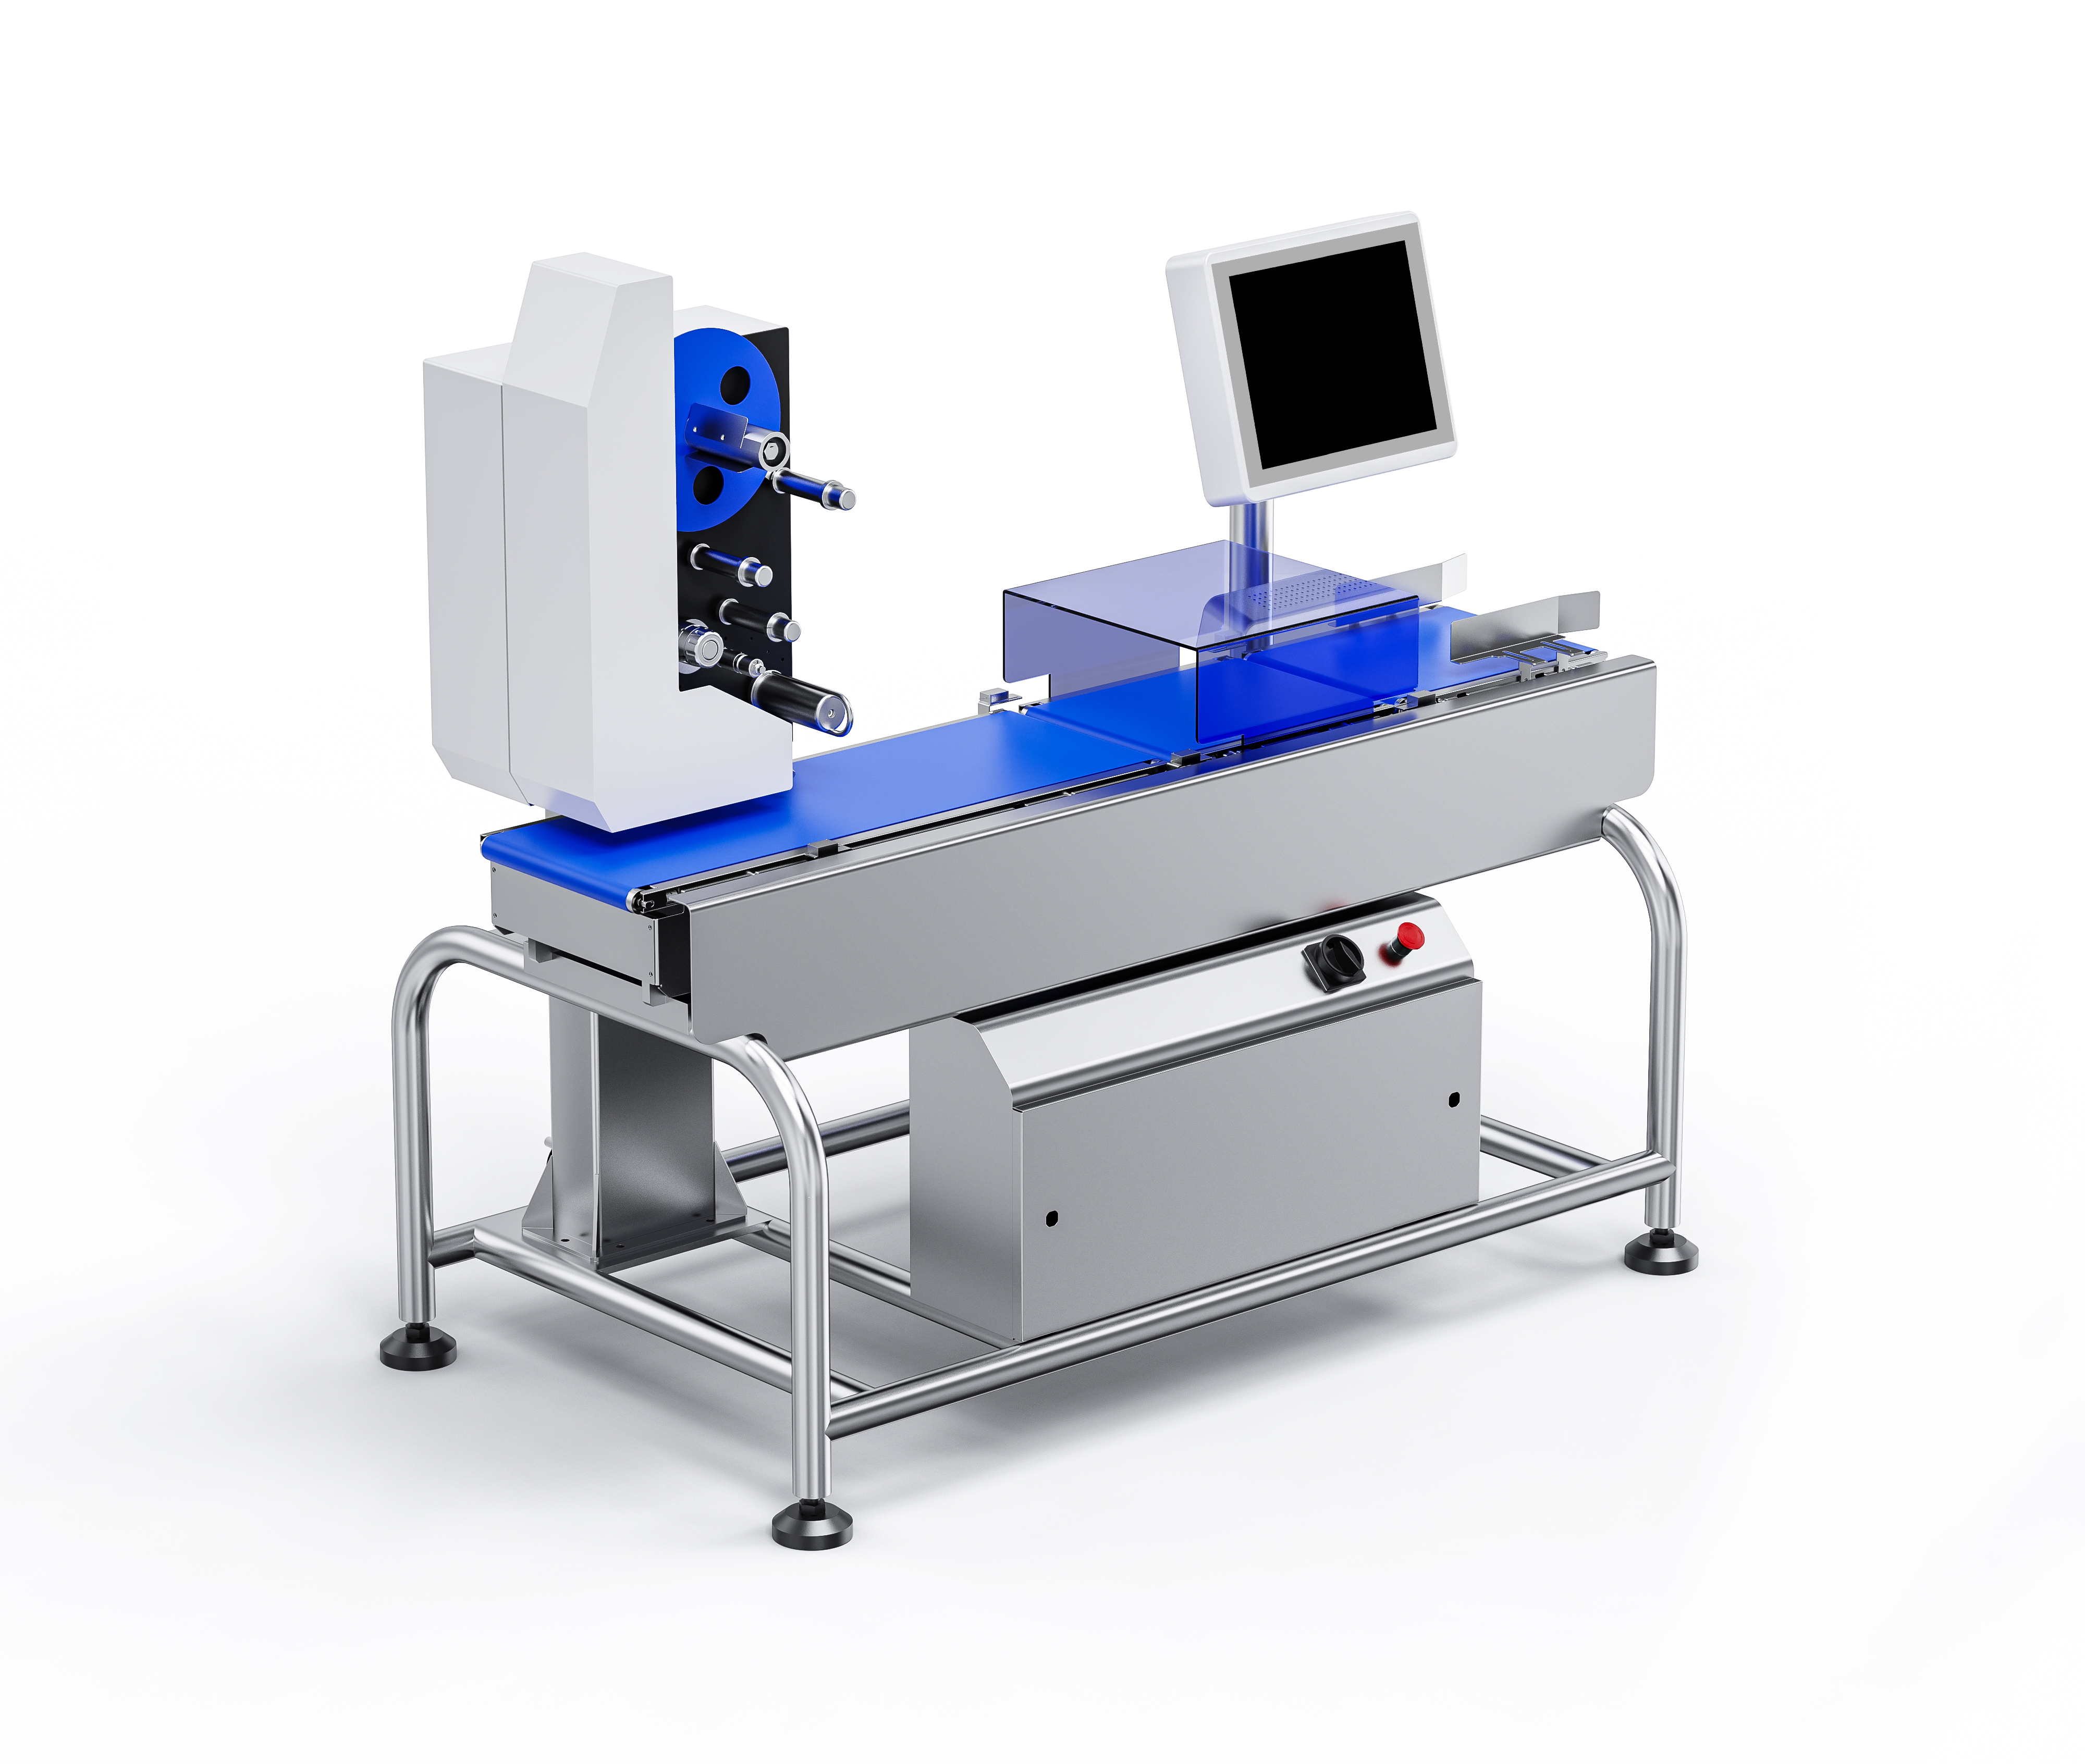
Key technological features of a carton case packer encompass high-speed processing capabilities, adjustable infeed systems, and customizable loading patterns. The equipment incorporates safety sensors, emergency stop mechanisms, and user-friendly control interfaces. Modern carton case packer systems integrate seamlessly with existing production lines, offering scalability and compatibility with various carton dimensions and materials.
Applications extend across numerous sectors where efficient packaging is essential. Manufacturers utilize carton case packer equipment for beverage distribution, pharmaceutical packaging, retail goods preparation, and industrial product containment. The carton case packer significantly reduces labor costs, minimizes product damage, and accelerates production throughput. Businesses benefit from improved operational efficiency, enhanced consistency, and reduced packaging waste. Whether operating in high-volume facilities or specialized production environments, carton case packer technology delivers measurable performance improvements and operational advantages.

 EN


