automated material handling solutions
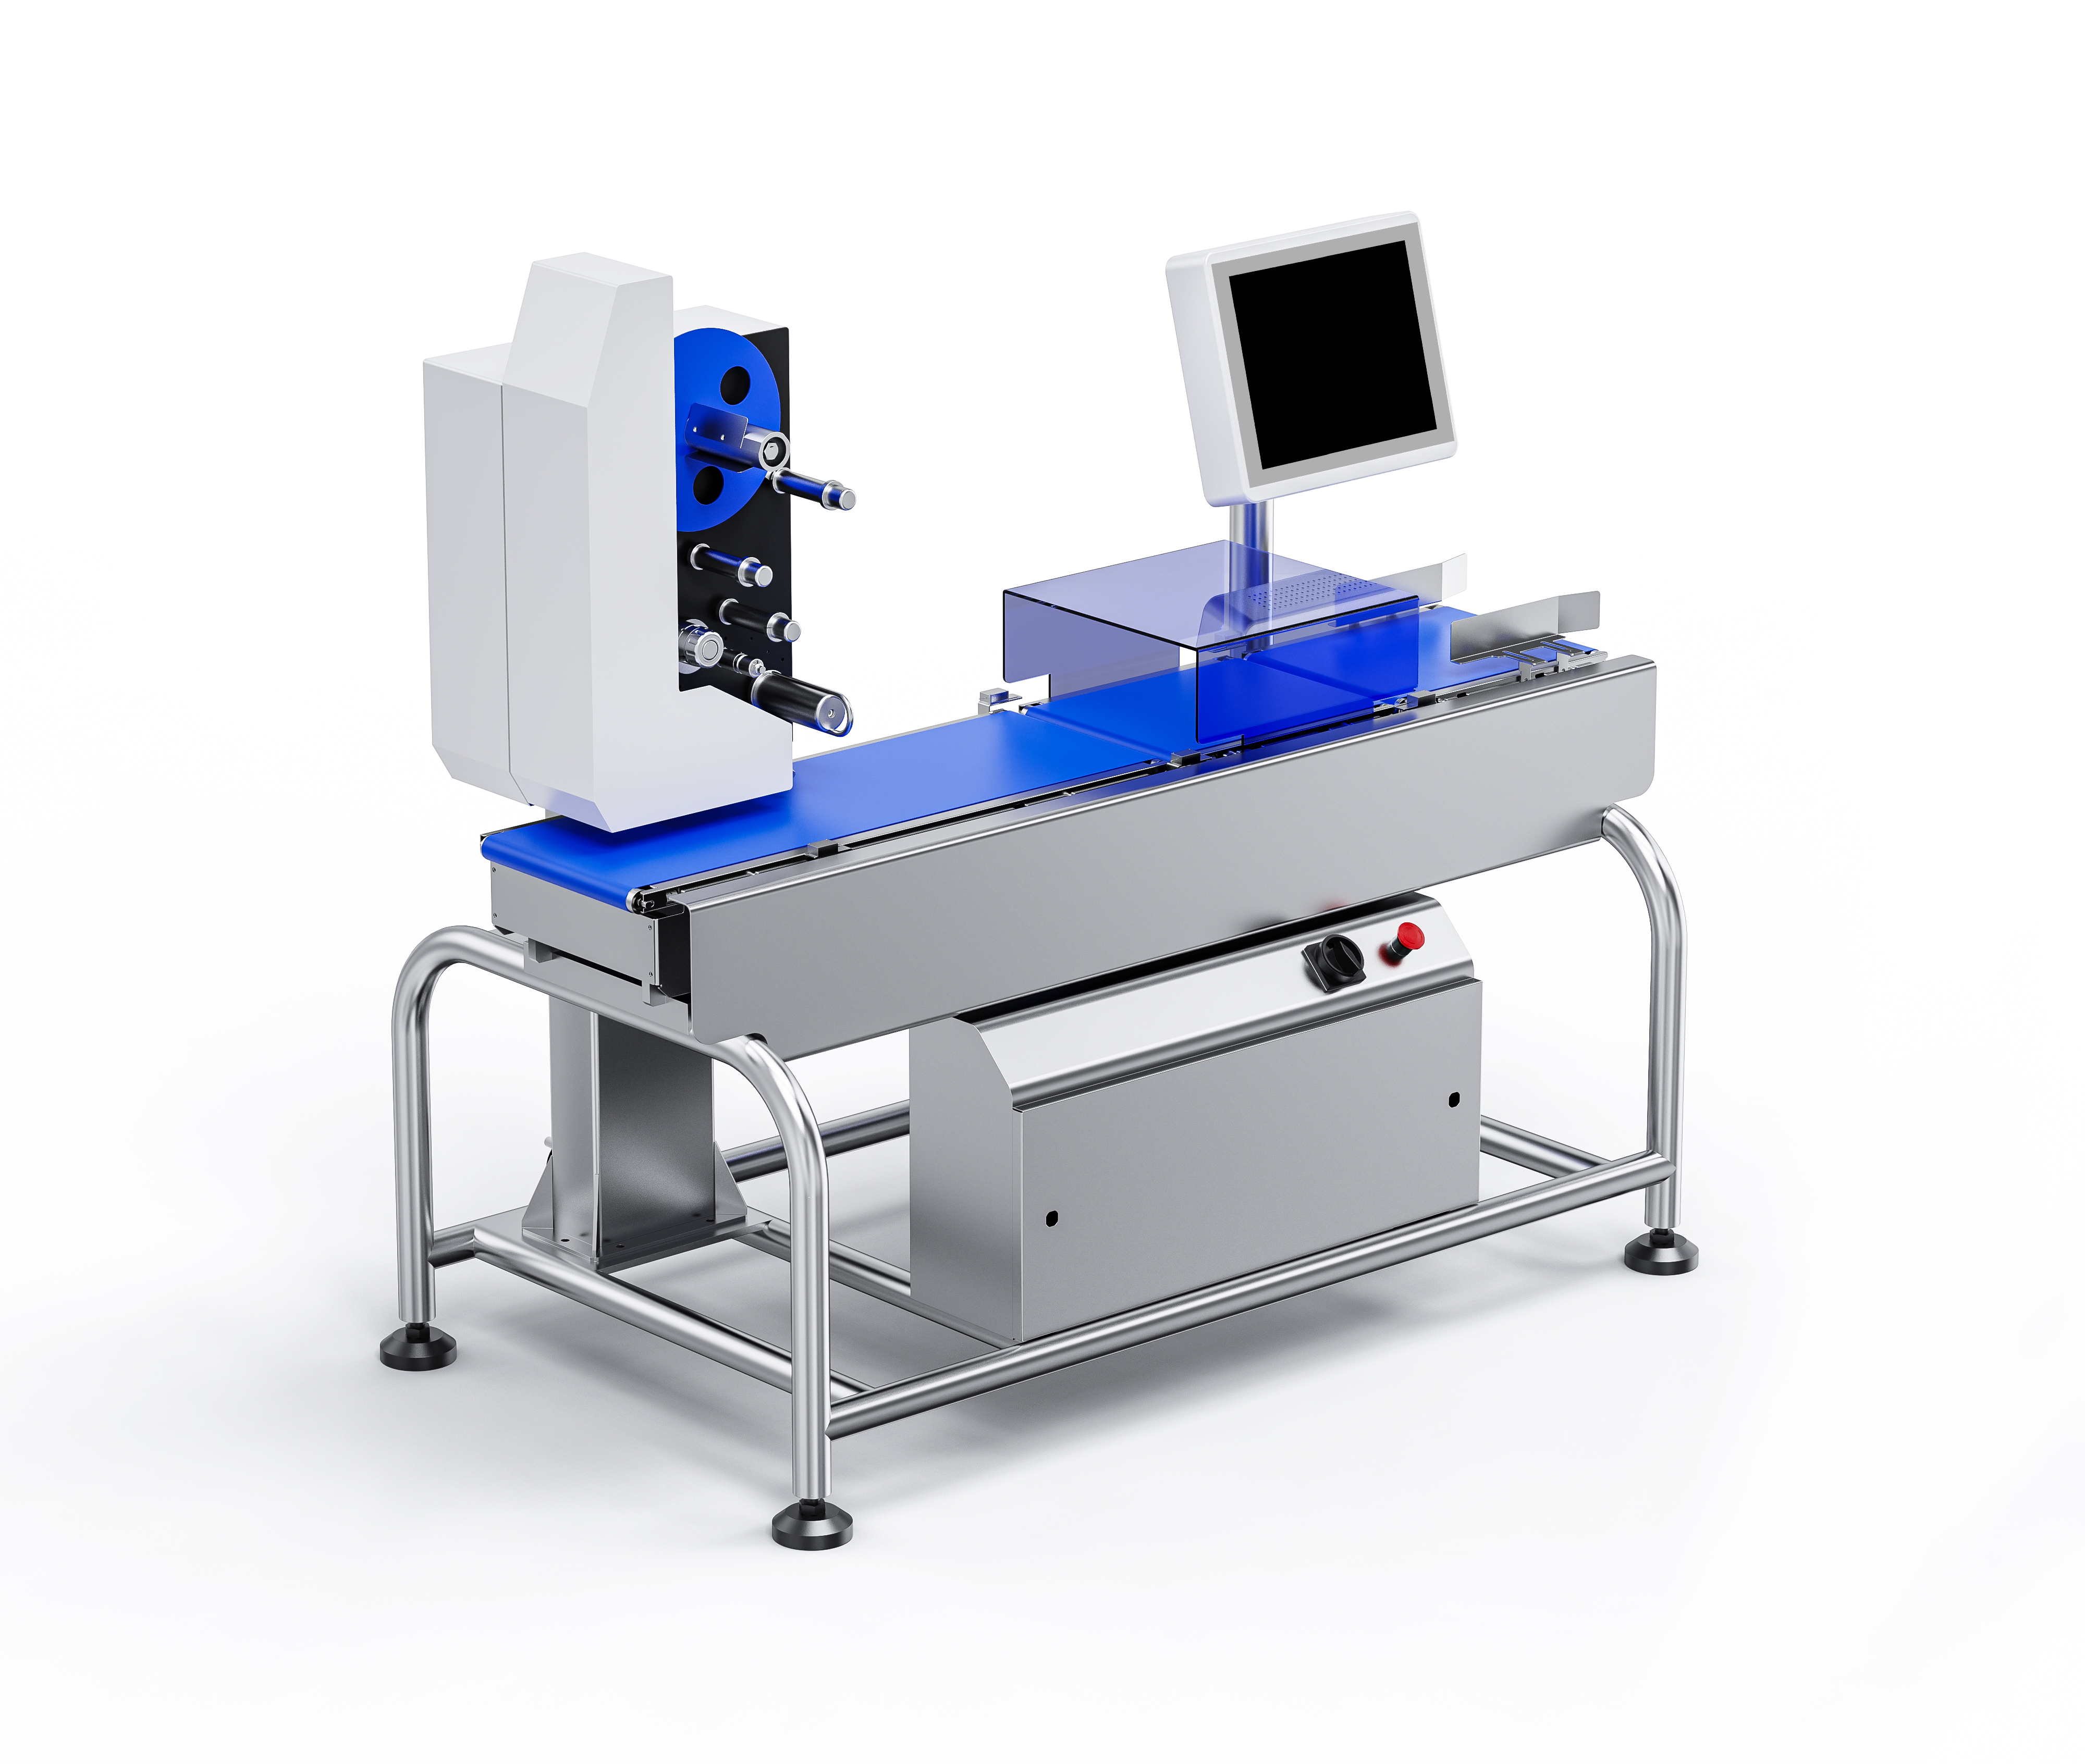
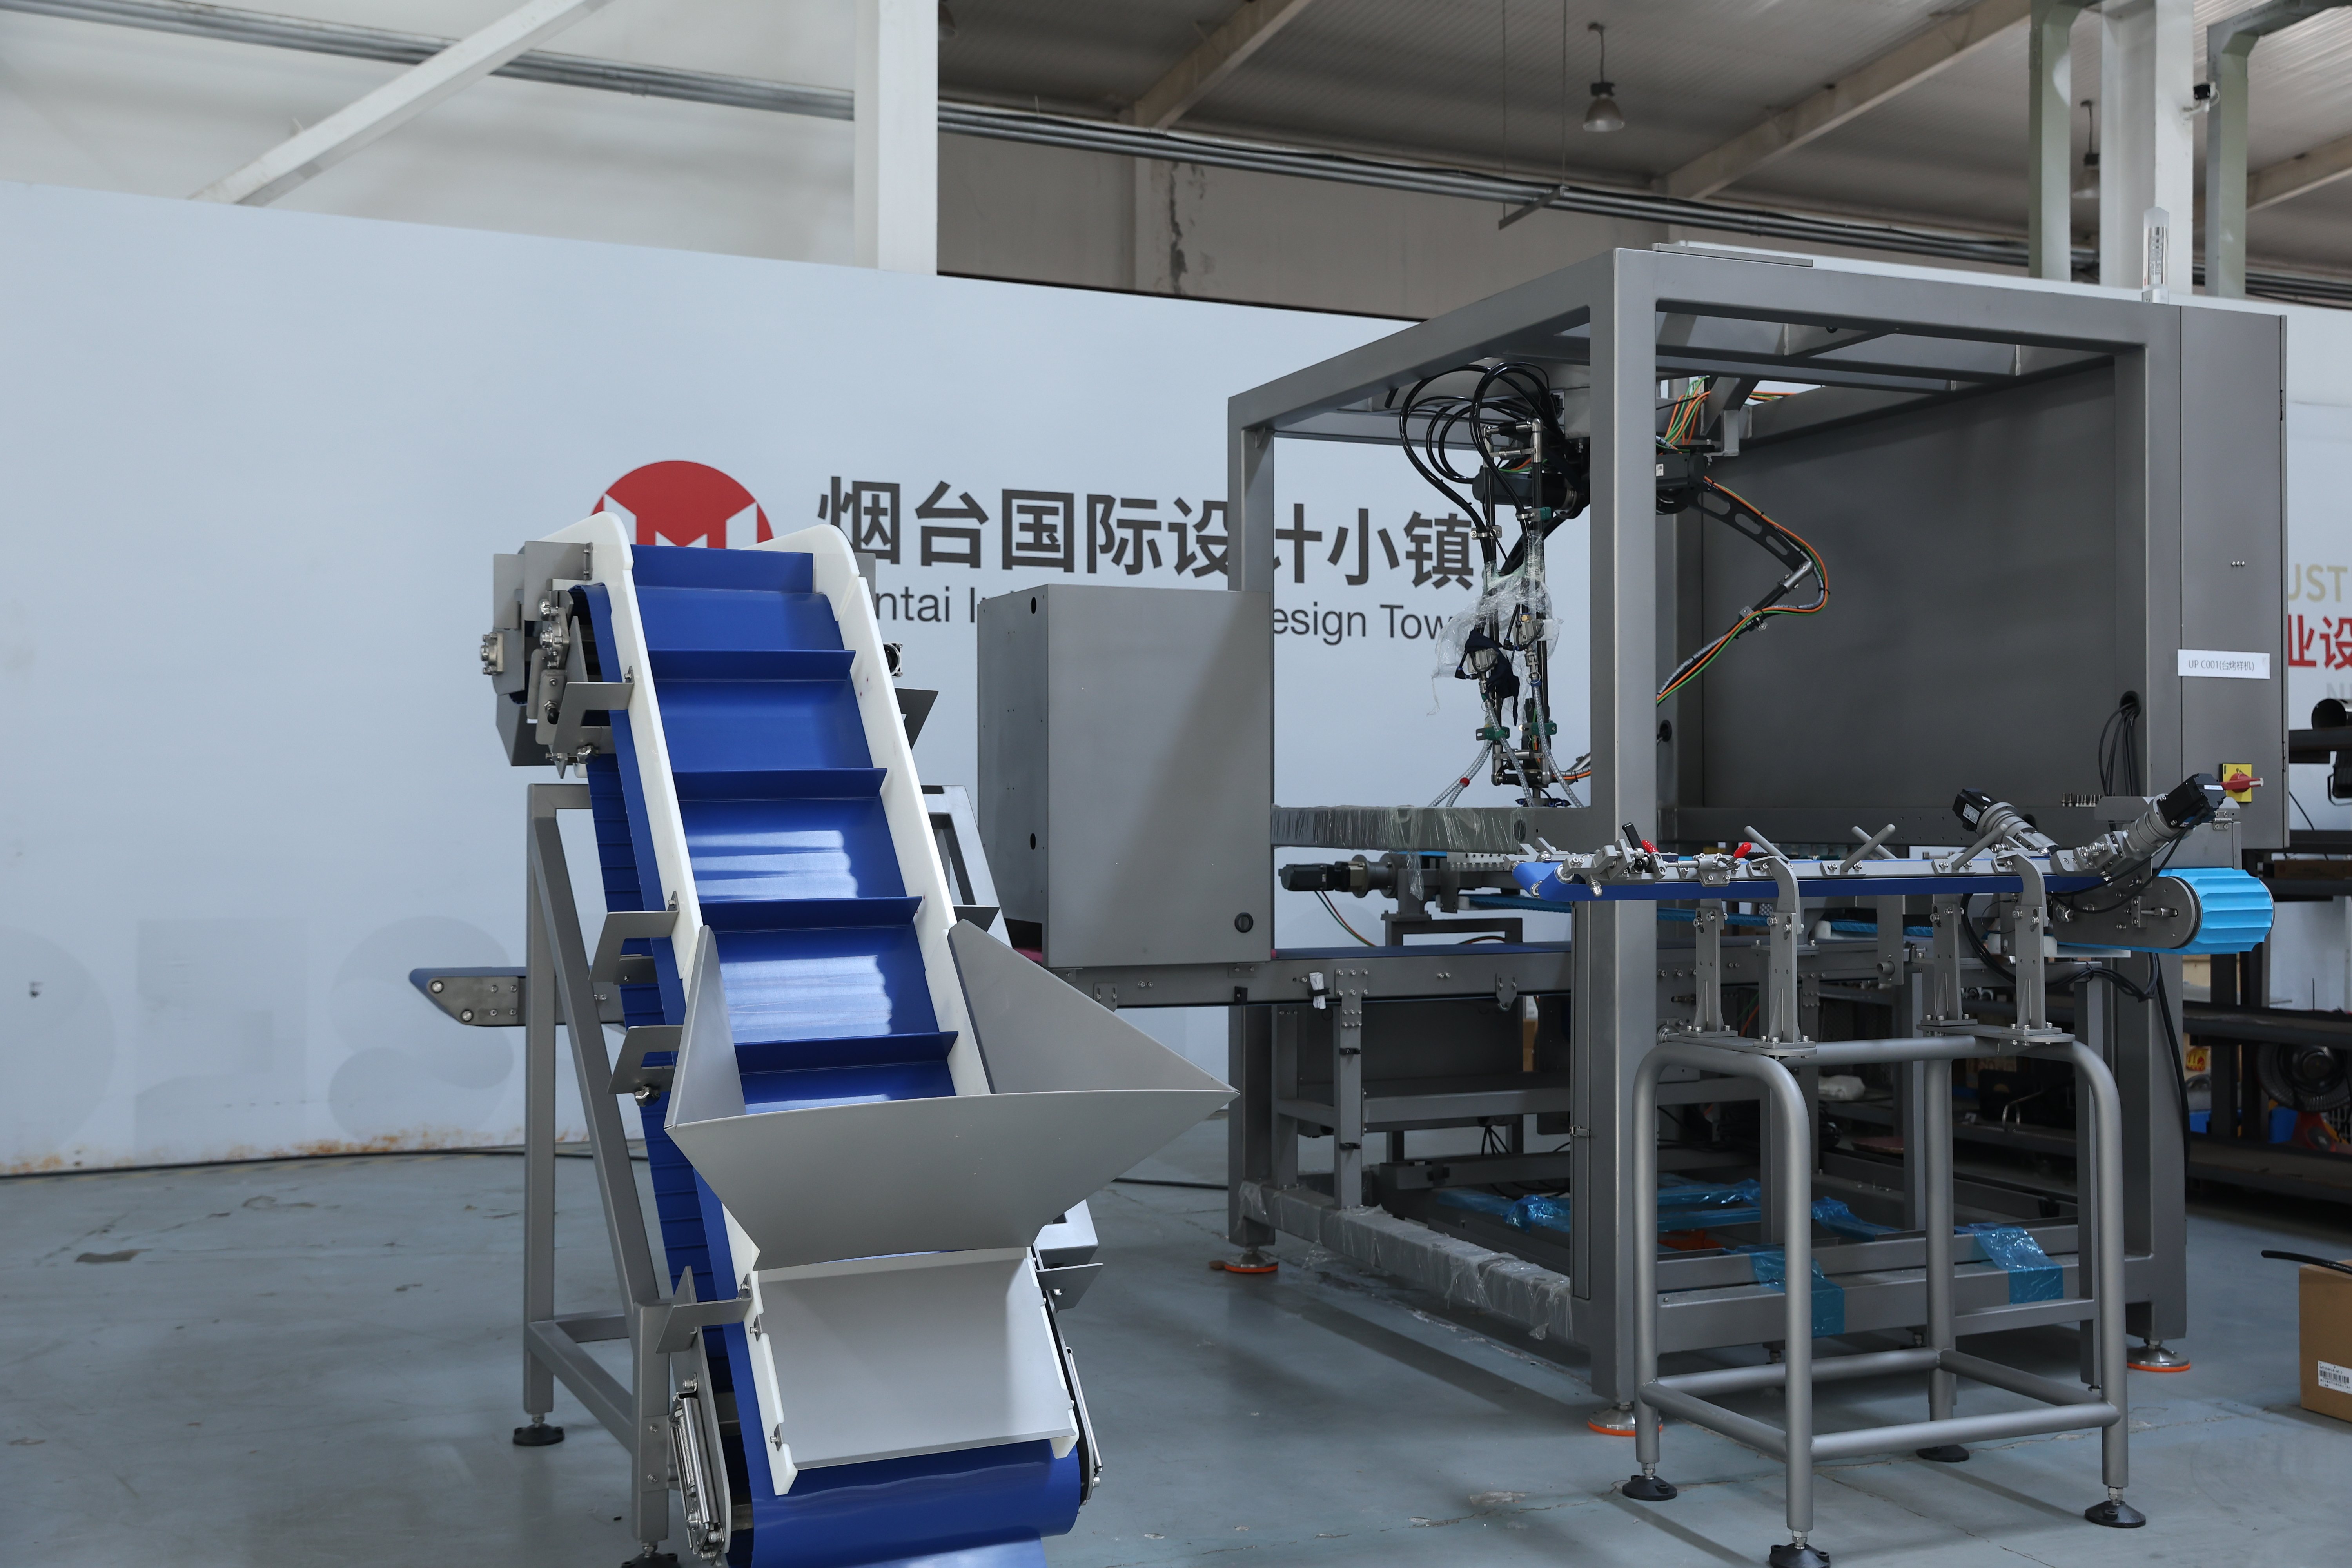
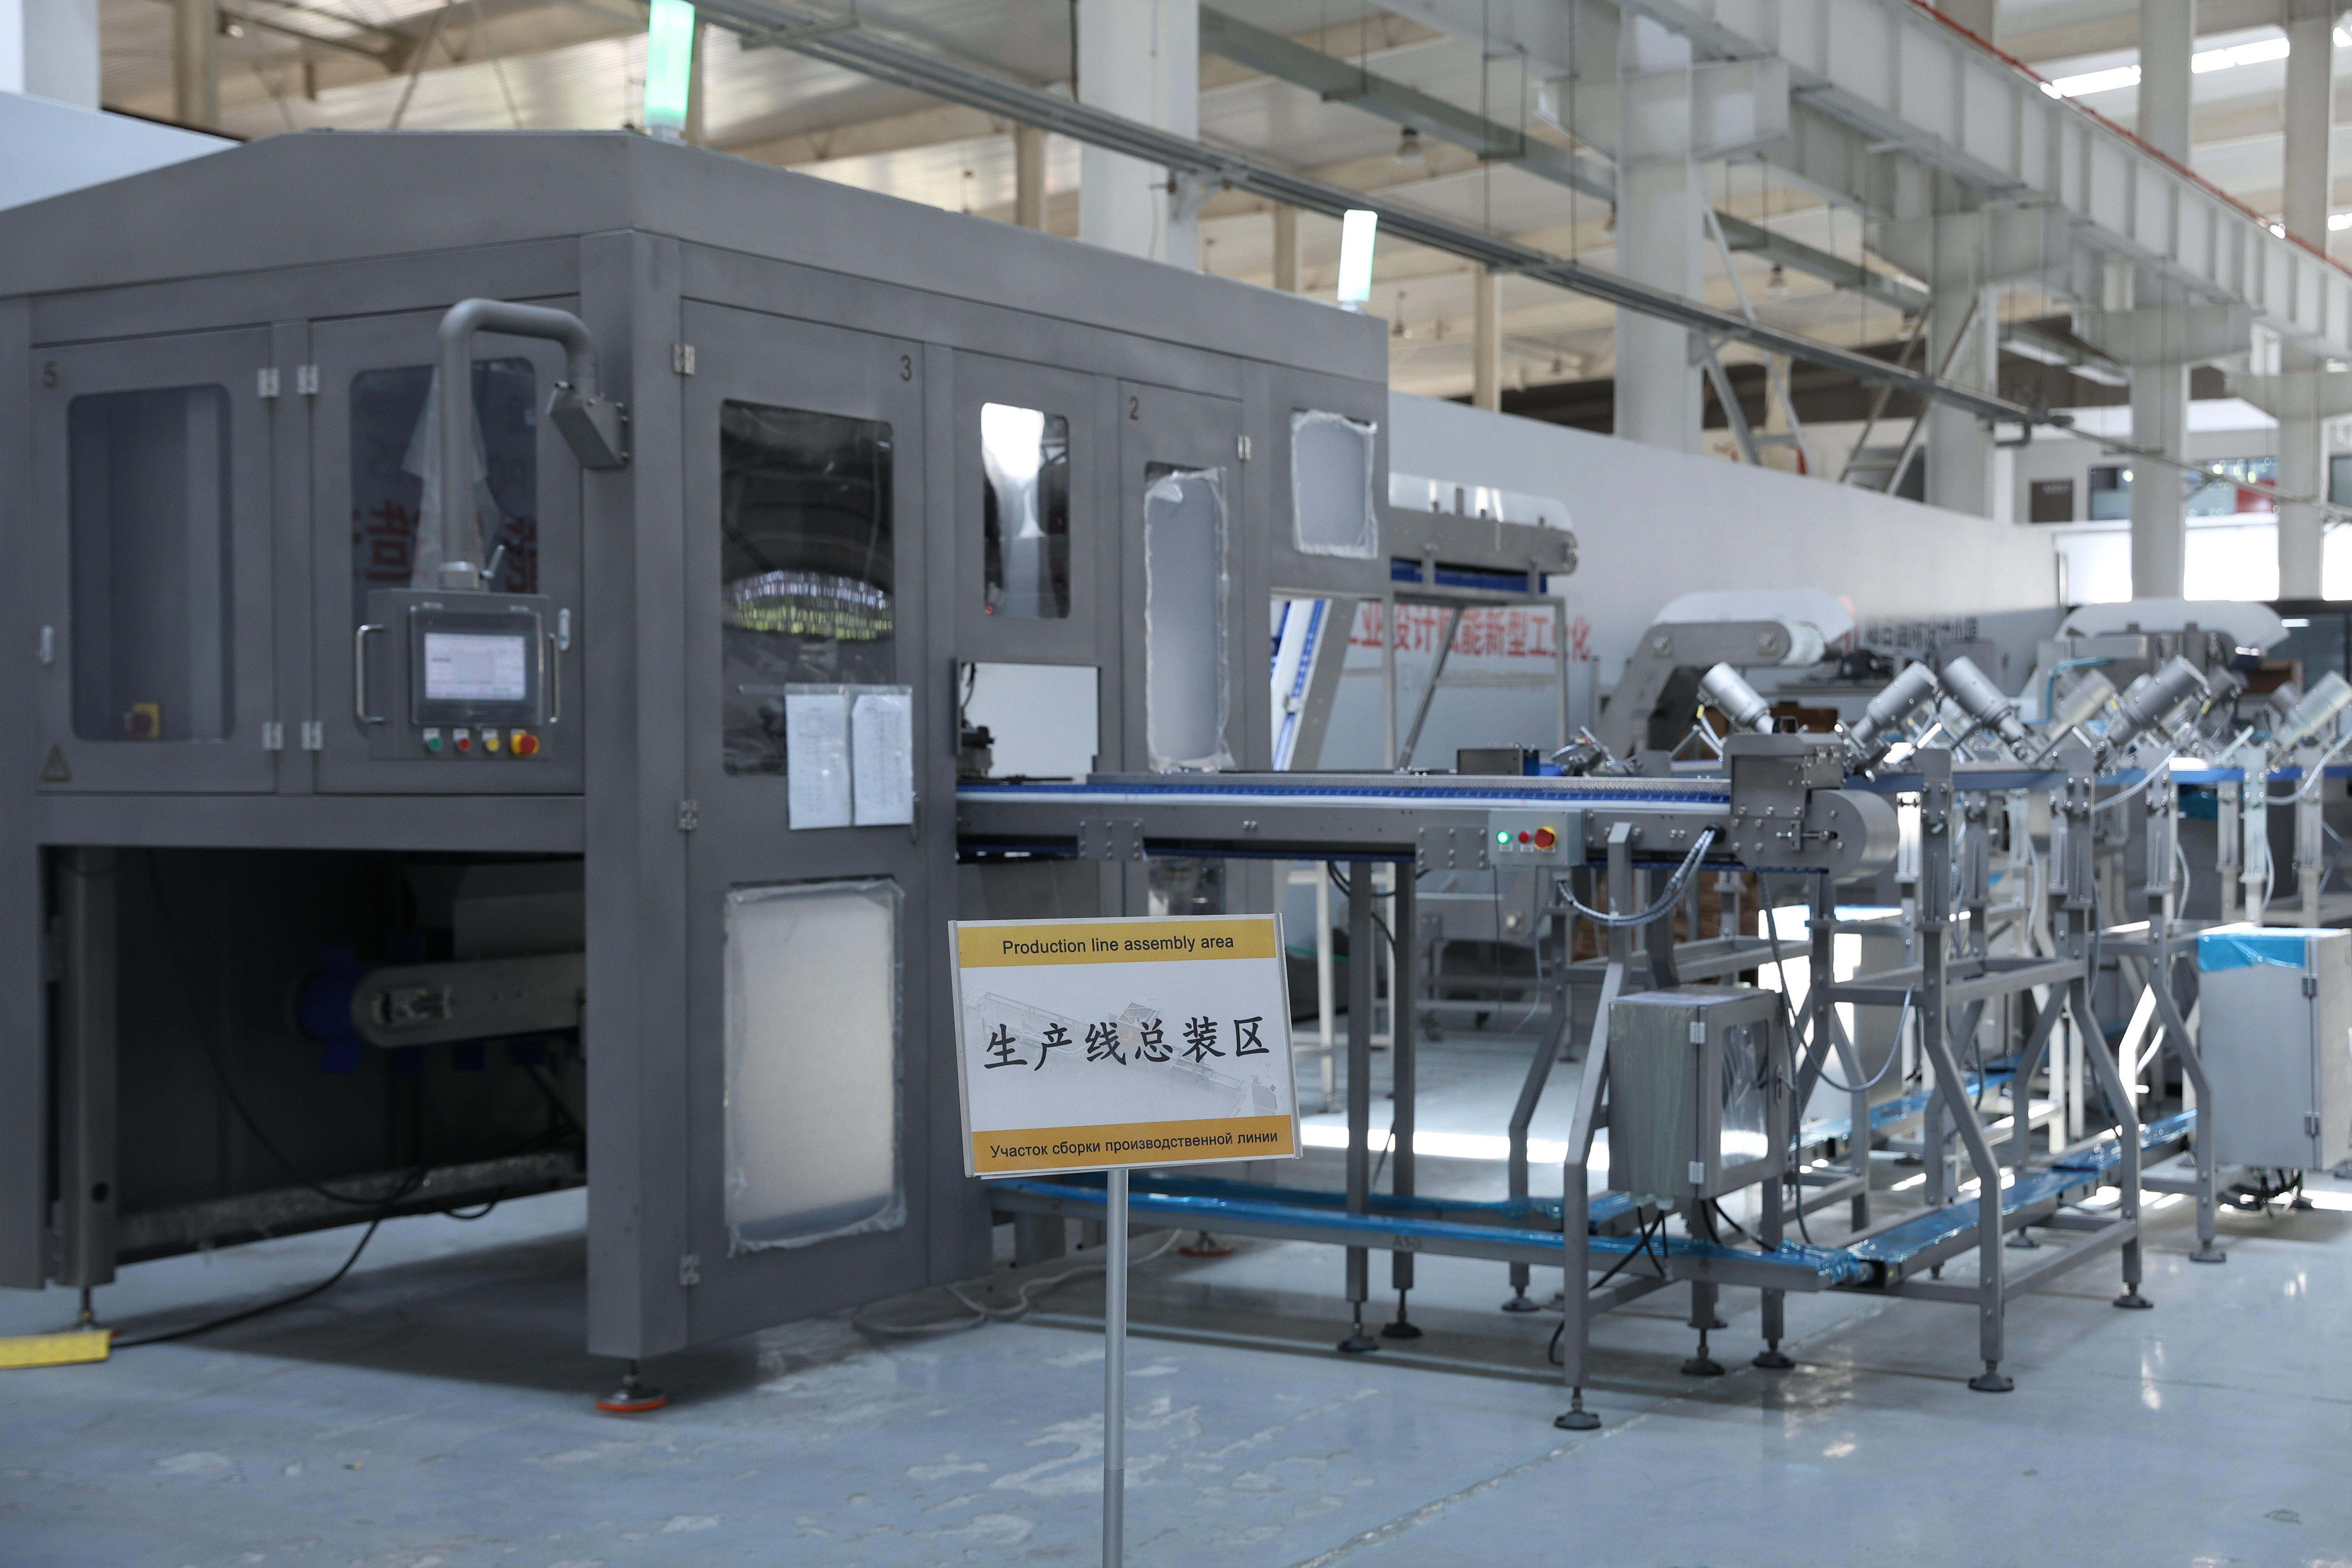
Automated material handling solutions represent a transformative approach to warehouse and logistics operations. These systems streamline the movement, storage, and retrieval of goods throughout your facility, eliminating manual labor inefficiencies and reducing operational costs significantly. Automated material handling solutions utilize advanced robotics, conveyor systems, and intelligent software to manage inventory with unprecedented precision and speed.
The core functions of automated material handling solutions include automated sorting, picking, packing, and transportation of items. These systems work seamlessly to reduce human error and accelerate order fulfillment processes. The technological features encompass real-time inventory tracking, artificial intelligence-driven optimization algorithms, and integrated warehouse management systems that communicate across all operational touchpoints.
Applications for automated material handling solutions span diverse industries including e-commerce, manufacturing, pharmaceuticals, and retail distribution centers. From high-volume order fulfillment to specialized handling of sensitive materials, automated material handling solutions adapt to various operational requirements. These solutions integrate conveyors, autonomous mobile robots, automated storage and retrieval systems, and vision-guided technology to create cohesive material flow networks.
The implementation of automated material handling solutions enables facilities to handle increasing order volumes without proportional increases in staffing requirements. Modern systems provide scalability, allowing businesses to expand capacity as demand grows. By choosing automated material handling solutions, companies invest in long-term operational excellence and competitive advantage in today's fast-paced logistics environment.

 EN


