robot box palletizer
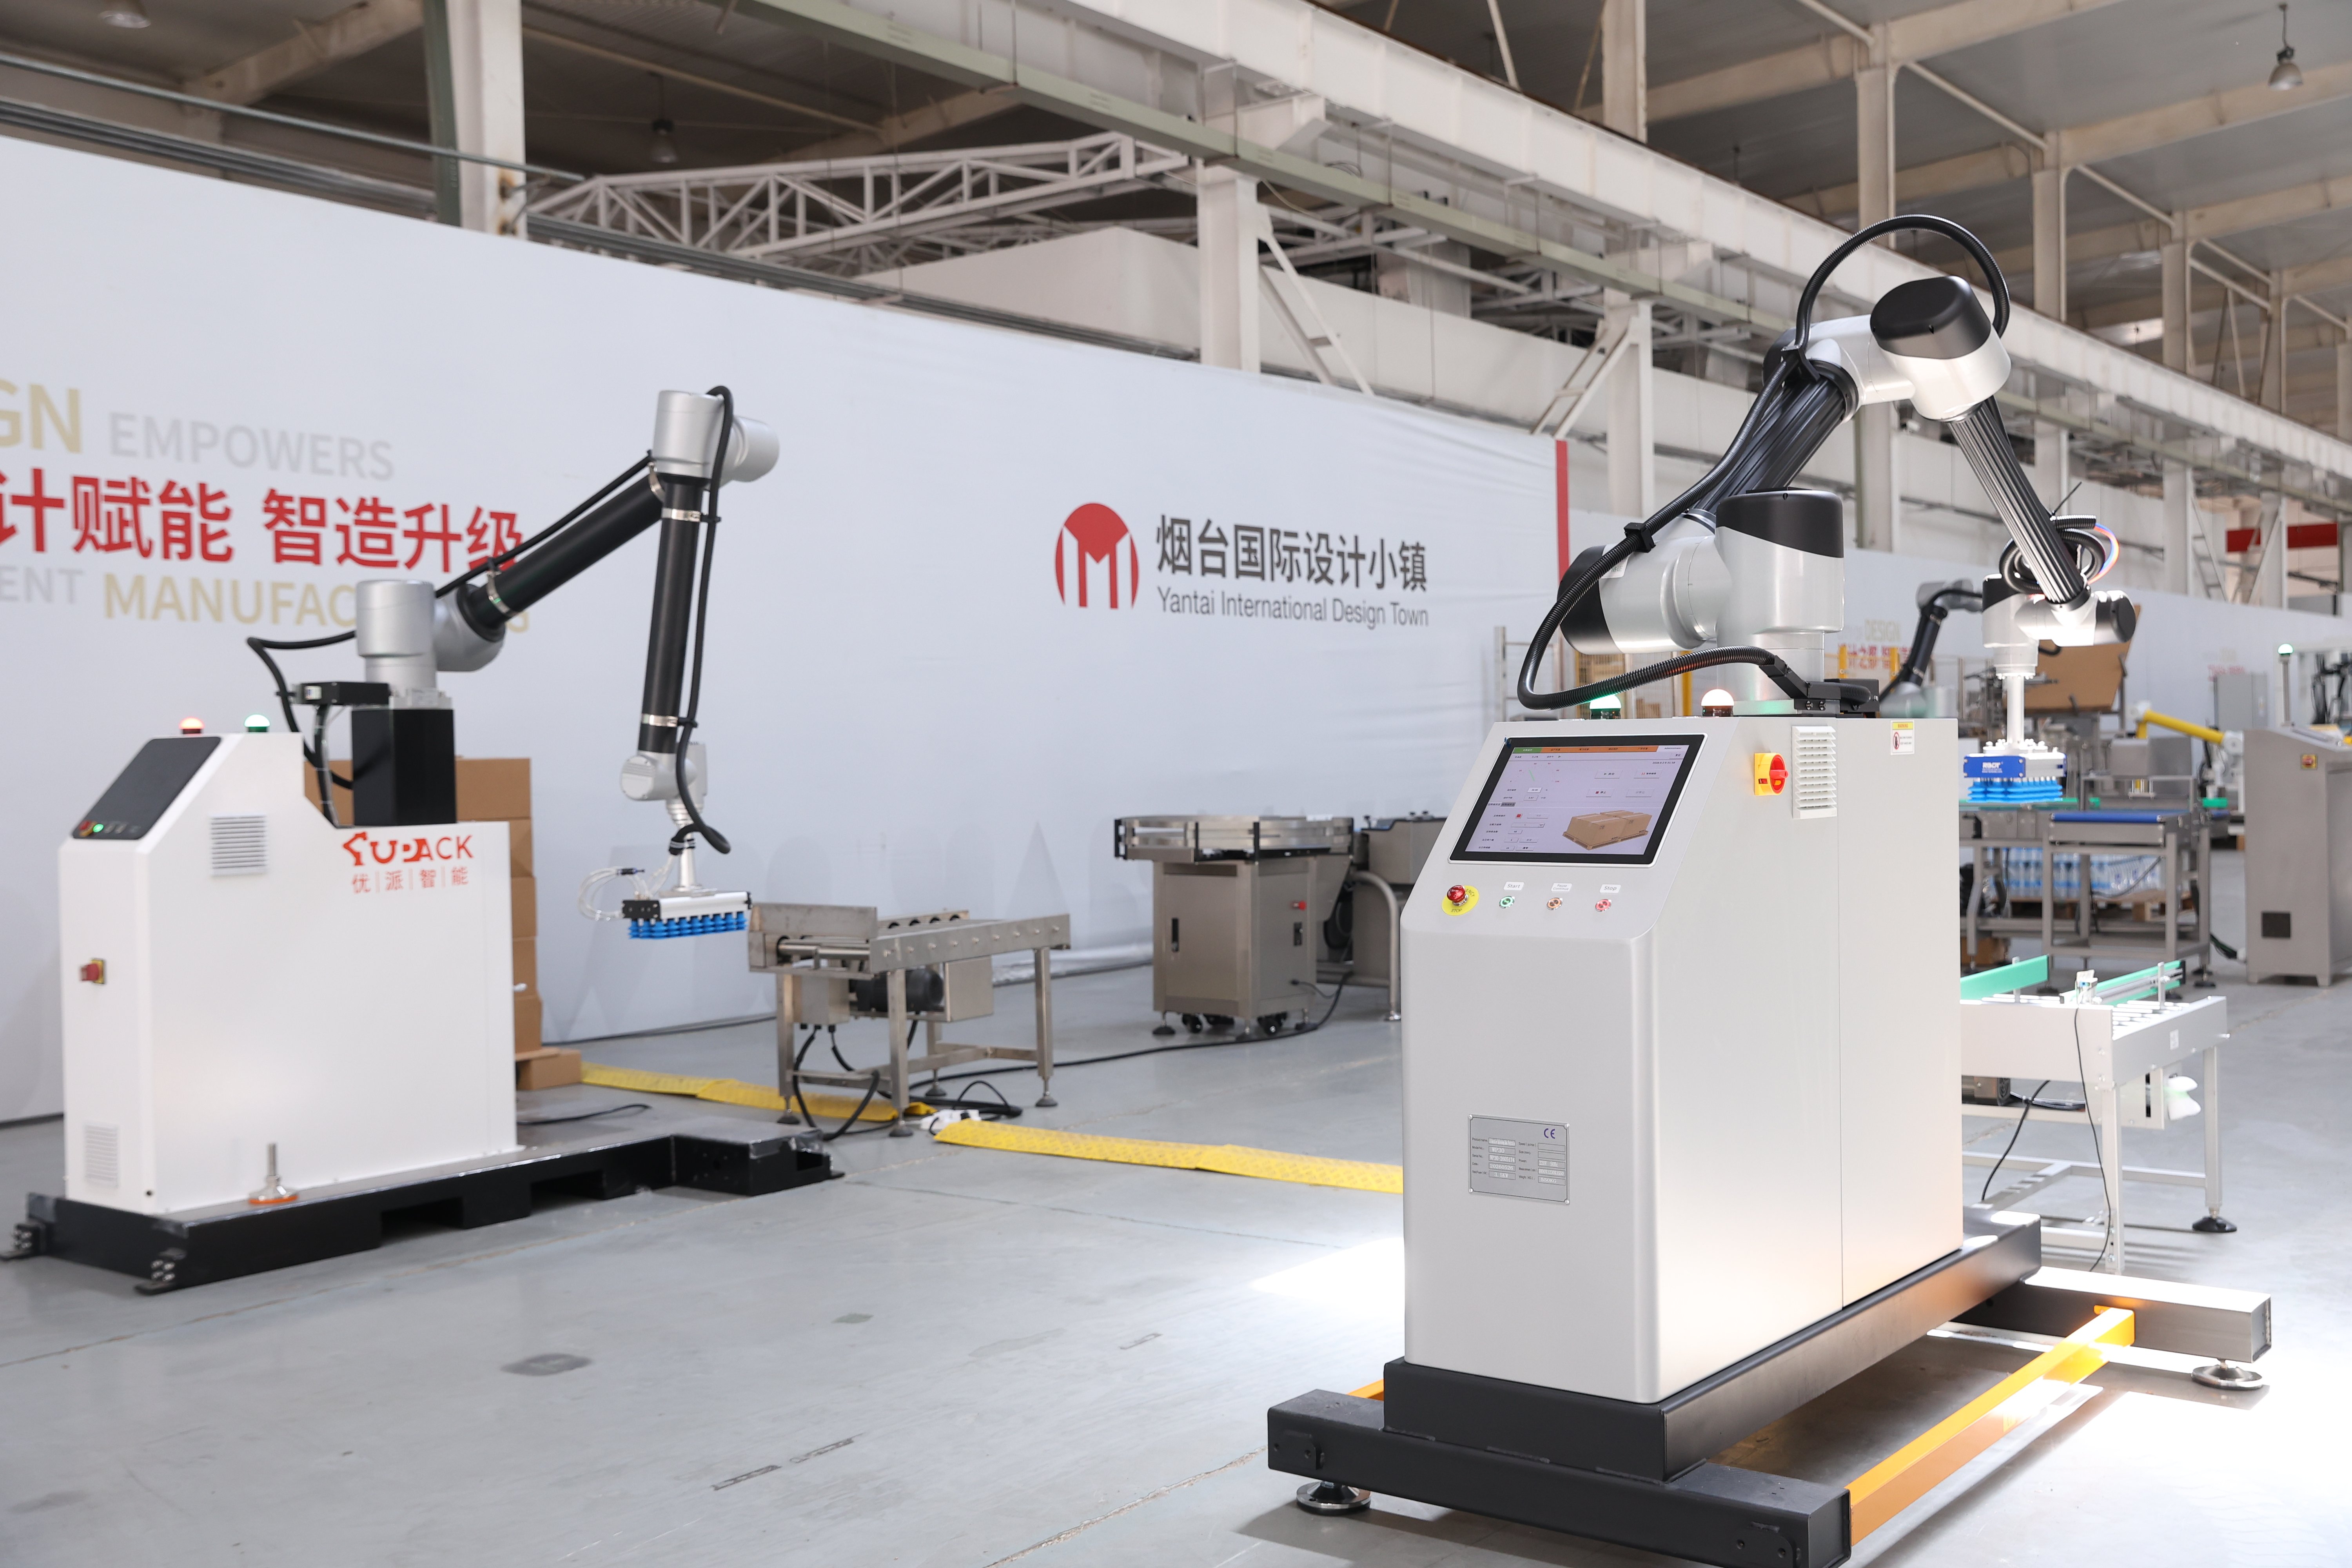
A robot box palletizer represents a revolutionary automated solution designed to streamline warehouse and manufacturing operations. This advanced equipment uses robotic technology to efficiently stack boxes onto pallets, dramatically improving productivity and reducing manual labor requirements. The robot box palletizer combines precision engineering with intelligent software to handle repetitive palletizing tasks with remarkable accuracy and speed.
The primary function of a robot box palletizer is to automatically arrange boxes in organized, stable stacks on pallets for storage, transportation, and distribution. This system can process hundreds of boxes per hour, maintaining consistent pallet configurations regardless of box size or weight variations. Modern robot box palletizer units feature adaptive gripper systems that gently handle delicate items while securely gripping heavier products.
Technologically, the robot box palletizer incorporates advanced vision systems that detect box dimensions and weight, allowing real-time adjustments to stacking patterns. These systems use artificial intelligence to optimize pallet utilization and minimize wasted space. The robot box palletizer integrates seamlessly with existing conveyor systems and warehouse management software, creating a cohesive automated environment.
Applications for a robot box palletizer span numerous industries including food and beverage, pharmaceuticals, electronics, and consumer goods manufacturing. Companies utilize robot box palletizer technology in distribution centers, production facilities, and logistics hubs. The flexibility of a robot box palletizer makes it suitable for high-volume operations requiring consistent output quality and operational reliability throughout demanding work shifts.

 EN


