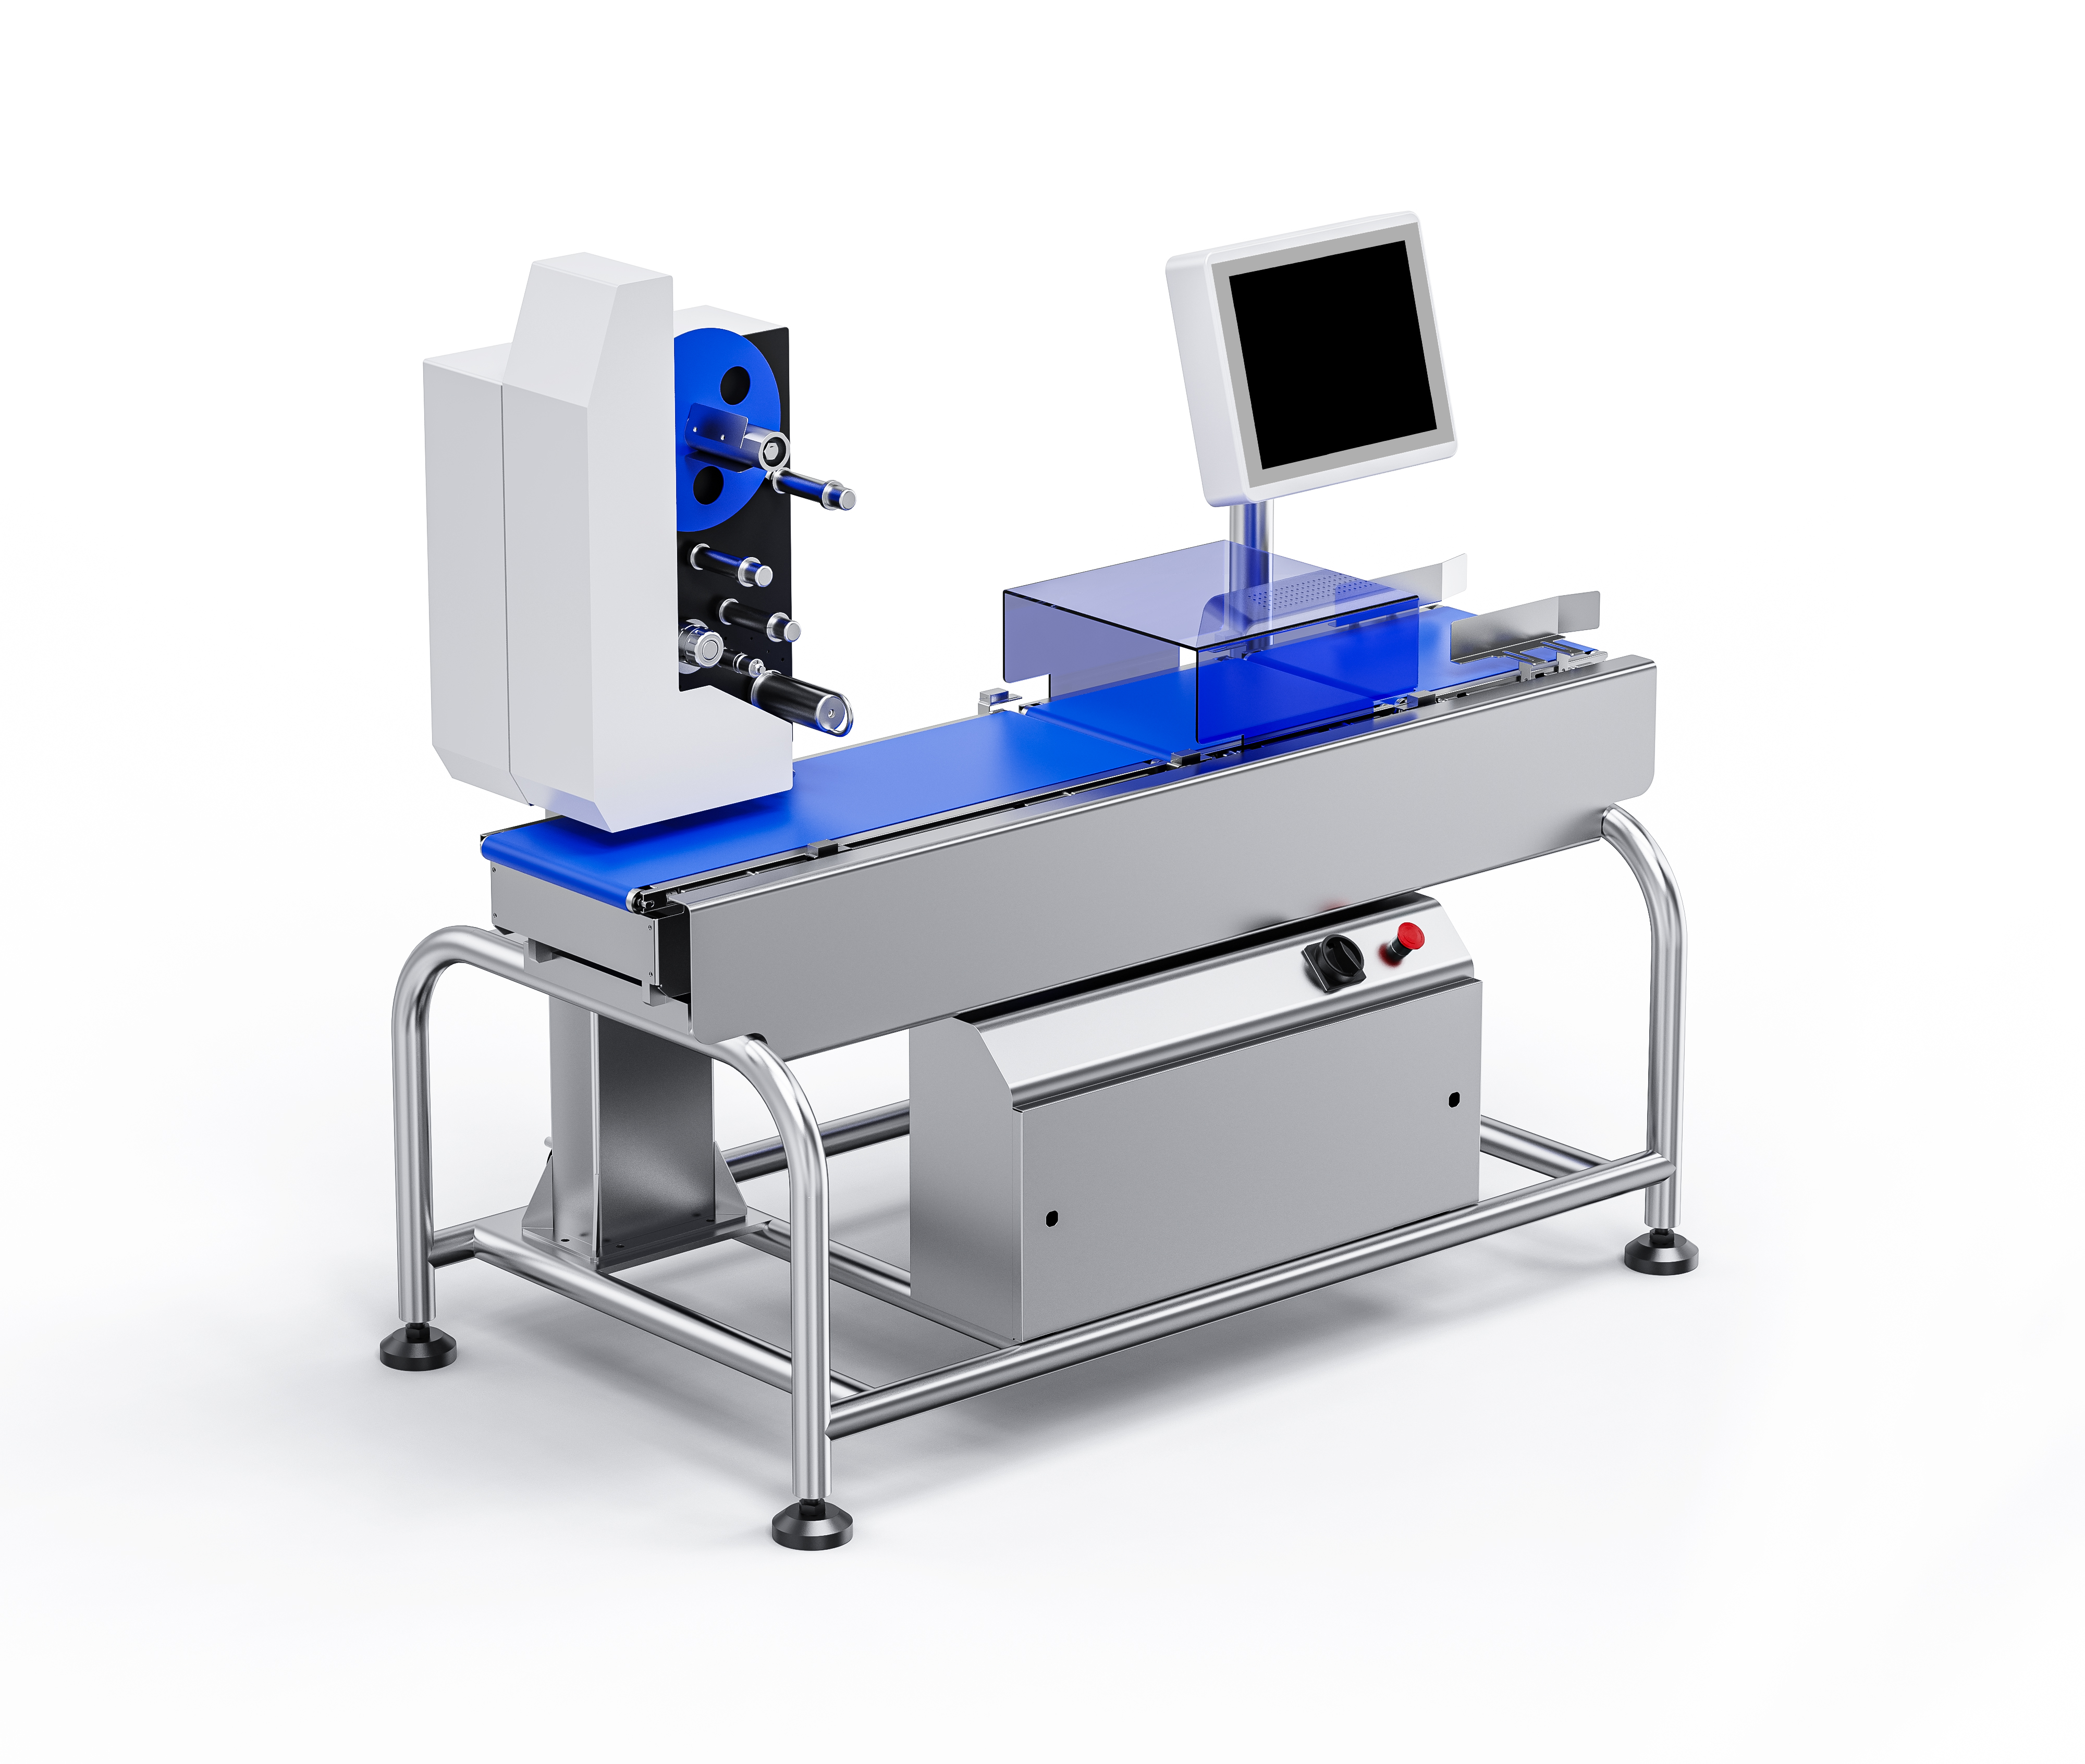
Box Palletizer Machine | Automated Pallet Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

box palletizer machine

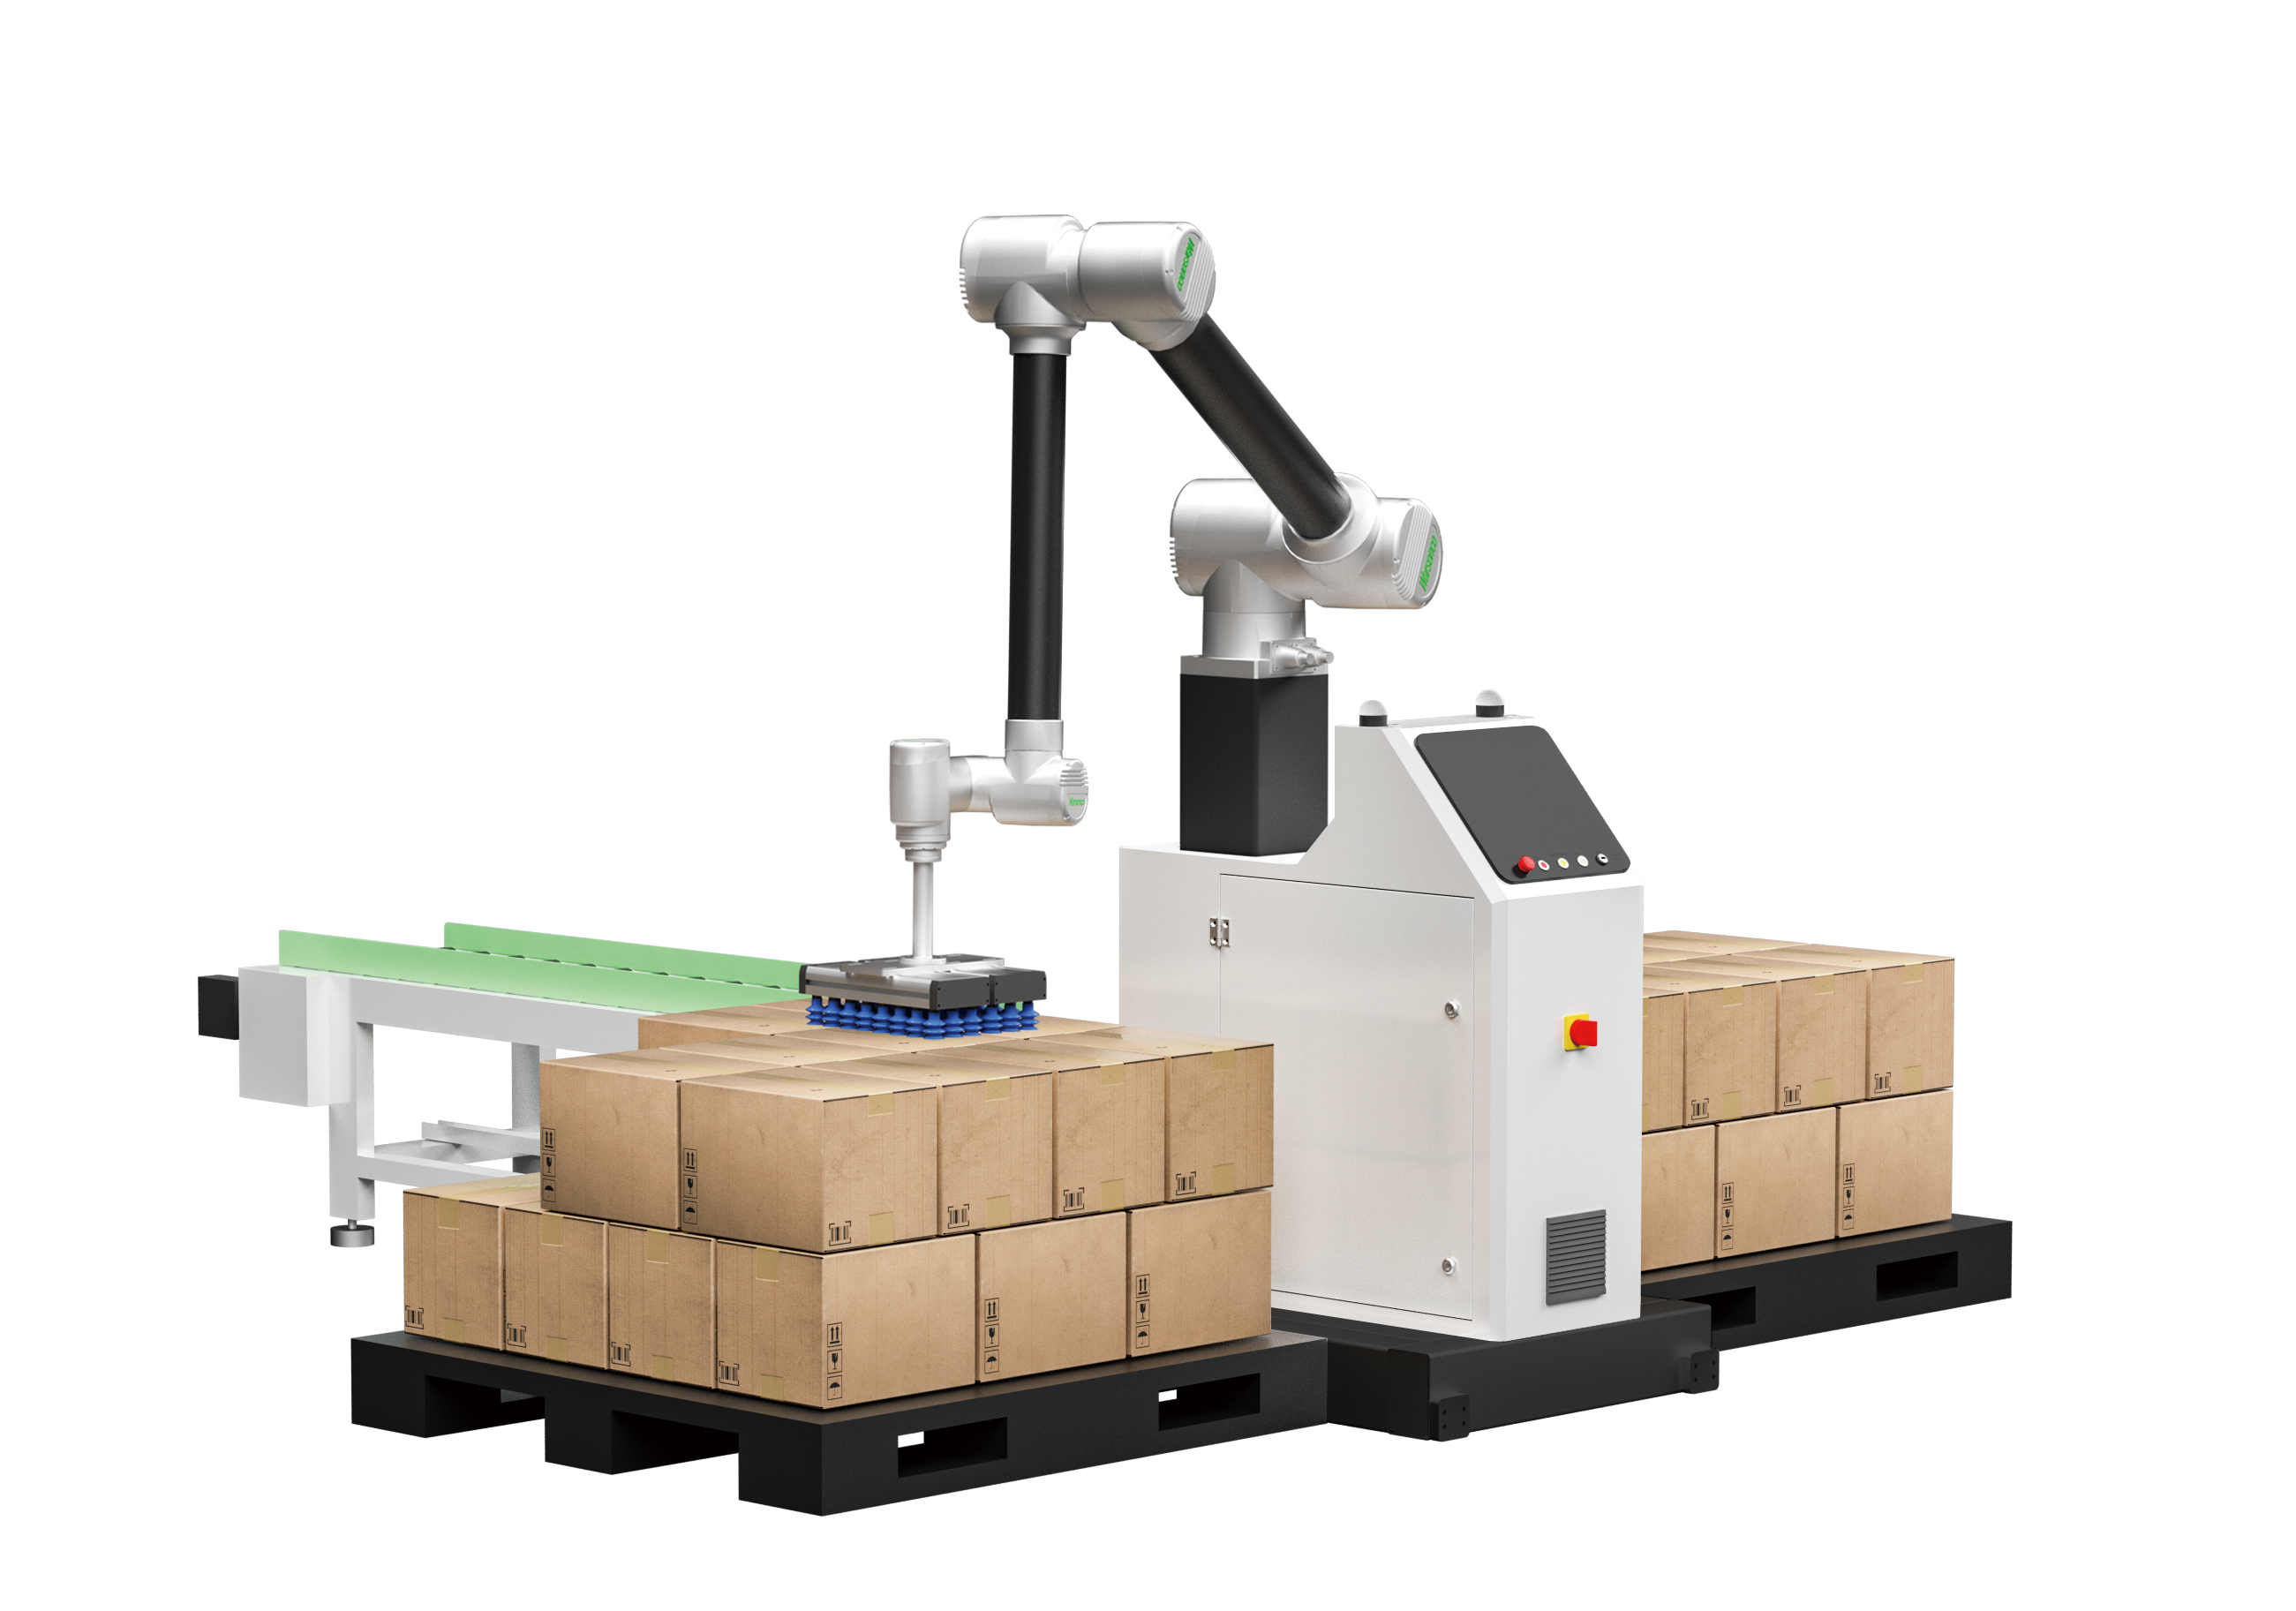
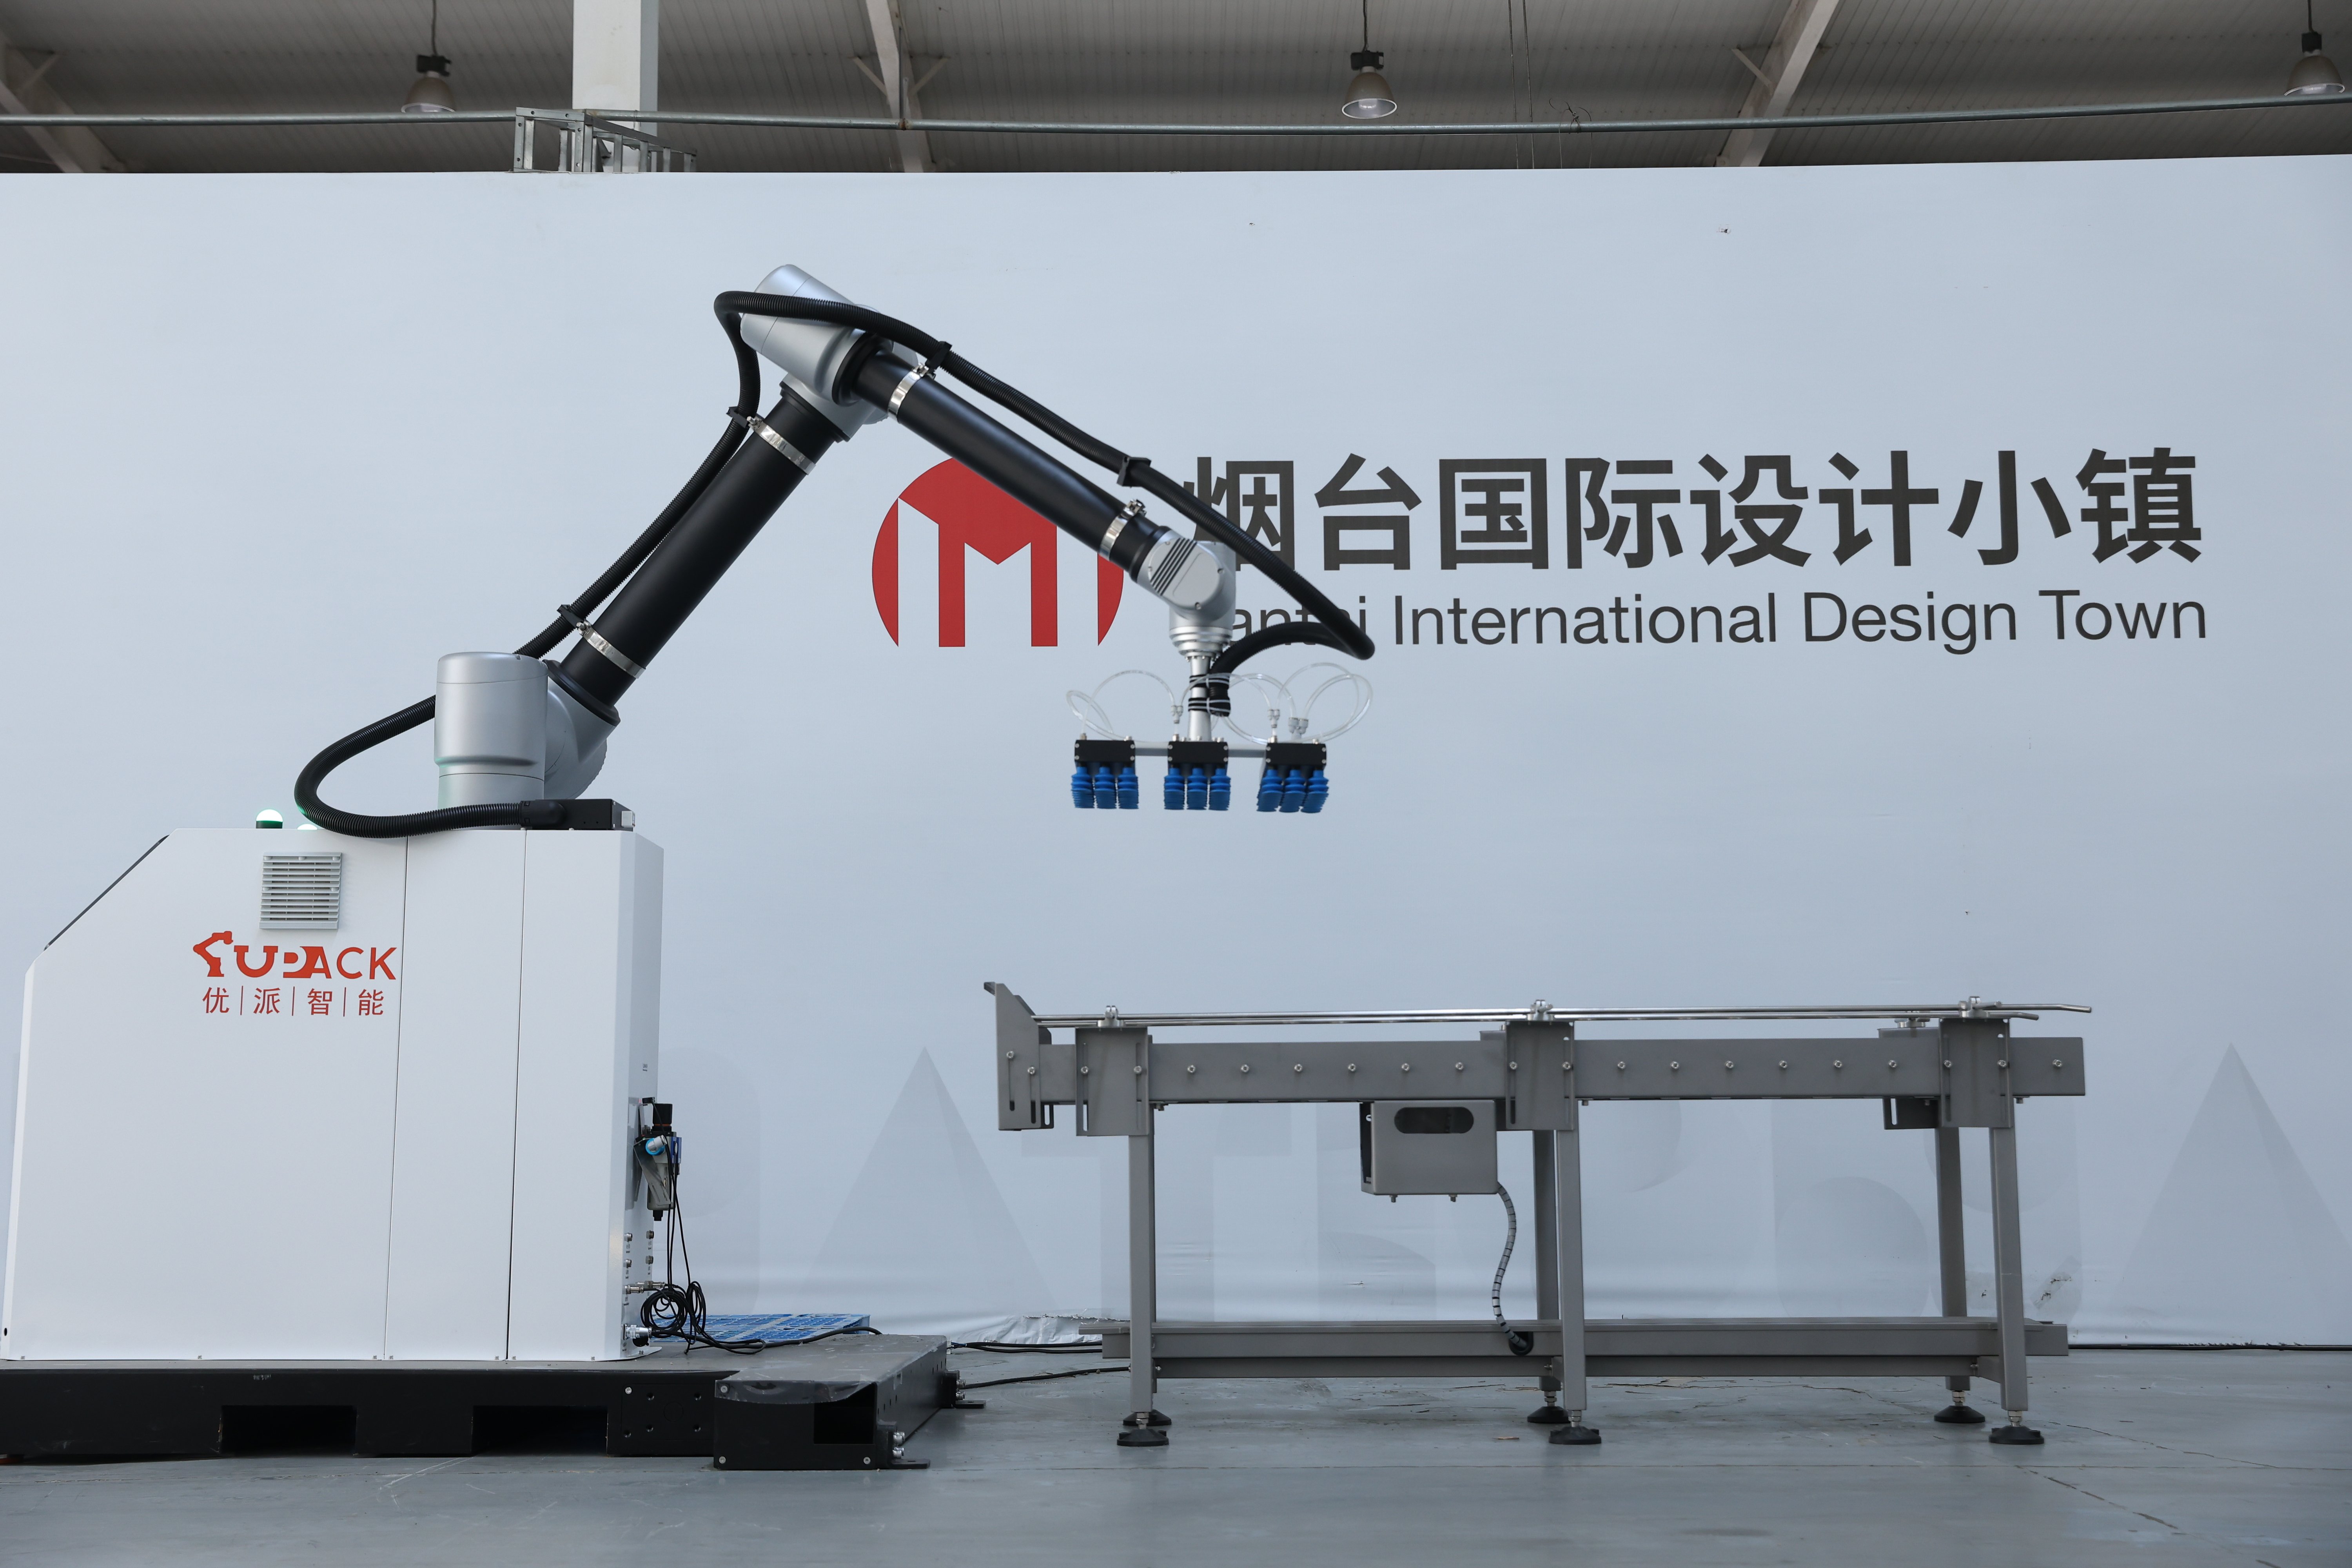
A box palletizer machine is an automated material handling system designed to efficiently stack boxes and cartons onto pallets with precision and speed. This innovative box palletizer machine streamlines warehouse operations by eliminating manual stacking processes, reducing labor costs, and increasing productivity. The box palletizer machine operates using advanced robotics and control systems that organize products into predetermined pallet patterns, ensuring consistent and stable loads. Modern box palletizer machines feature intelligent vision systems that detect box dimensions and weights, allowing automatic adjustment to various product sizes. These systems integrate seamlessly with existing conveyor lines and production facilities, making them ideal for high-volume distribution centers. The box palletizer machine accommodates different box configurations, from lightweight cartons to heavy industrial containers, providing versatility across multiple industries. Key technological features include programmable logic controllers, user-friendly touch screens, and real-time monitoring capabilities that track performance metrics and identify maintenance needs. The box palletizer machine delivers significant efficiency gains by processing hundreds of boxes per hour while maintaining accuracy. Applications span food and beverage, pharmaceuticals, cosmetics, electronics, and automotive sectors. Companies benefit from reduced product damage, improved worker safety, and enhanced operational efficiency when implementing a box palletizer machine solution. The investment in this technology translates to faster fulfillment times and improved competitiveness in today's demanding market landscape.
New Product Releases

The box palletizer machine offers numerous practical benefits that directly enhance operational performance and profitability. First, it dramatically reduces labor requirements by automating repetitive stacking tasks, allowing your workforce to focus on higher-value activities. This operational efficiency means faster pallet formation and reduced processing times, enabling businesses to handle increased order volumes without proportional cost increases. The box palletizer machine minimizes product damage through controlled, consistent stacking patterns that prevent box crushing and shifting during storage and transport. Worker safety improves significantly as employees no longer perform physically demanding stacking work, reducing injury risks and related compensation claims. Financial benefits include lower long-term labor costs, reduced product loss from mishandling, and improved shipping accuracy that enhances customer satisfaction. The box palletizer machine adapts quickly to changing product specifications and order requirements through simple software adjustments, providing flexibility that manual operations cannot match. Installation of a box palletizer machine typically integrates smoothly into existing warehouse layouts, minimizing disruption to current operations. Real-time tracking and reporting features provide valuable data for decision-making and performance optimization. Companies experience faster inventory turnover and improved supply chain responsiveness. The box palletizer machine creates competitive advantages by enabling faster order fulfillment and more reliable delivery schedules. Additionally, the technology reduces space requirements through efficient pallet utilization, maximizing warehouse capacity and reducing overhead costs. Return on investment occurs relatively quickly in high-volume operations, making this equipment a sound business decision for growth-oriented companies.

Tips And Tricks

Common Customer Q&A

20

Jan

Common Customer Q&A

View More
Global Collaboration, Shared Growth

20

Jan

Global Collaboration, Shared Growth

View More
Comprehensive After-Sales Service System for Peace

20

Jan

Comprehensive After-Sales Service System for Peace

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

box palletizer machine

Advanced Automation for Maximum Efficiency

Advanced Automation for Maximum Efficiency

The box palletizer machine incorporates state-of-the-art robotic technology that operates continuously without fatigue or performance degradation. This automation capability enables processing speeds that manual methods simply cannot achieve, handling hundreds of boxes hourly with precision and reliability. The box palletizer machine reduces cycle times significantly, meaning completed pallets leave your facility faster, accelerating cash flow and customer delivery timelines. Programmable settings allow the box palletizer machine to optimize stacking patterns based on product weight distribution, ensuring maximum load stability and safety during transport. The consistent performance of this equipment eliminates human variability that often leads to quality inconsistencies. Your facility gains predictable output metrics, enabling accurate production forecasting and resource planning. The box palletizer machine operates across multiple shifts without quality degradation, providing unmatched reliability that traditional labor-based systems cannot replicate. This technological advancement positions your warehouse operations at peak efficiency levels.
Flexible Integration with Existing Systems

Flexible Integration with Existing Systems

A box palletizer machine seamlessly connects with your current conveyor systems and warehouse infrastructure, requiring minimal modifications to established workflows. The flexible design accommodates diverse box dimensions, weights, and materials, from delicate consumer products to industrial components. Your box palletizer machine can be reprogrammed quickly to handle different product configurations, adapting to seasonal demands or product line changes without requiring equipment replacement. This versatility makes the investment more cost-effective across multiple applications and industries. Integration capabilities include connections to inventory management systems, enabling synchronized operations between receiving, processing, and shipping departments. The box palletizer machine interfaces with your existing WMS and ERP systems, creating unified operational visibility. Real-time communication between the box palletizer machine and management systems provides instant alerts about performance issues or maintenance requirements. This interconnectedness optimizes overall warehouse performance and reduces operational silos that typically hinder efficiency gains.
Superior Product Protection and Quality Control

Superior Product Protection and Quality Control

The box palletizer machine ensures consistent, controlled stacking that significantly reduces product damage during warehouse handling and transportation. Precise load formation prevents boxes from shifting, crushing, or toppling, protecting your valuable inventory from costly loss. The box palletizer machine utilizes advanced sensors to detect box conditions and adjust handling force accordingly, accommodating fragile products that require gentler treatment. Quality control benefits extend beyond mere damage prevention; the box palletizer machine maintains pallet integrity by ensuring proper weight distribution and load balancing. Damaged goods represent substantial financial losses and customer dissatisfaction, both of which are substantially reduced by implementing this equipment. The box palletizer machine creates audit trails documenting each pallet's formation, providing accountability and traceability for compliance requirements. This quality assurance capability is invaluable for pharmaceutical, food service, and other regulated industries. Customers receive products in pristine condition, enhancing your reputation and encouraging repeat business.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000