custom conveyor systems
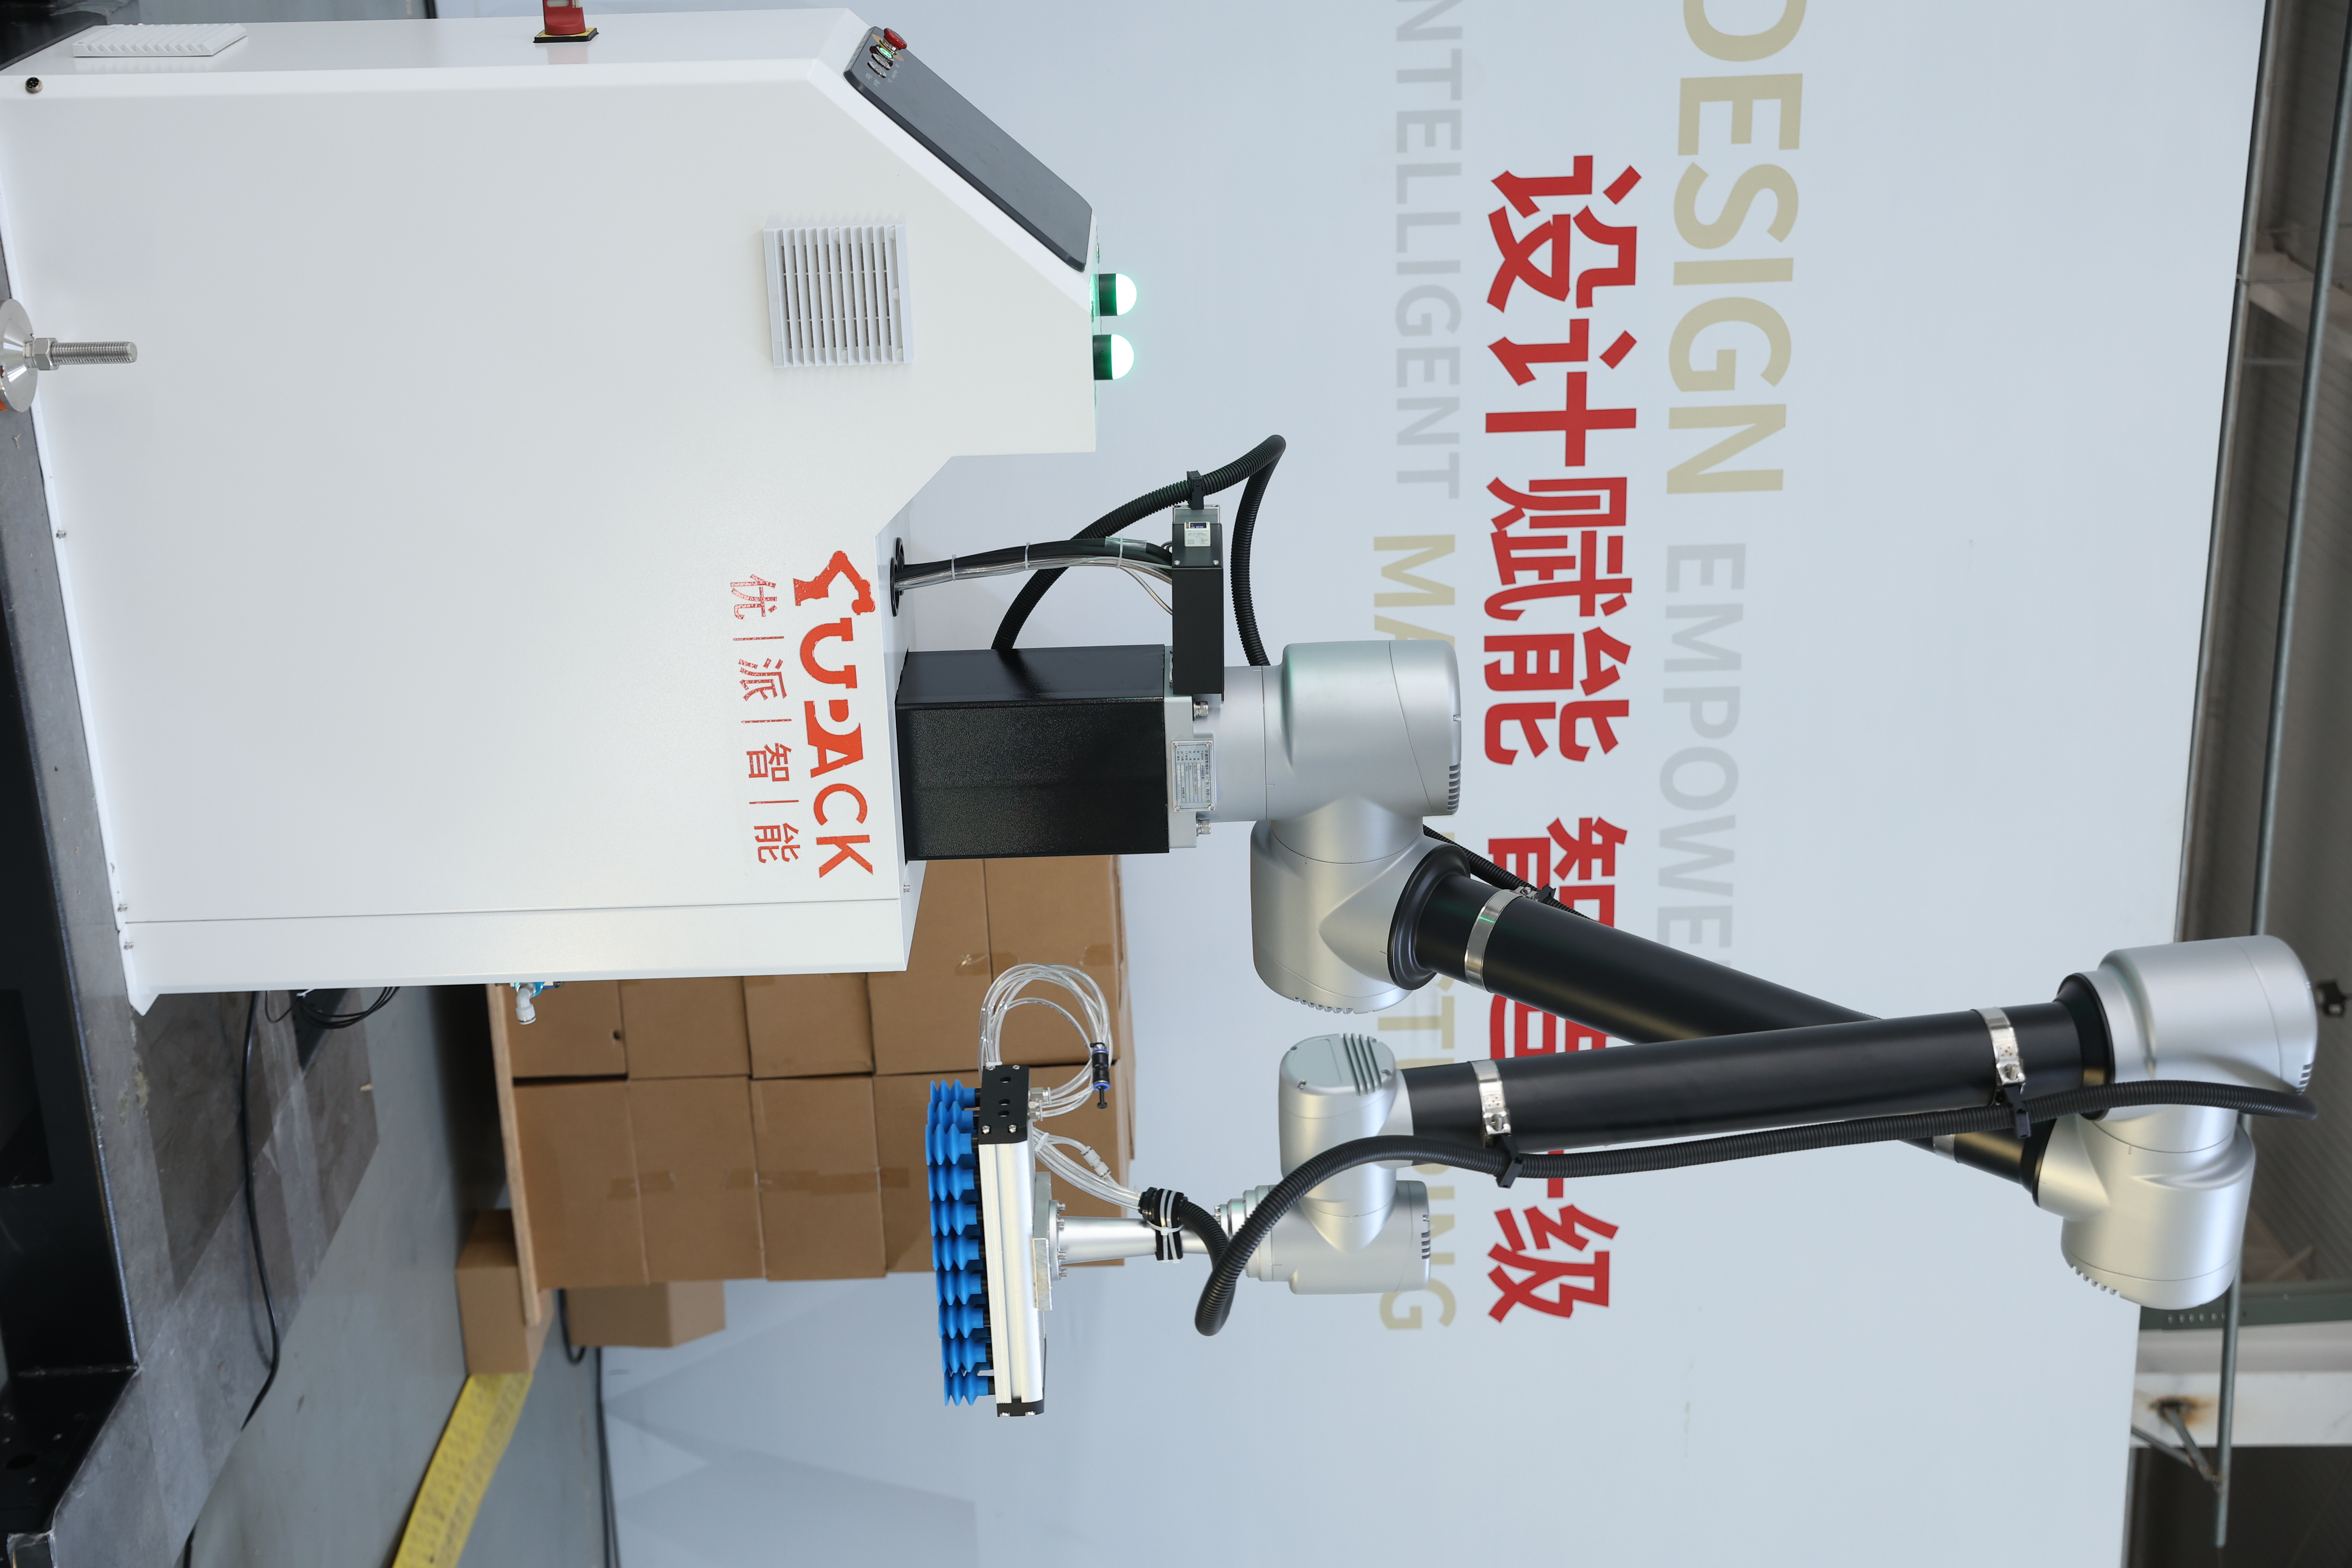
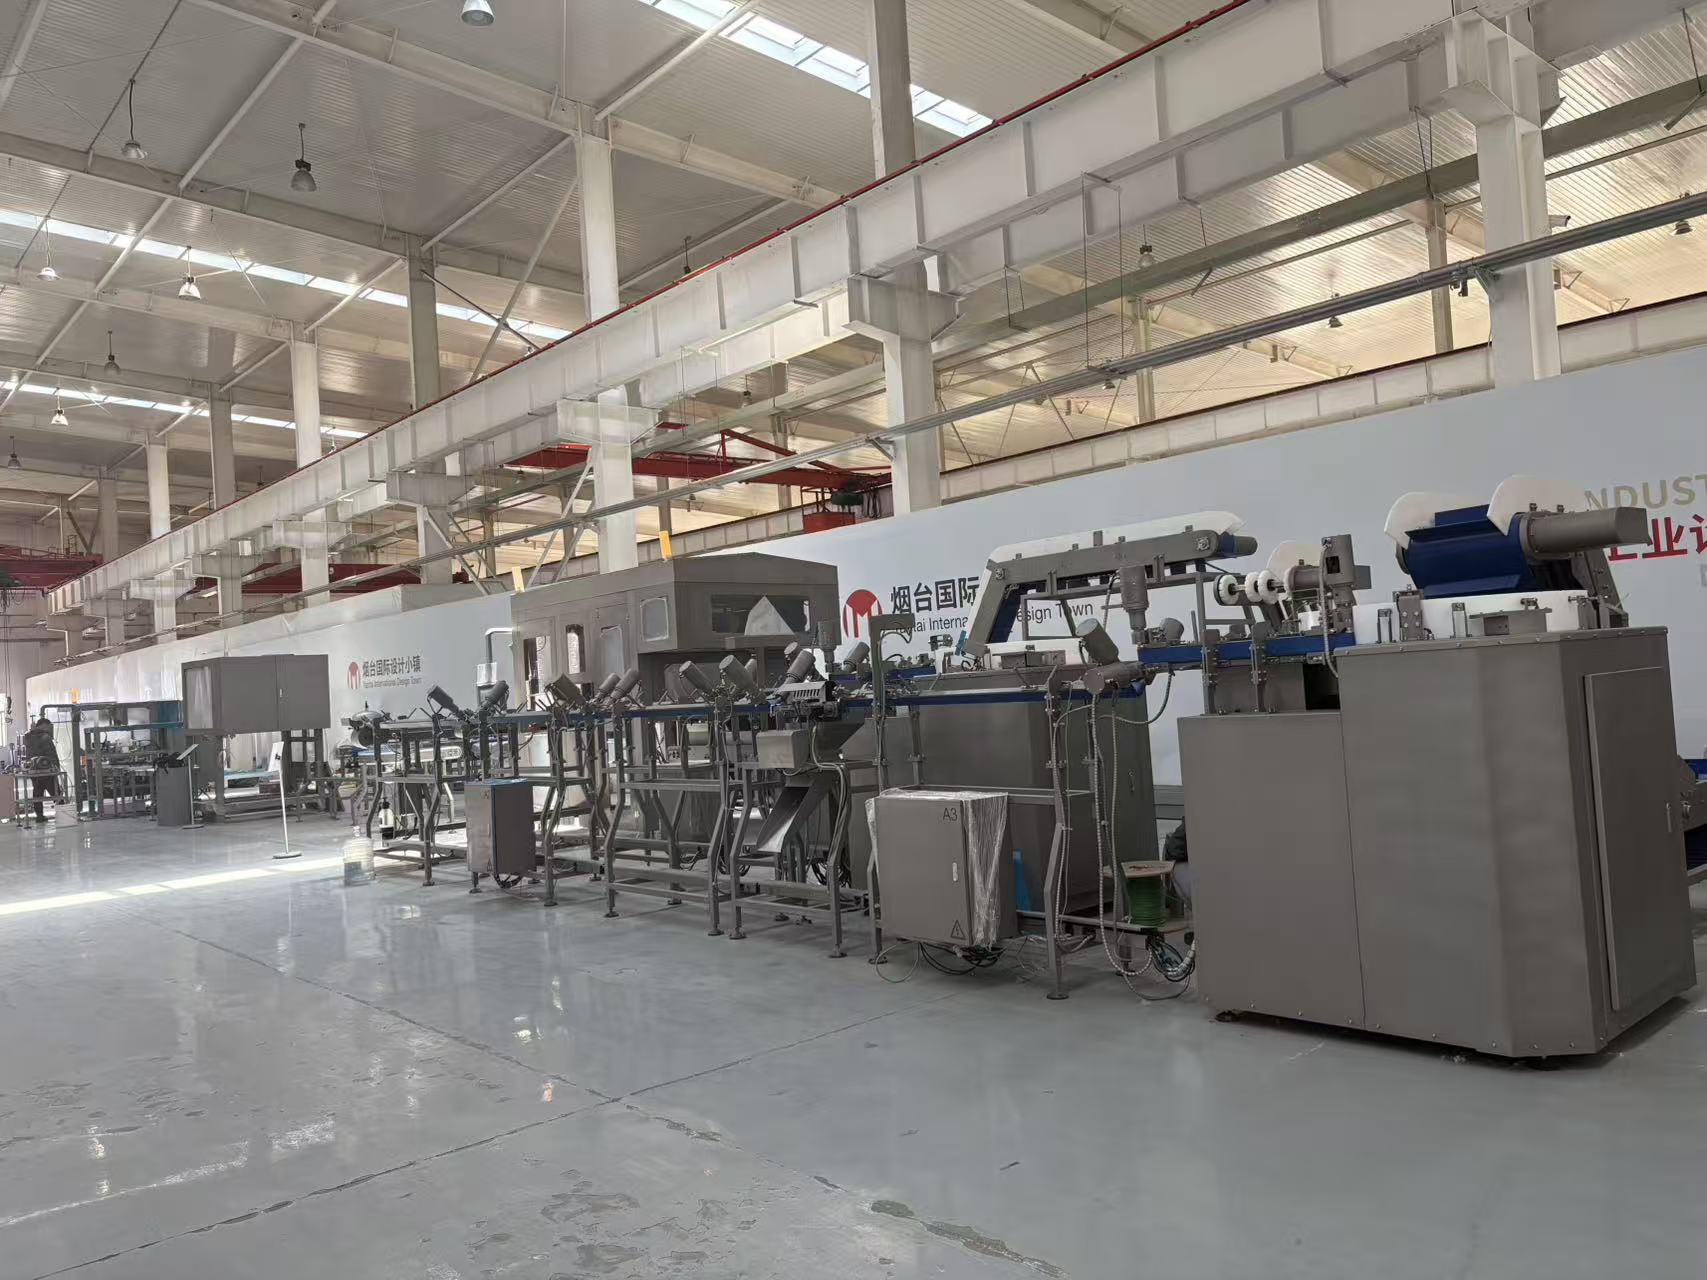
Custom conveyor systems represent a revolutionary approach to material handling and product transportation across diverse industries. These specialized systems are engineered to meet specific operational requirements, delivering tailored solutions that standard equipment simply cannot provide. Custom conveyor systems integrate advanced technology with flexible design principles to address unique business challenges.
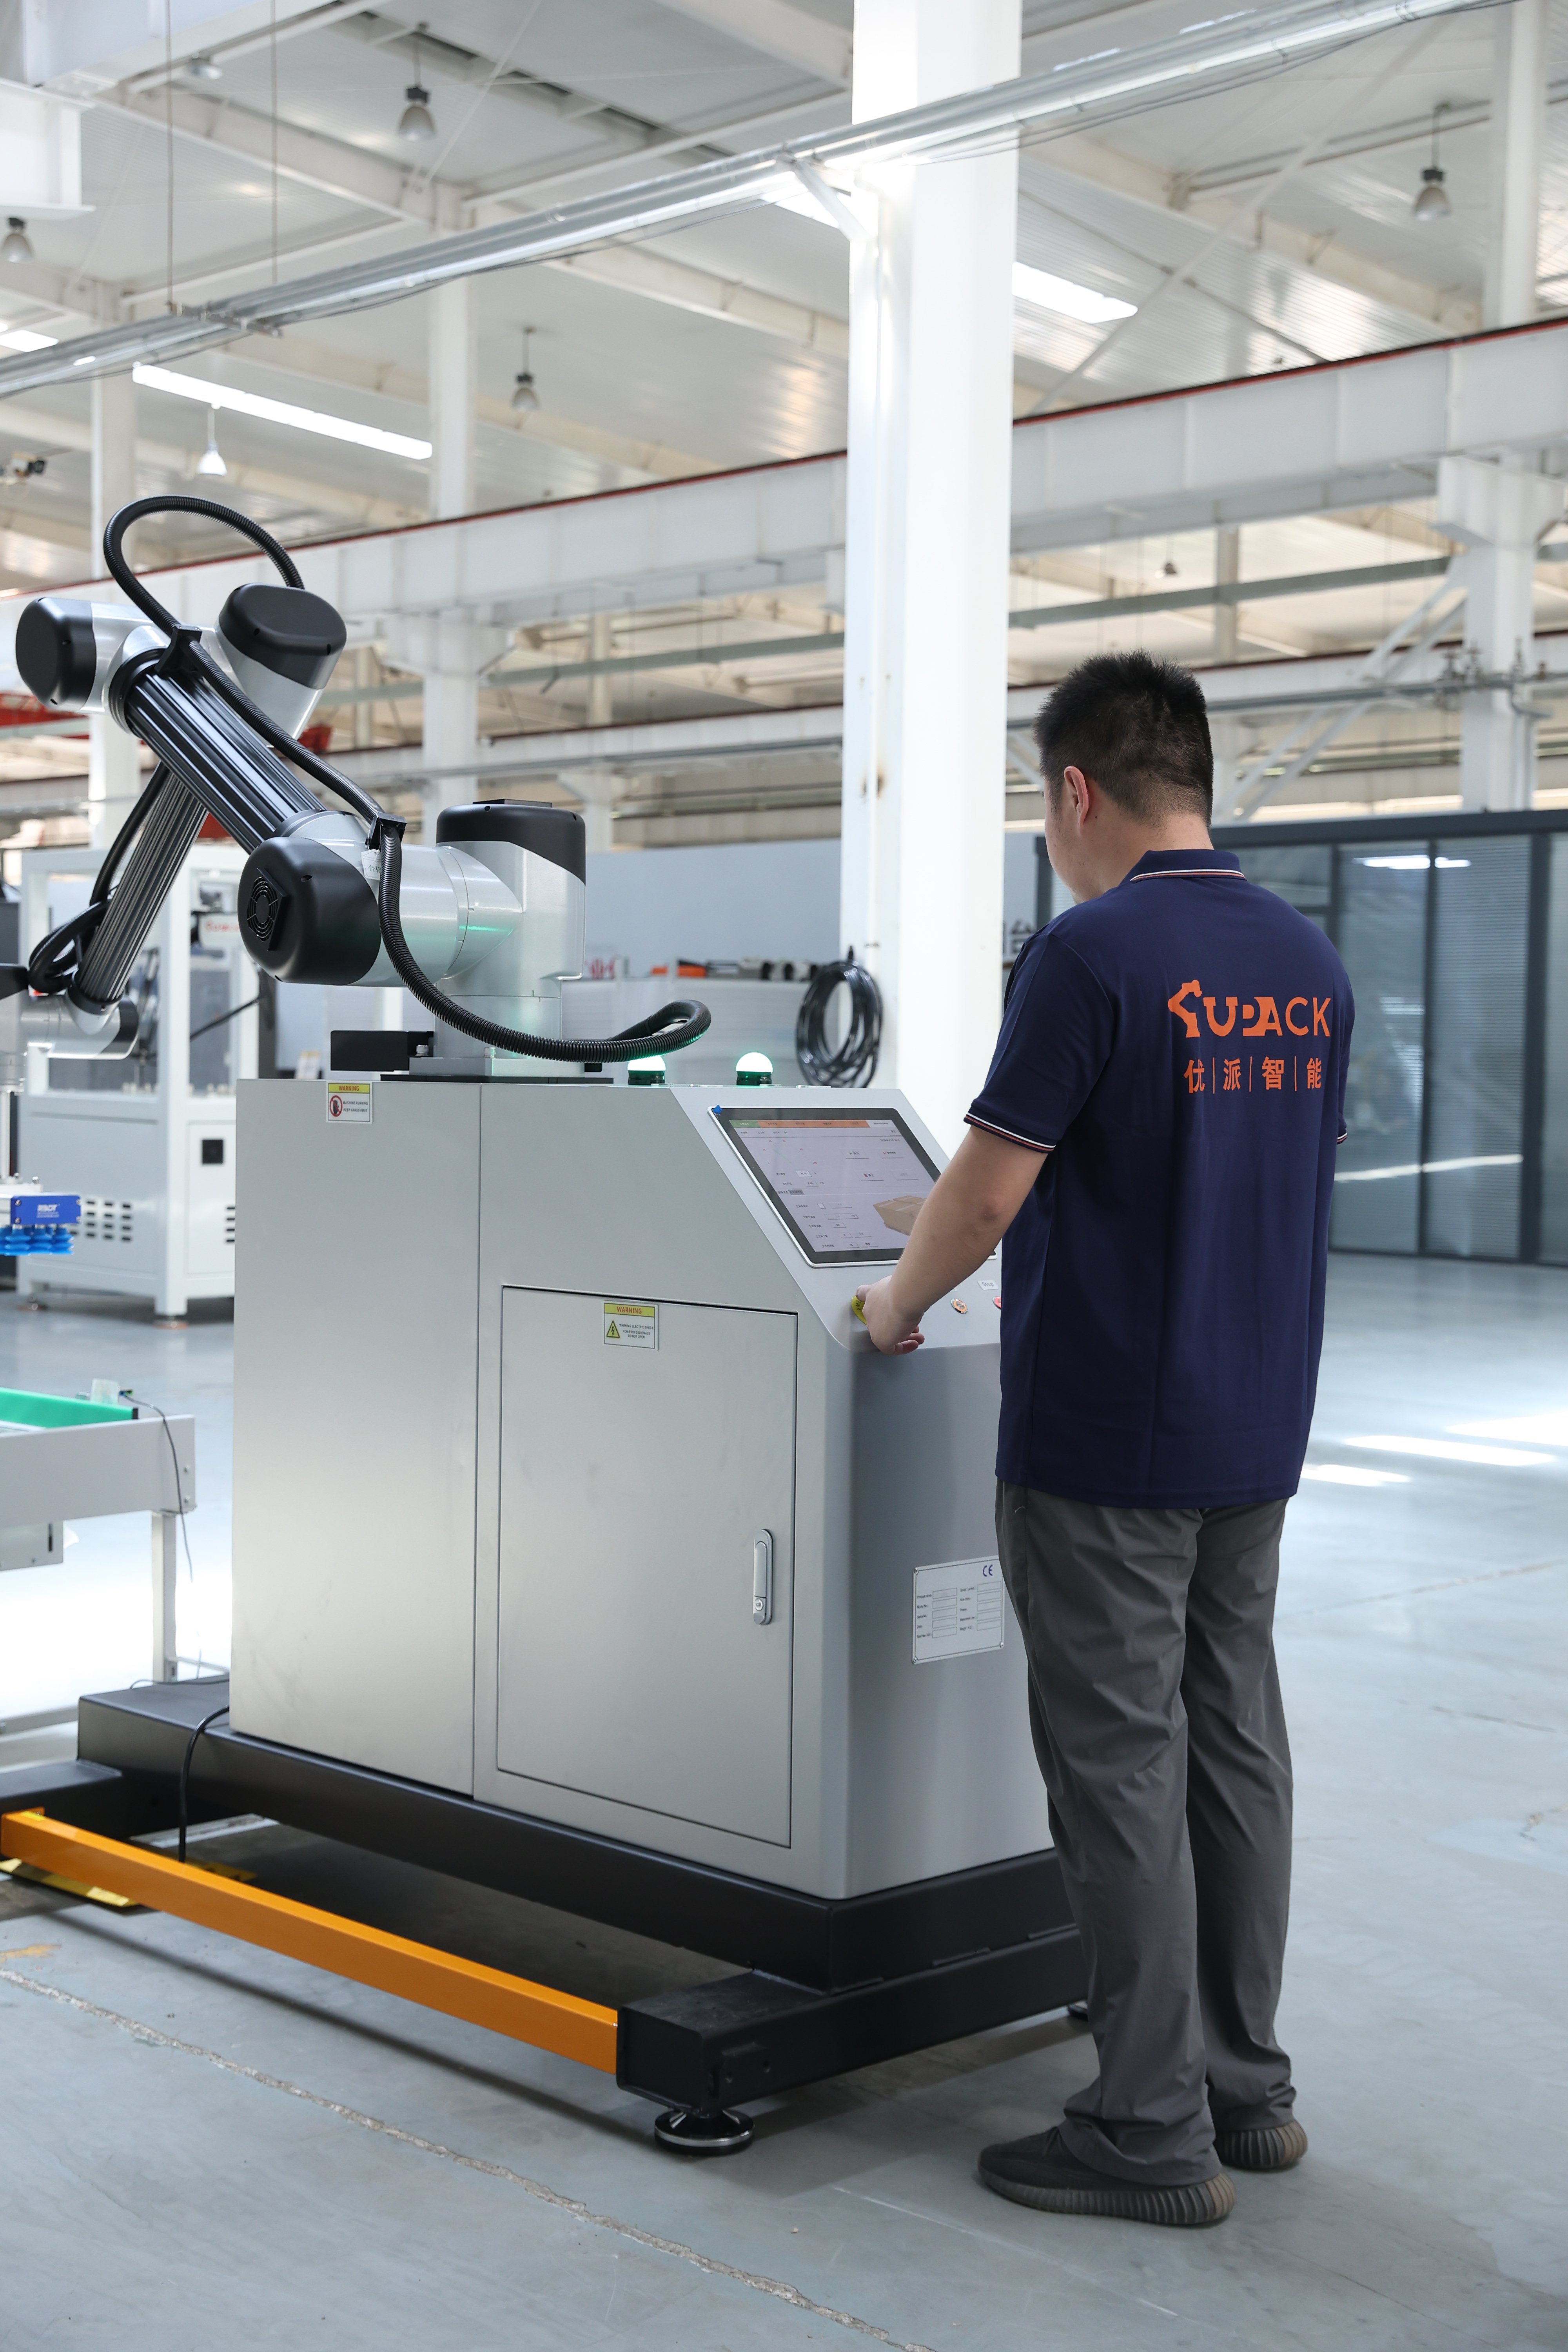
The primary function of custom conveyor systems involves moving products, materials, and components efficiently through manufacturing facilities, warehouses, and distribution centers. These systems automate repetitive handling tasks, significantly reducing manual labor and increasing throughput. Custom conveyor systems feature intelligent control mechanisms that adapt to varying load capacities, speeds, and environmental conditions.
Technologically, custom conveyor systems incorporate servo motors, variable frequency drives, and real-time monitoring sensors. These components work synergistically to optimize performance and prevent costly downtime. Advanced automation capabilities allow custom conveyor systems to integrate seamlessly with existing production infrastructure and enterprise software systems.
Applications for custom conveyor systems span numerous sectors including food processing, automotive manufacturing, pharmaceuticals, e-commerce fulfillment, and heavy industries. Custom conveyor systems excel in scenarios requiring specialized handling of fragile items, hazardous materials, or precision-engineered products. Whether managing high-speed sorting operations or delicate product transfers, custom conveyor systems provide reliable performance tailored to specific operational demands and future scalability requirements.

 EN


