machine labeling
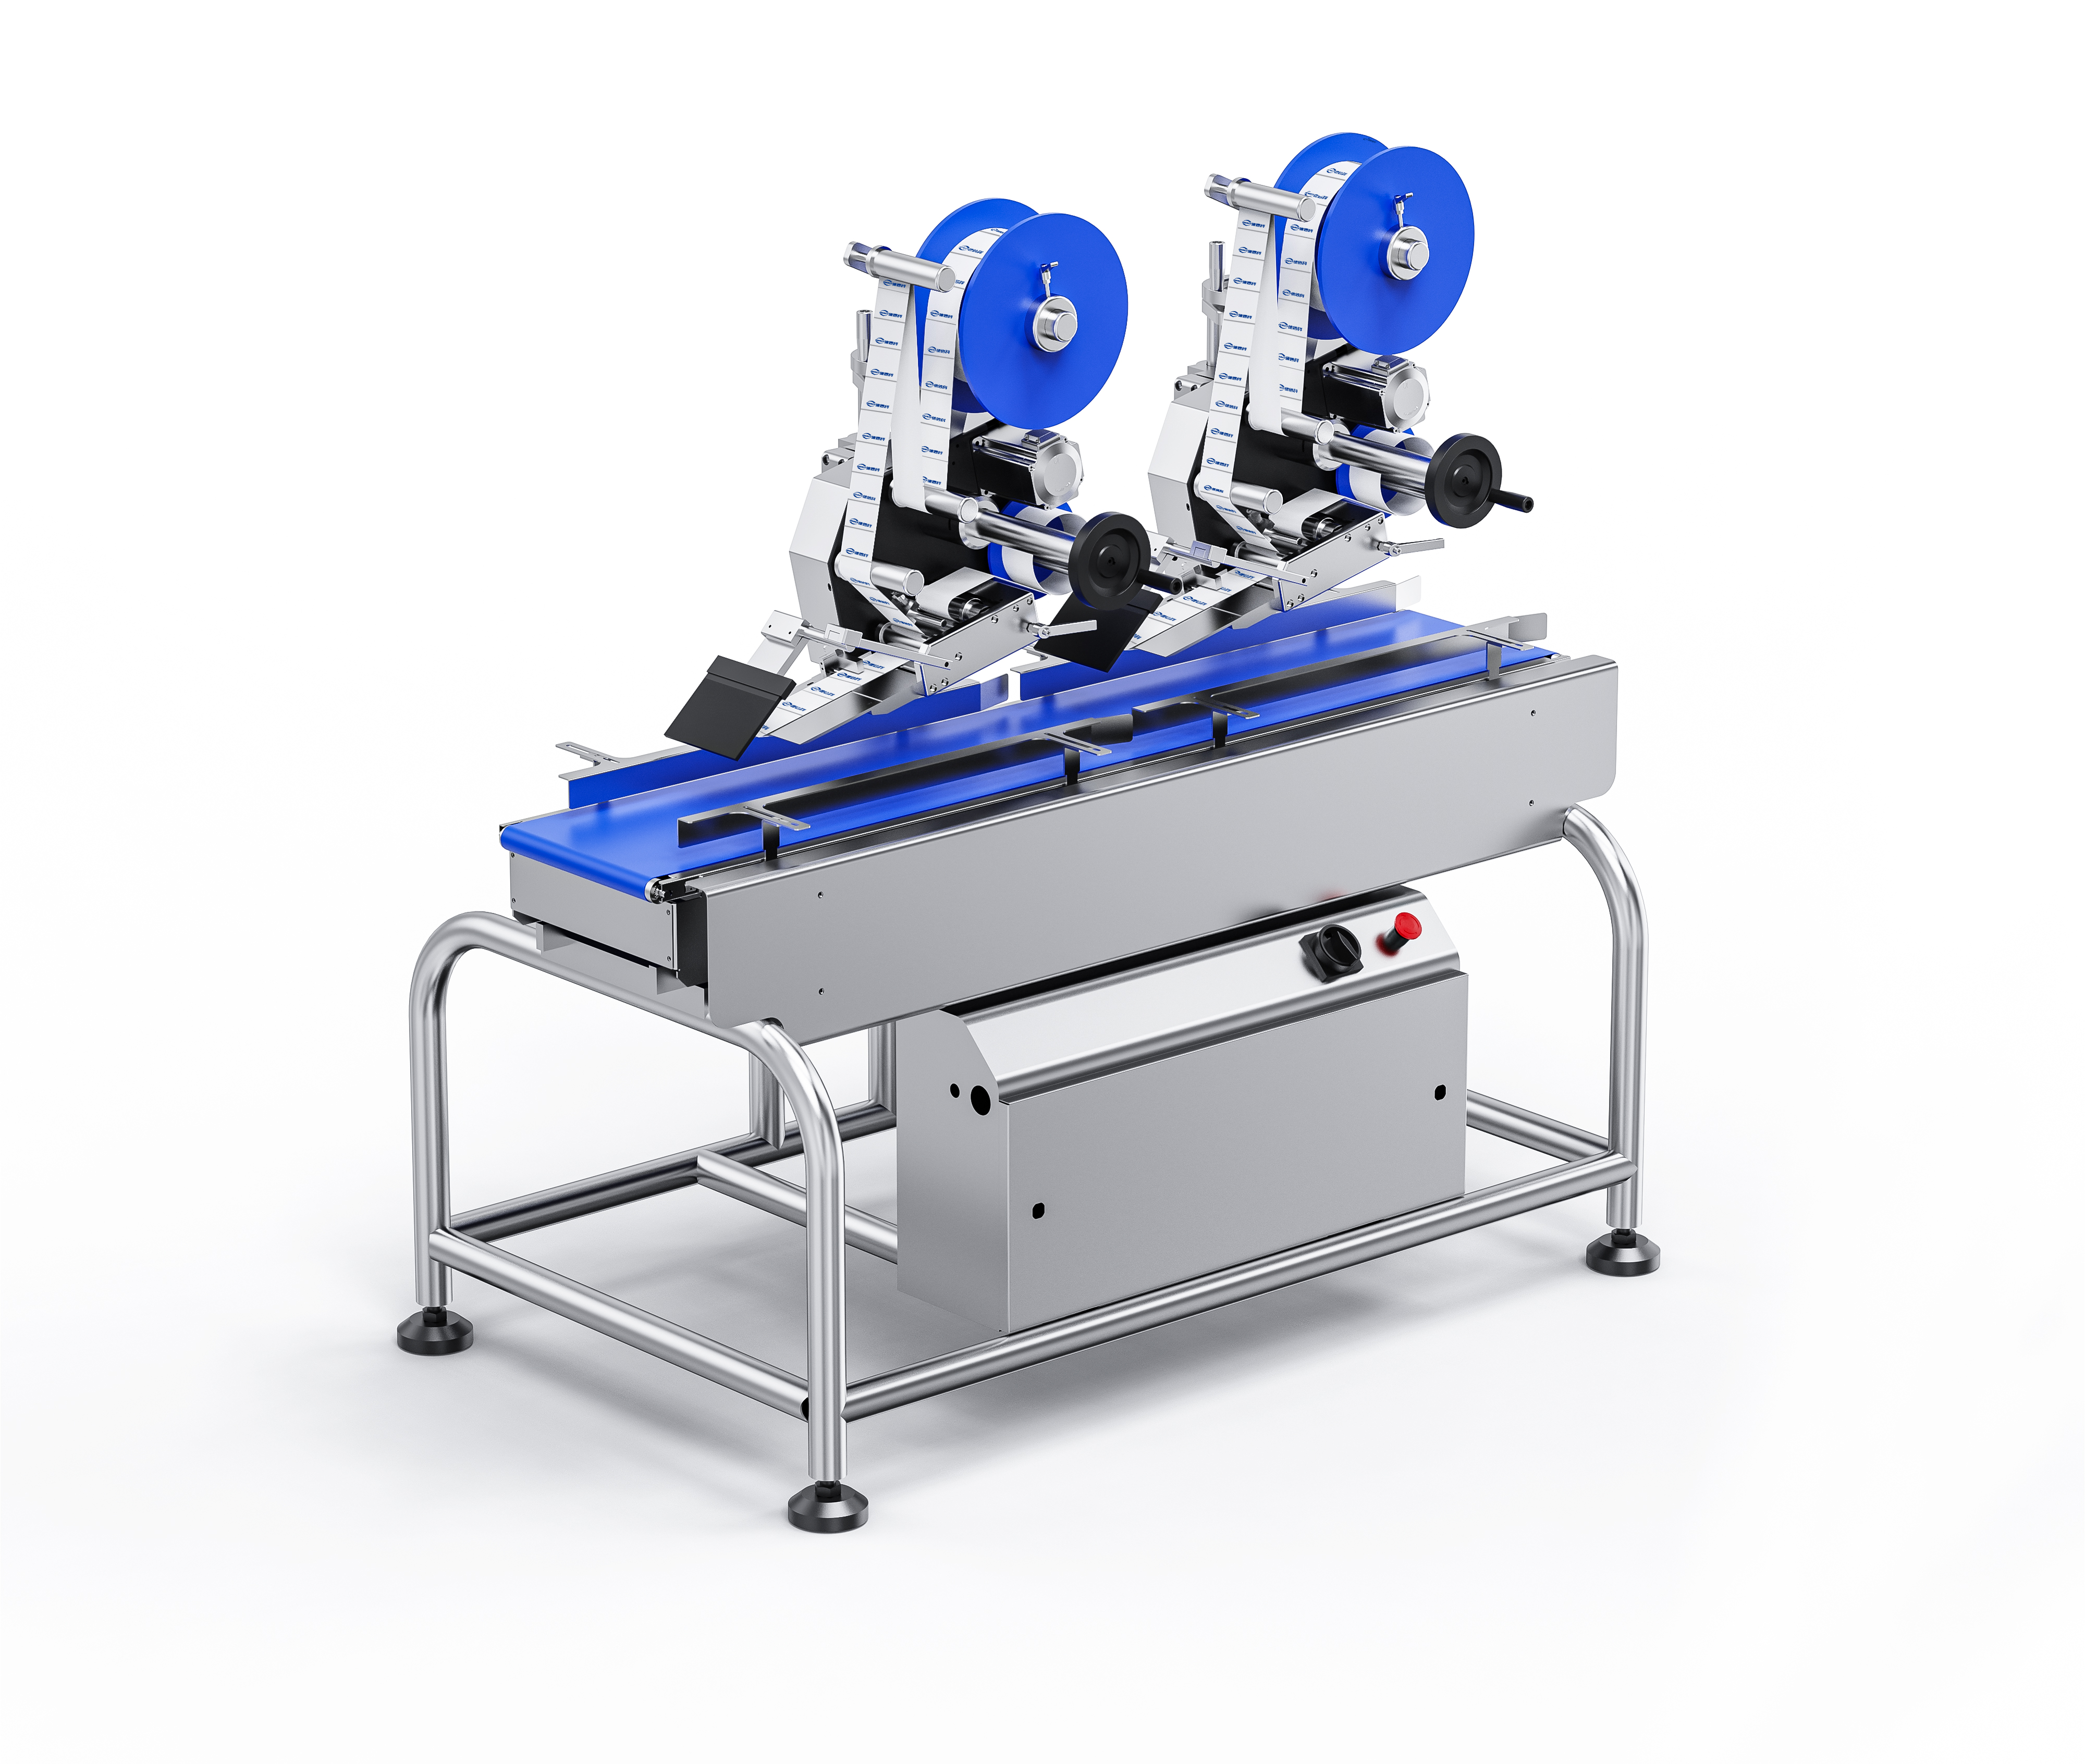
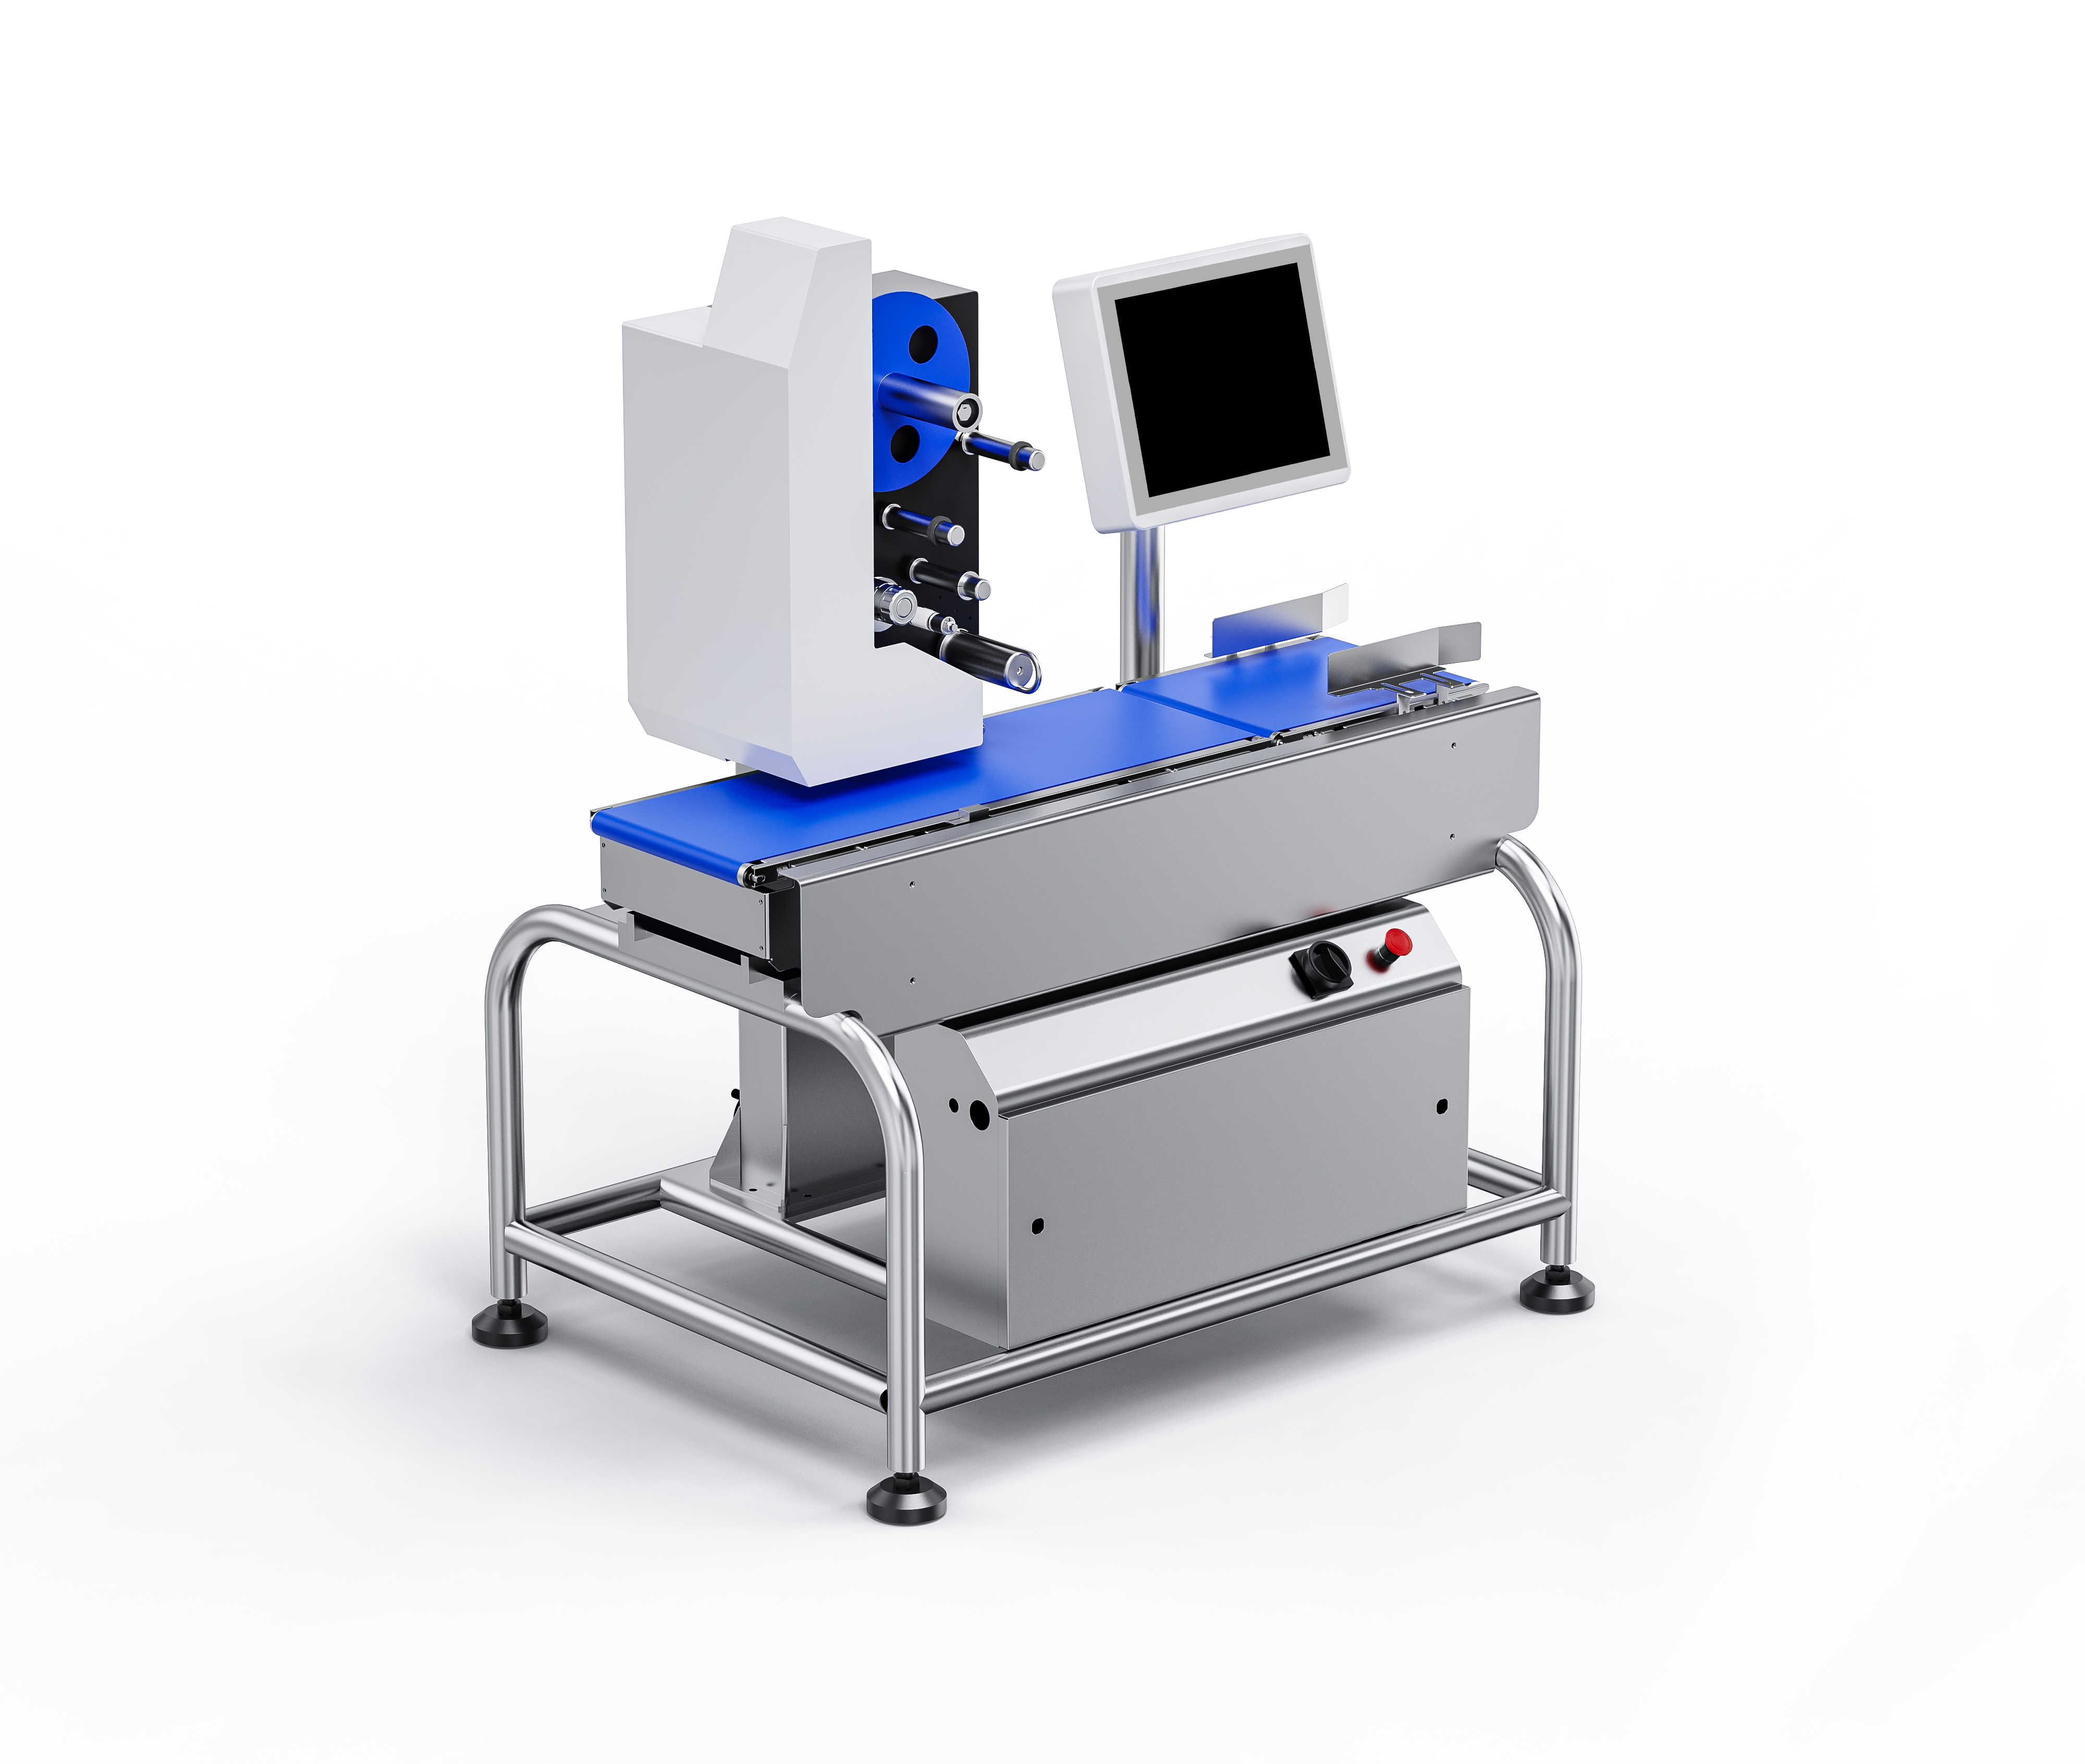
Machine labeling represents a sophisticated automation solution designed to streamline product identification and tracking processes across diverse industries. This technology encompasses automated systems that apply labels to products with precision and consistency, eliminating manual labeling inefficiencies. Machine labeling systems utilize advanced vision technology, conveyor integration, and intelligent positioning mechanisms to ensure accurate label placement on items of varying shapes and sizes.
The core functionality of machine labeling involves detecting product position, calculating optimal label placement, and dispensing adhesive labels at high speeds. Modern machine labeling equipment incorporates sensor technology that communicates with control systems to maintain perfect synchronization throughout the production line. Machine labeling solutions adapt to different label dimensions, substrate materials, and application requirements without requiring extensive reconfiguration.
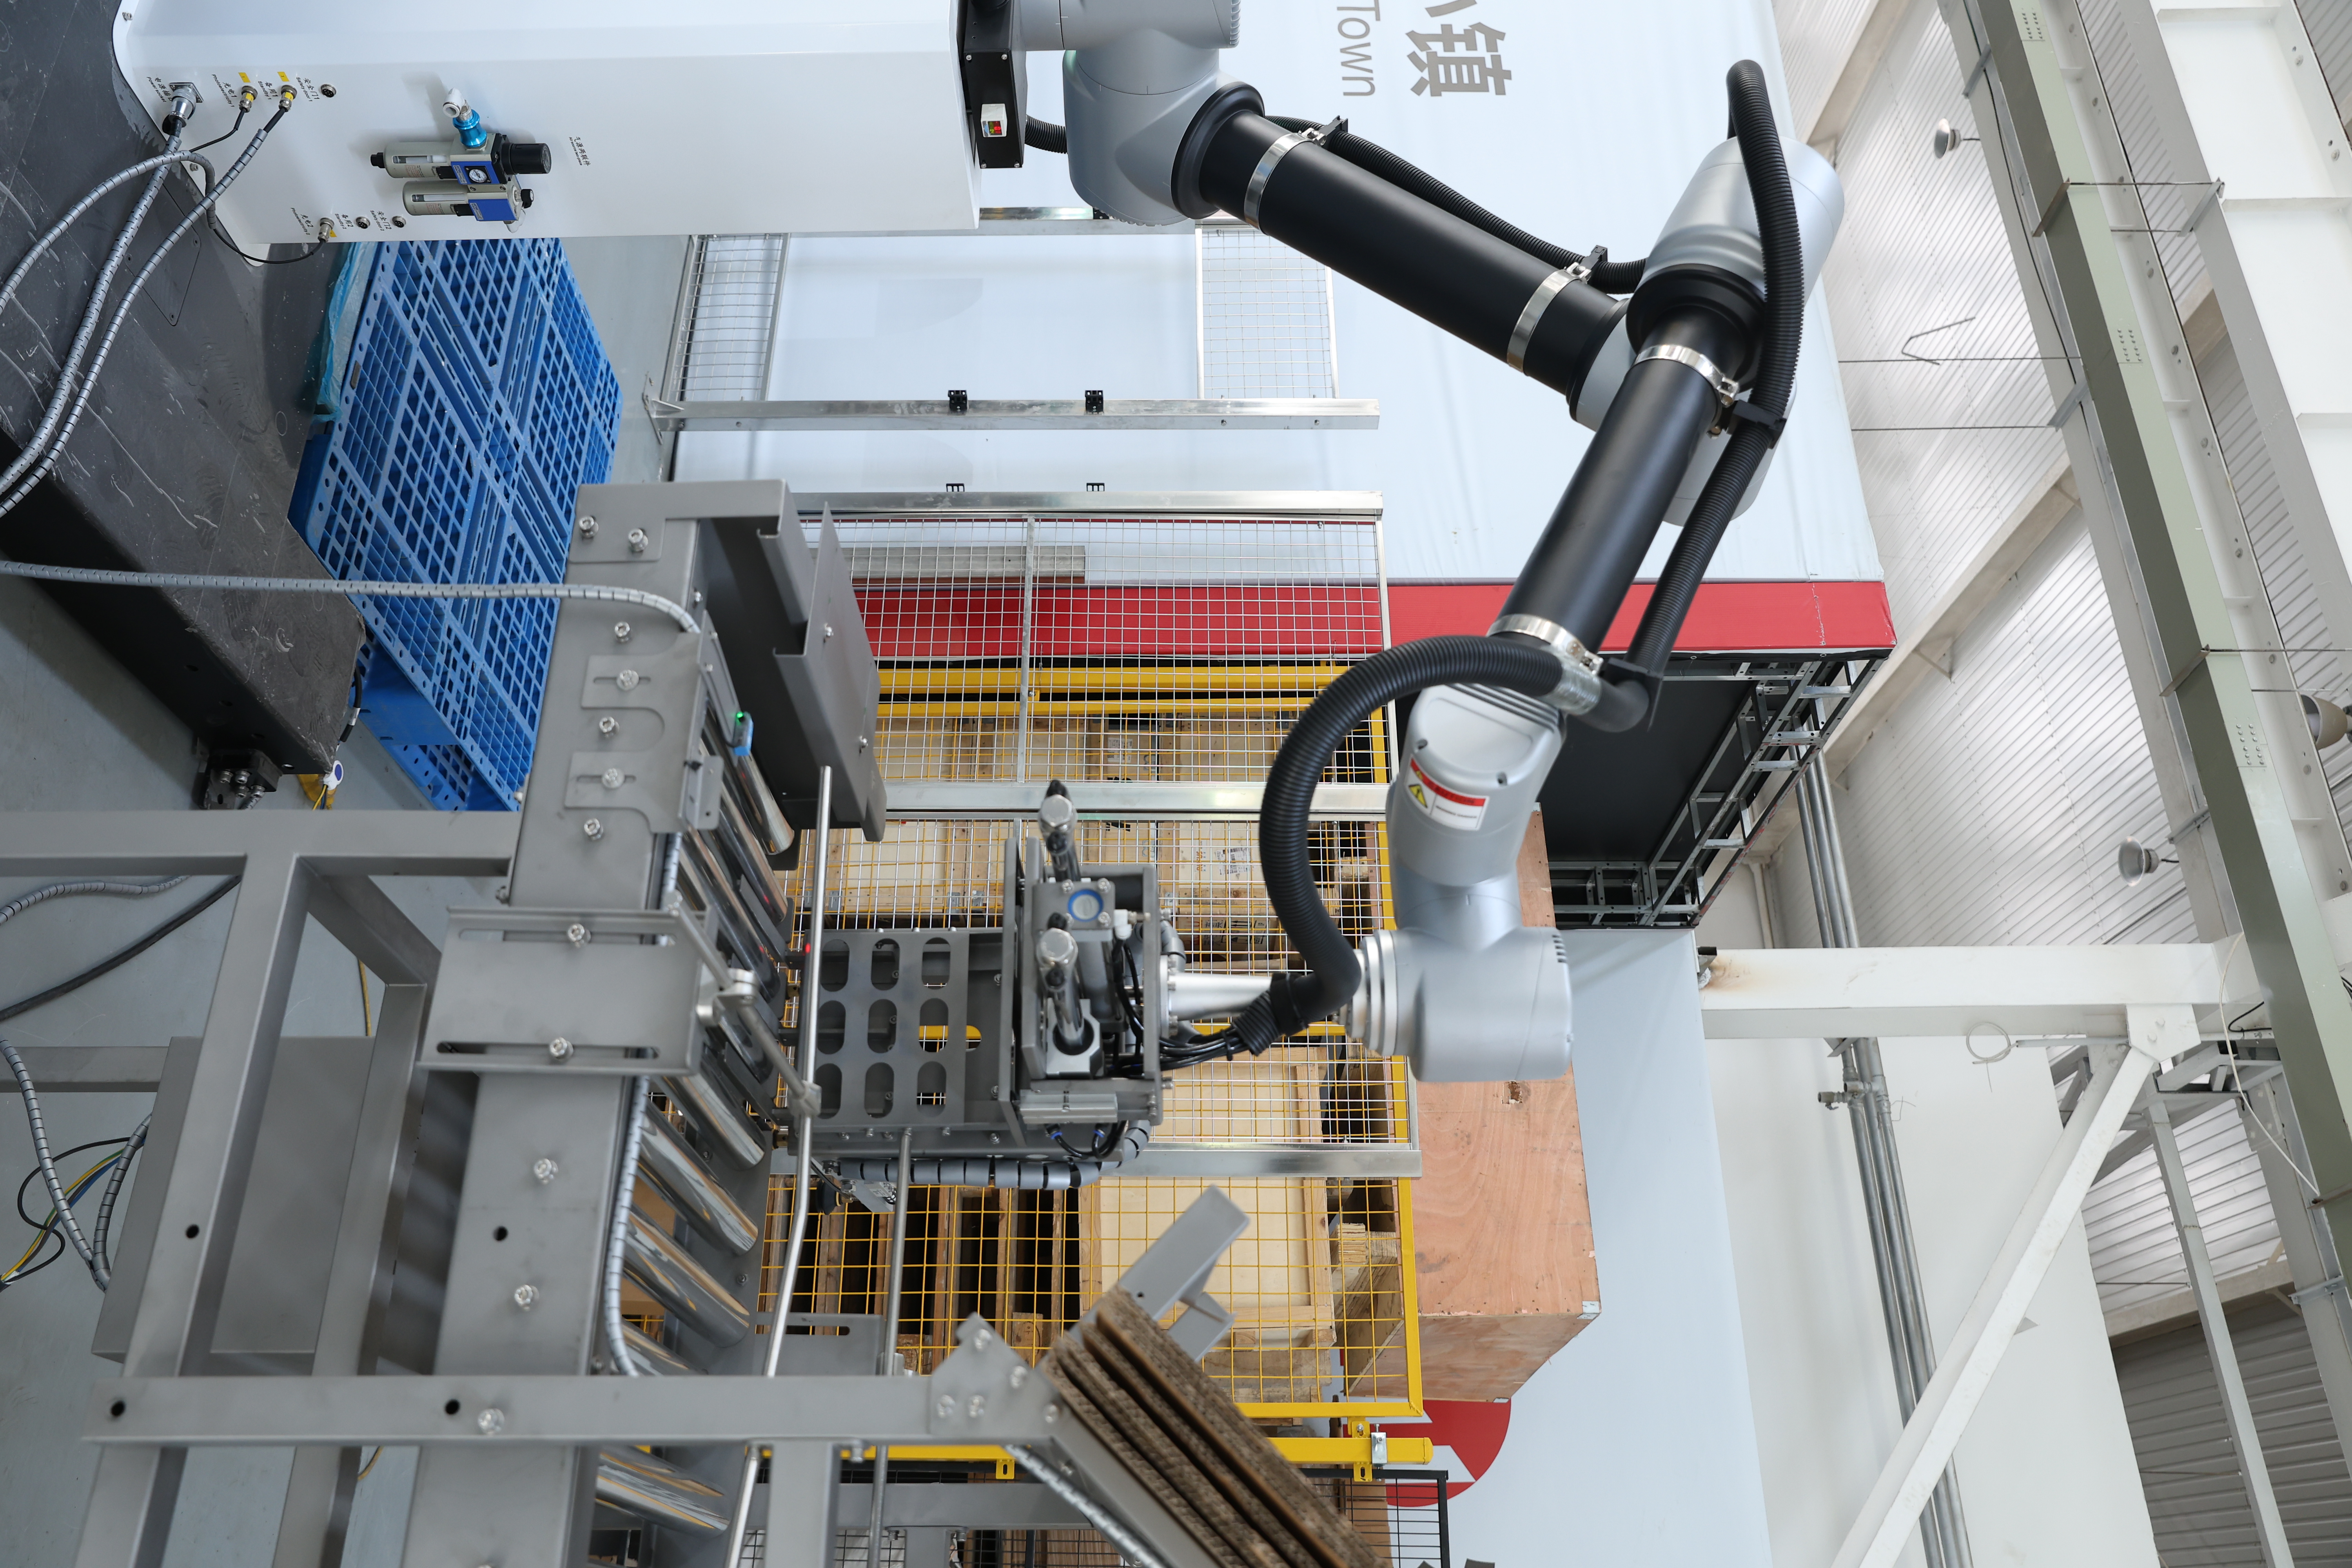
Technological features of contemporary machine labeling systems include real-time quality verification, adjustable application speeds ranging from modest to high-volume production rates, and compatibility with various label stock materials. The integration of machine labeling into existing production environments requires minimal disruption, as most systems feature modular designs enabling seamless incorporation into current workflows.
Applications for machine labeling span retail product packaging, pharmaceutical containers, food and beverage products, cosmetics, industrial goods, and logistics operations. Machine labeling technology proves invaluable in environments demanding consistent branding presentation, regulatory compliance, and operational efficiency. Industries relying on machine labeling experience significant improvements in production throughput, cost reduction, and quality assurance outcomes.

 EN


