case palletizer
A case palletizer is an automated material handling system designed to organize, arrange, and stack cases onto pallets with precision and efficiency. This sophisticated equipment represents a critical advancement in warehouse automation, streamlining operations across manufacturing, distribution, and logistics facilities.
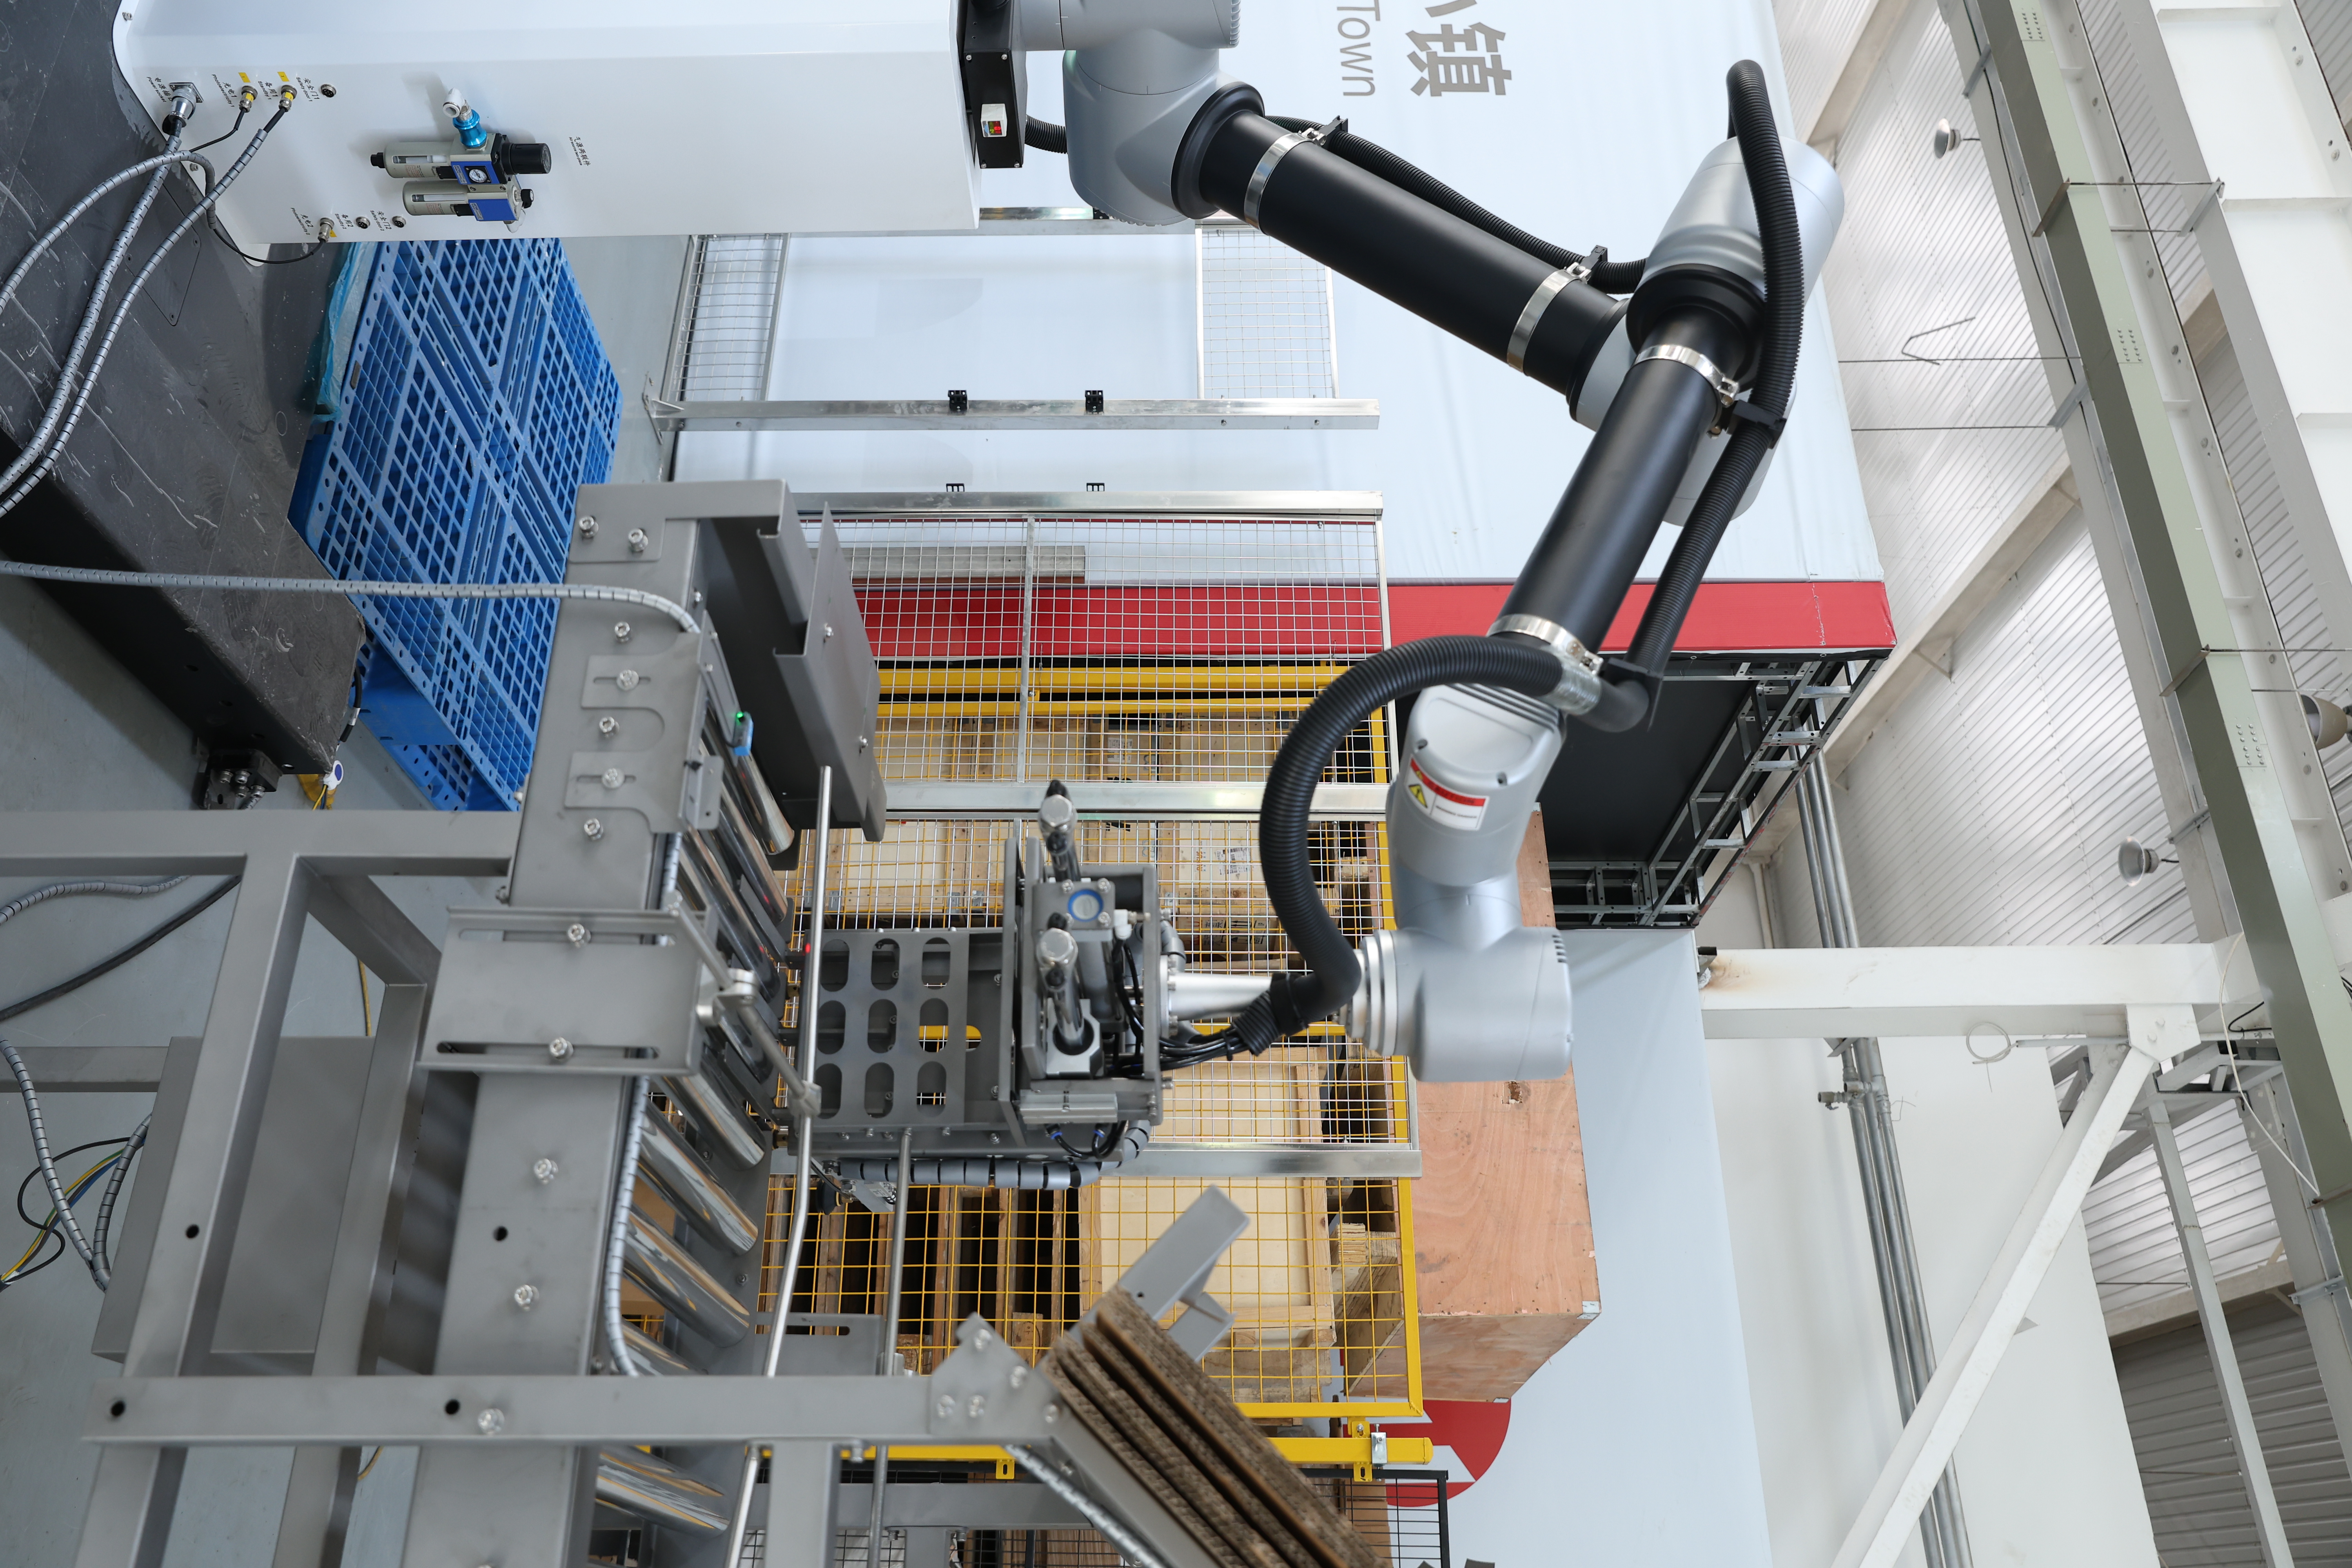
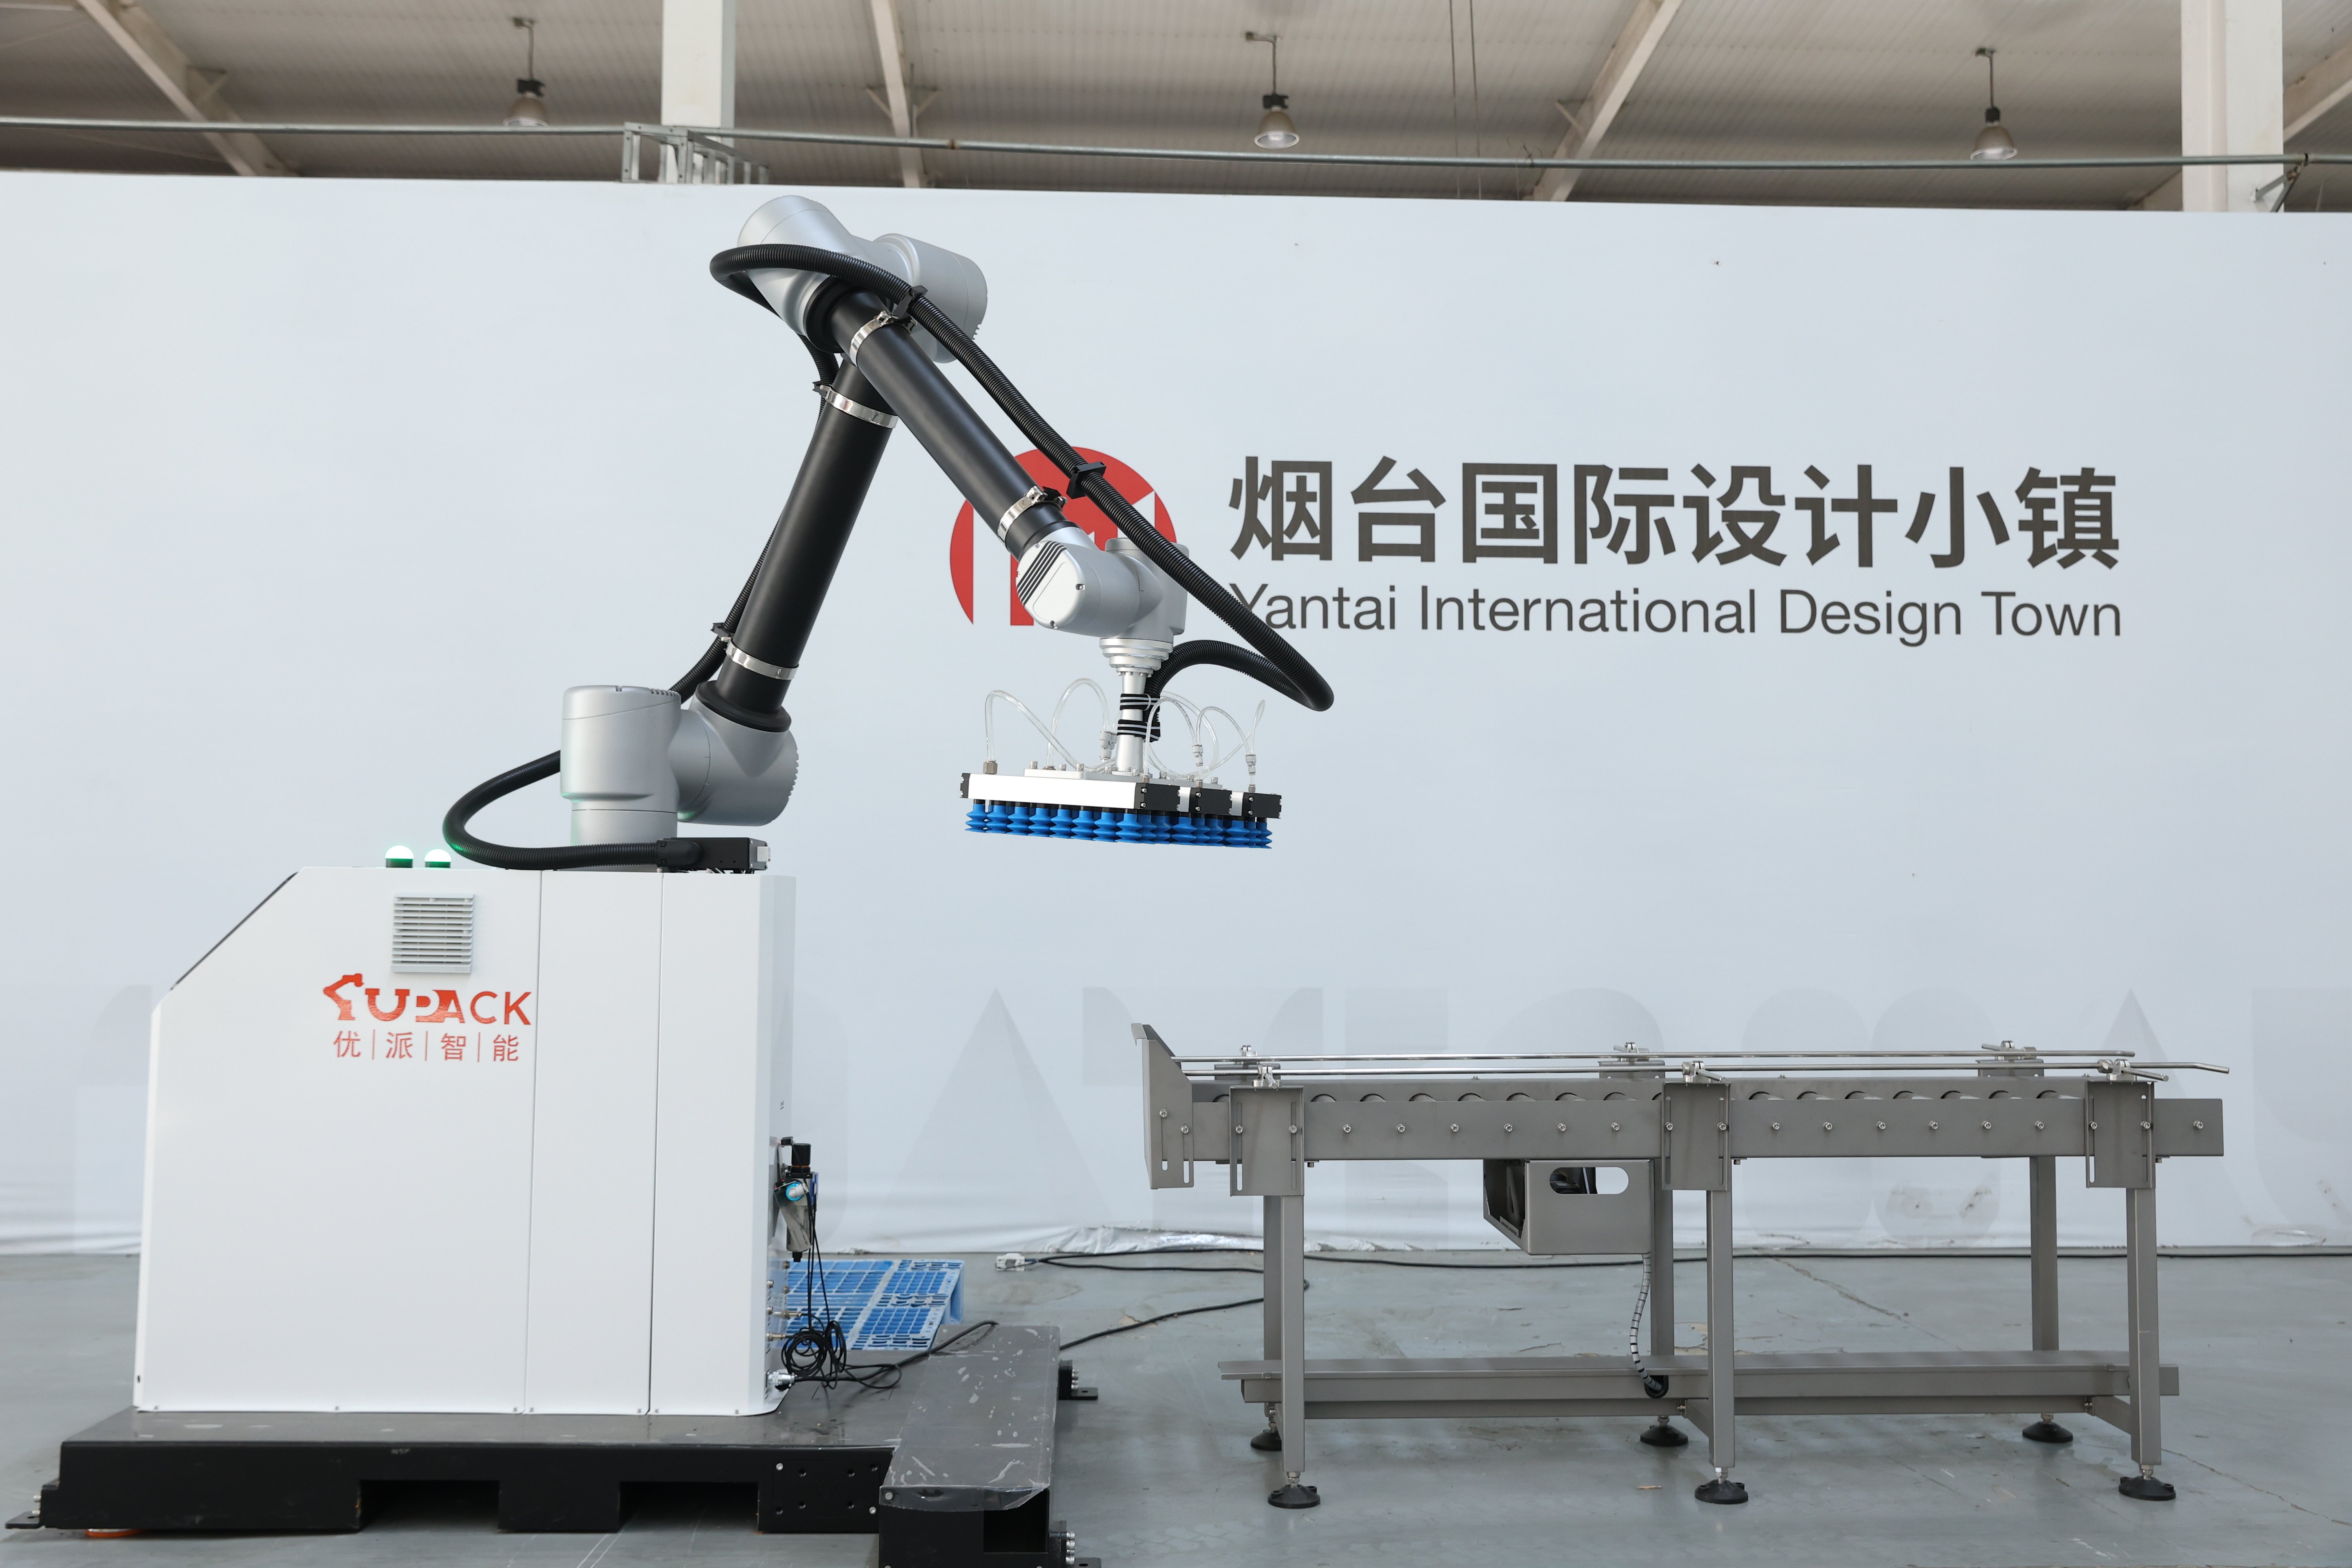
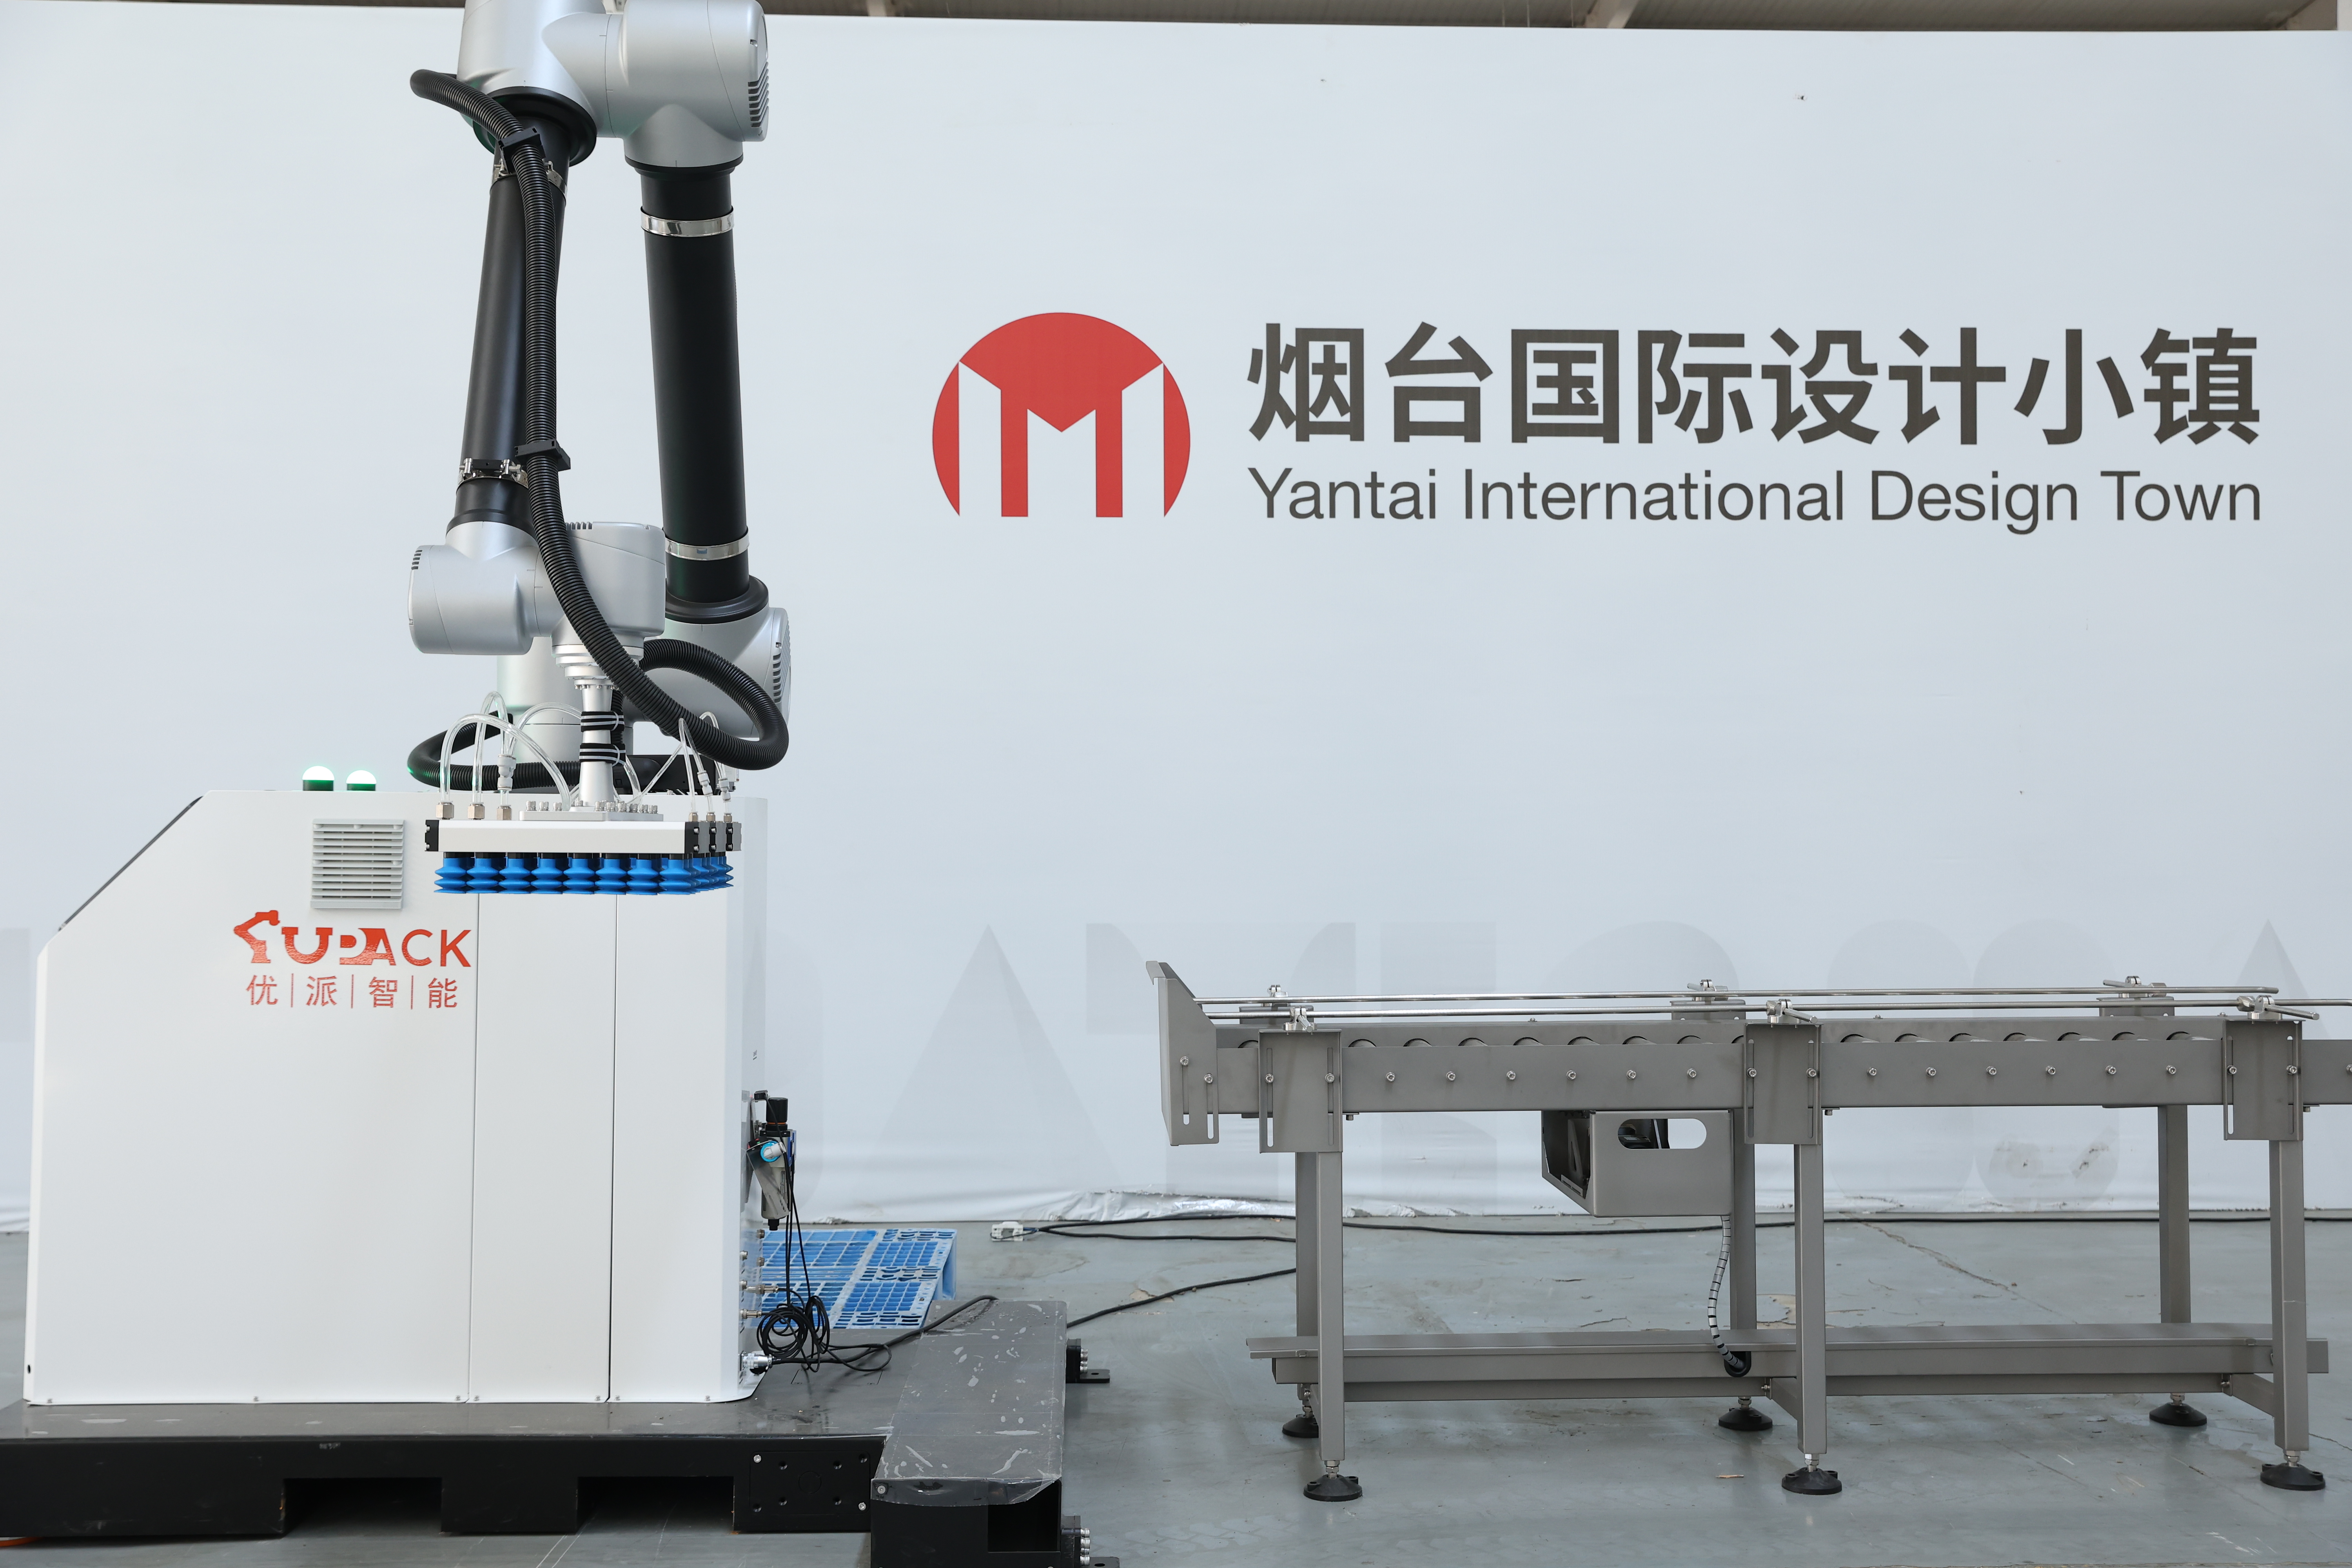
The primary function of a case palletizer involves receiving cases from conveyor systems, positioning them according to predetermined patterns, and systematically stacking them onto pallets. Modern case palletizers utilize advanced robotic arms, pneumatic systems, and computer controls to execute these tasks with remarkable accuracy and speed. The case palletizer technology incorporates intelligent sensors and vision systems that detect case dimensions, weights, and orientations, ensuring optimal placement every time.
Key technological features of a case palletizer include programmable logic controllers that manage stacking sequences, adjustable layer configurations, and automatic pallet detection systems. High-speed case palletizers can process hundreds of cases per hour, adapting seamlessly to various case sizes and weights without requiring extensive reconfiguration.
Applications for a case palletizer span numerous industries. Manufacturing facilities employ case palletizers for packaging consumer goods, beverages, and food products. Distribution centers rely on case palletizer systems to optimize warehouse space and accelerate order fulfillment. Pharmaceutical companies benefit from the precision and consistency that case palletizer equipment provides. Automotive suppliers and industrial manufacturers also depend on case palletizers to maintain production schedules and reduce manual labor demands. The versatility of case palletizer technology makes it indispensable for any operation requiring efficient case handling and pallet preparation.

 EN


