Case Packing Machine Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

case packing machine

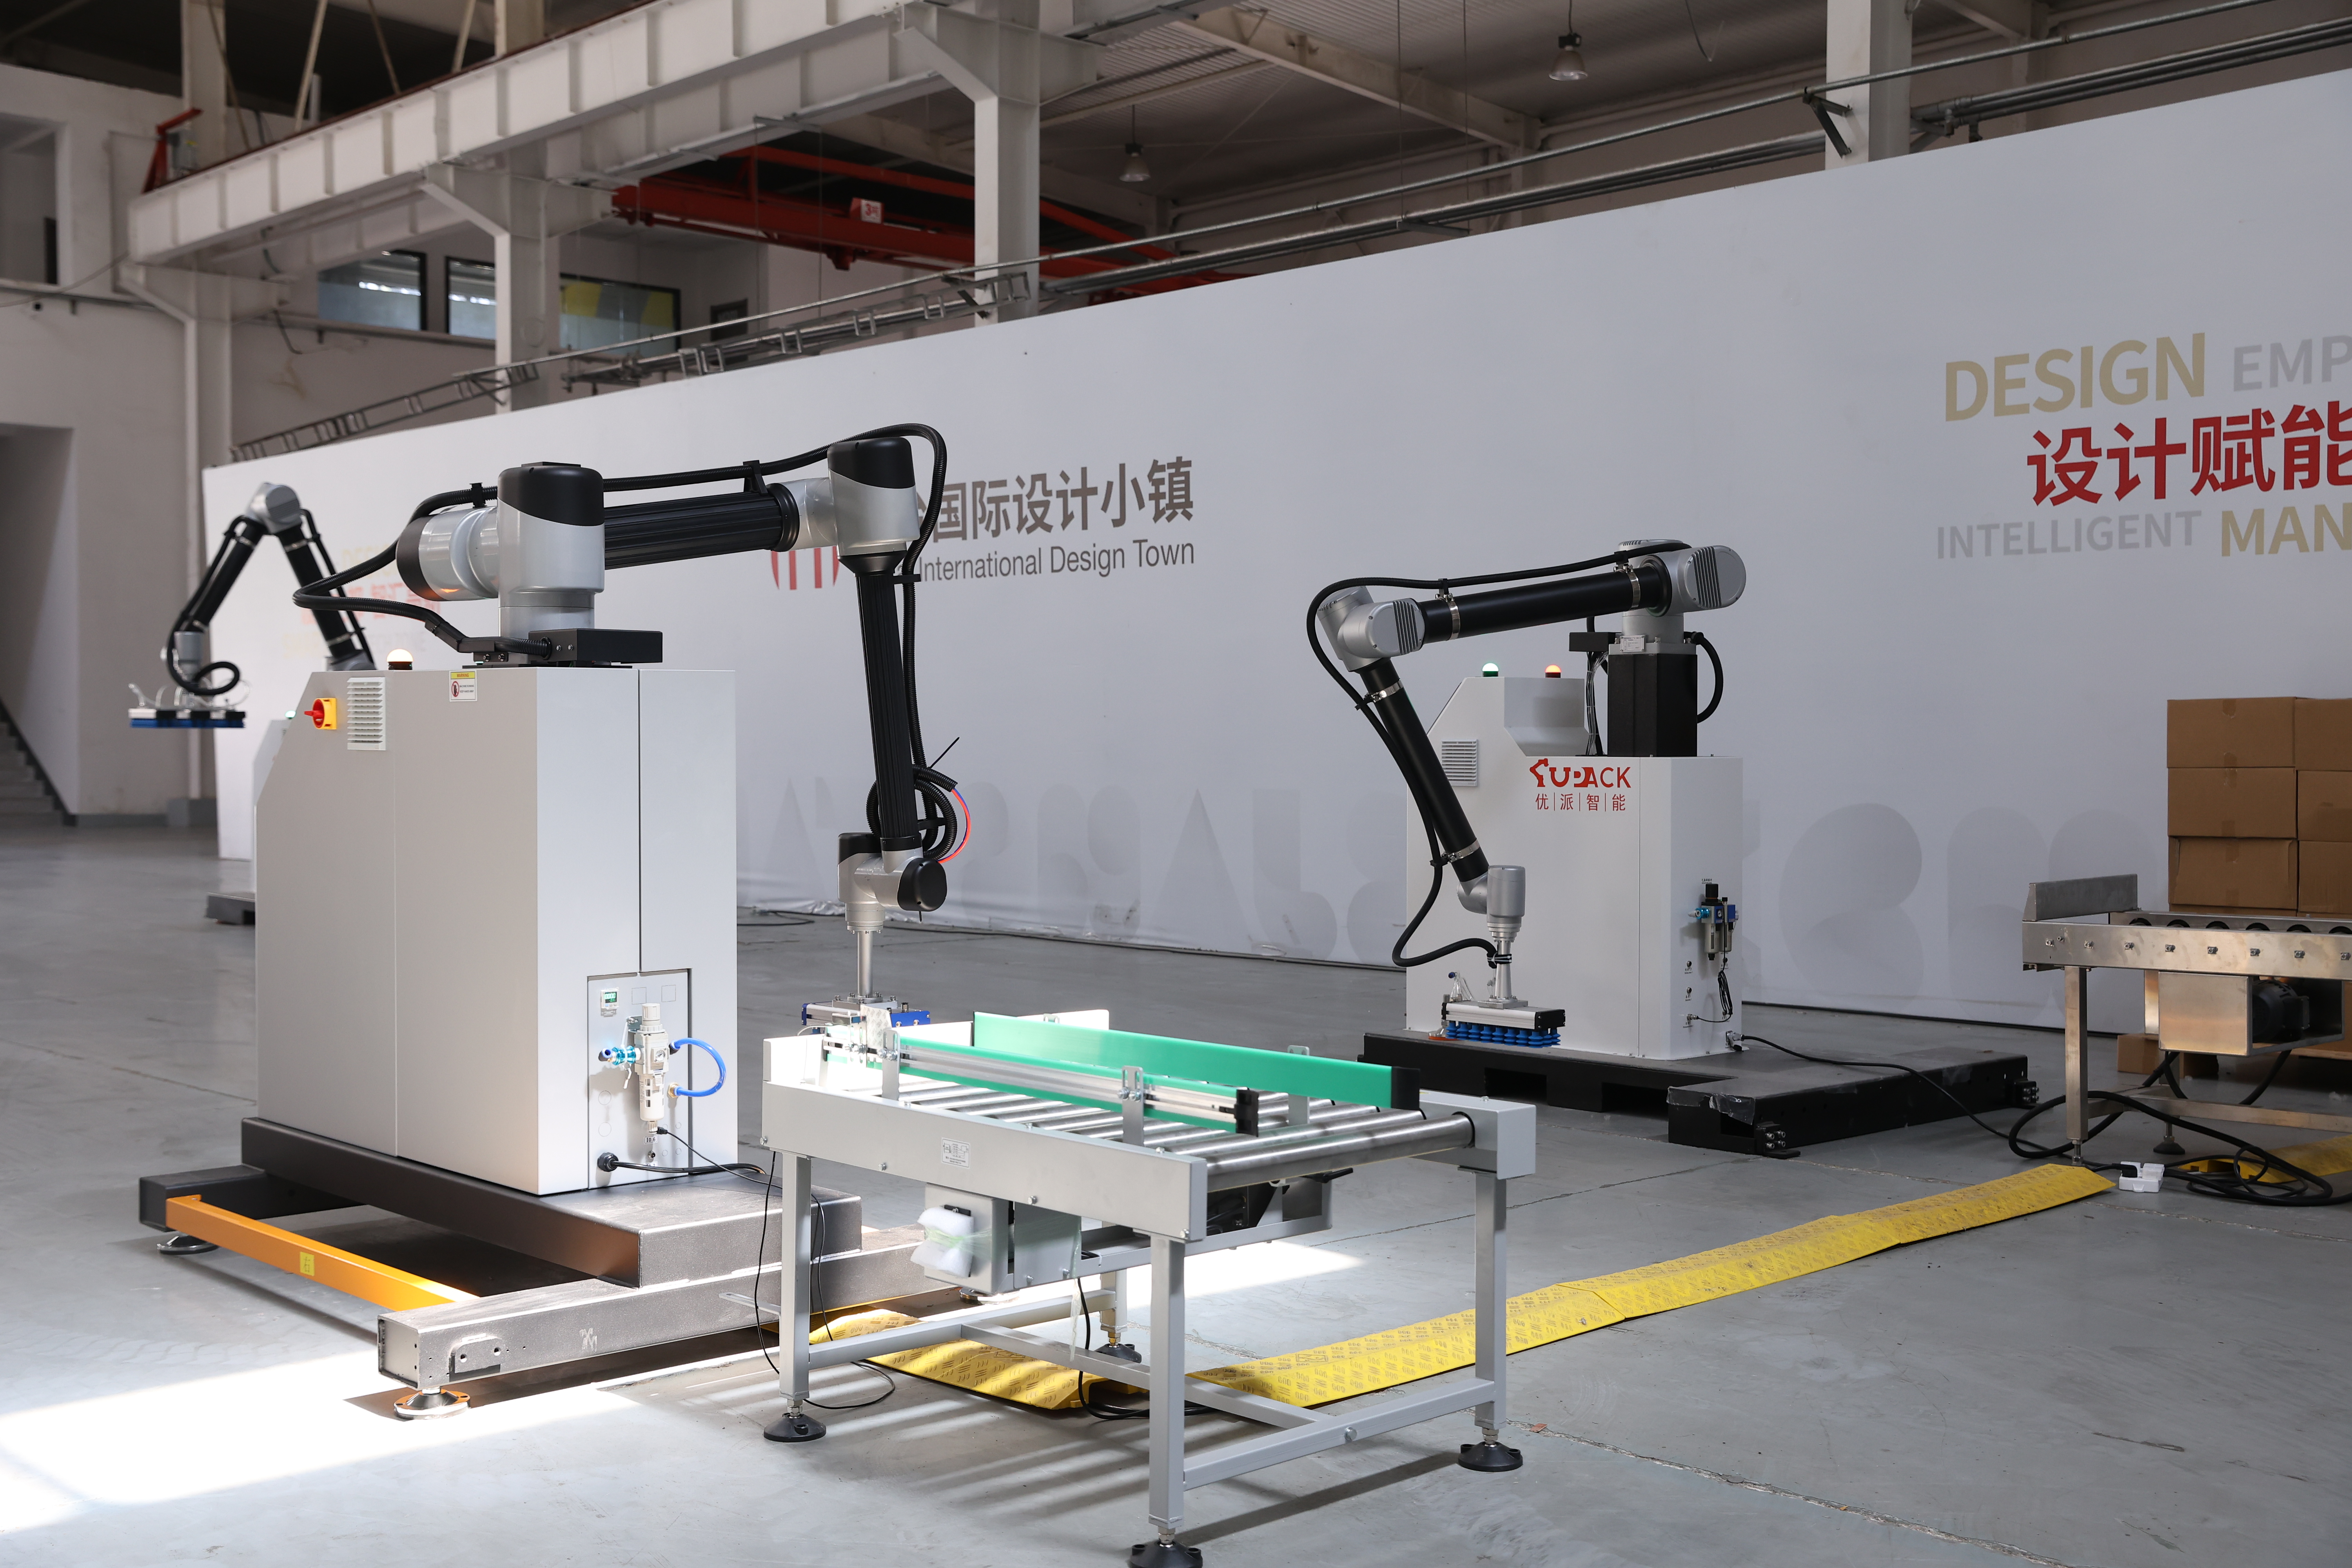
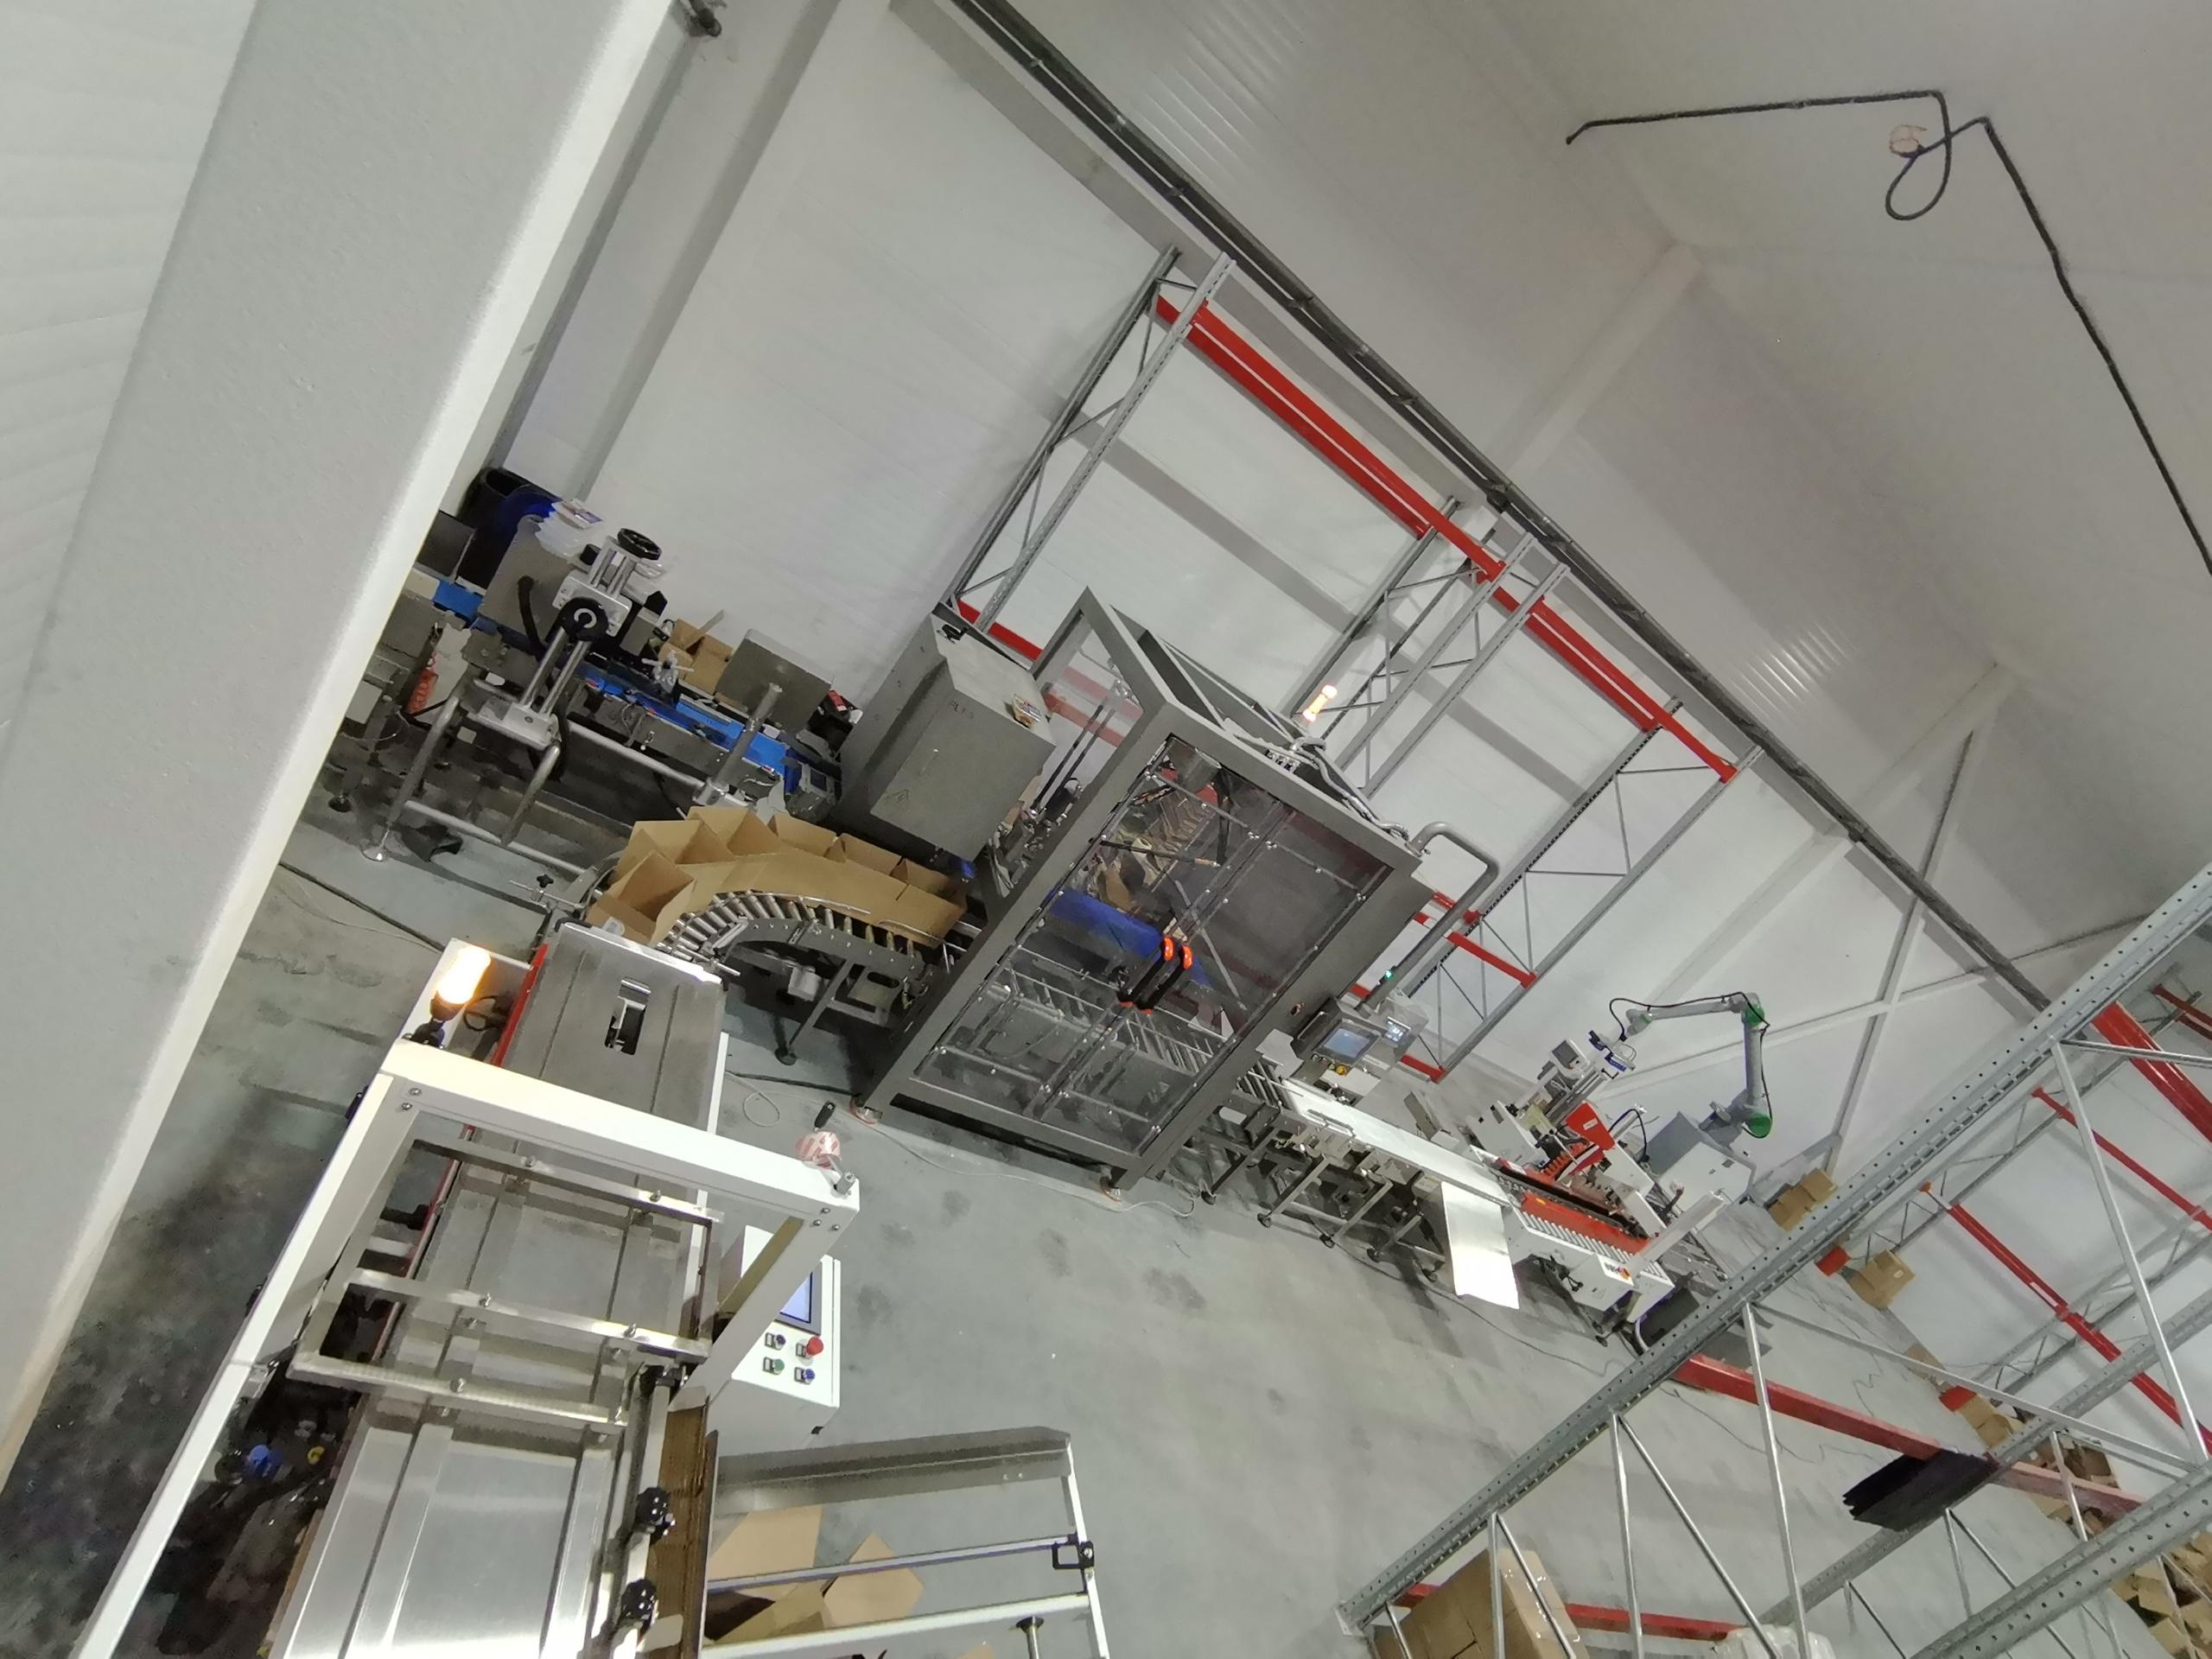
A case packing machine is an automated system designed to efficiently pack products into cases or cartons for storage, transportation, and distribution. This versatile equipment streamlines the packaging process by automatically organizing, arranging, and securing items into cases with minimal human intervention. The case packing machine serves as a critical component in modern manufacturing and logistics operations across various industries. The primary function of a case packing machine involves receiving products from a production line, arranging them in predetermined patterns, and placing them into cases or cartons. The case packing machine operates with precision timing, ensuring consistent packing density and product protection throughout the entire process. Advanced technological features include programmable logic controllers, vision systems, and robotic arms that enable the case packing machine to adapt to different product sizes and case configurations. Modern case packing machine systems incorporate several sophisticated technologies. High-speed conveyor systems transport products efficiently, while sensors detect product presence and positioning. The case packing machine integrates with existing production lines seamlessly, featuring adjustable parameters for different case sizes and product types. Robotics and automation reduce labor costs while improving consistency. Applications for a case packing machine extend across numerous industries including food and beverage, pharmaceuticals, cosmetics, consumer goods, and e-commerce fulfillment. The case packing machine handles everything from lightweight items to heavier products, making it ideal for diverse manufacturing environments. Whether packing beverages, electronics, or pharmaceutical products, the case packing machine delivers reliable performance and exceptional throughput rates for business success.
New Product Releases

Investing in a case packing machine delivers substantial operational and financial benefits that directly impact your bottom line. The most significant advantage lies in dramatically increased productivity and throughput. A case packing machine works continuously without fatigue, packing significantly more cases per hour than manual labor, resulting in faster order fulfillment and higher output capacity for your facility. Cost reduction represents another compelling advantage of implementing a case packing machine. By automating the packing process, companies substantially reduce labor expenses while minimizing packaging material waste. The case packing machine optimizes product placement within each case, reducing excess space and material consumption. Over time, these savings accumulate into meaningful financial benefits. Consistency and quality improvements distinguish a case packing machine from manual packing methods. Each case is packed identically, ensuring uniform product protection and professional appearance. This consistency reduces damage during shipping and enhances customer satisfaction. The case packing machine maintains precise packing patterns regardless of production volume or time of day. Operational flexibility represents a key advantage for businesses with diverse product lines. Modern case packing machine systems accept quick-change components, allowing rapid transitions between different case sizes, products, and configurations. This adaptability eliminates downtime and enables efficient production of multiple SKUs. Safety improvements benefit your workforce significantly. A case packing machine removes employees from repetitive, physically demanding tasks that cause strain injuries. Workers can focus on supervision, maintenance, and quality control instead of performing monotonous packing duties. Additionally, the case packing machine creates a more organized, safer work environment by eliminating congestion and injury hazards associated with manual packing operations. These advantages combine to create compelling value for modern manufacturers seeking operational excellence.

Practical Tips

Common Customer Q&A

20

Jan

Common Customer Q&A

View More
Global Collaboration, Shared Growth

20

Jan

Global Collaboration, Shared Growth

View More
Comprehensive After-Sales Service System for Peace

20

Jan

Comprehensive After-Sales Service System for Peace

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

case packing machine

Advanced Automation Technology

Advanced Automation Technology

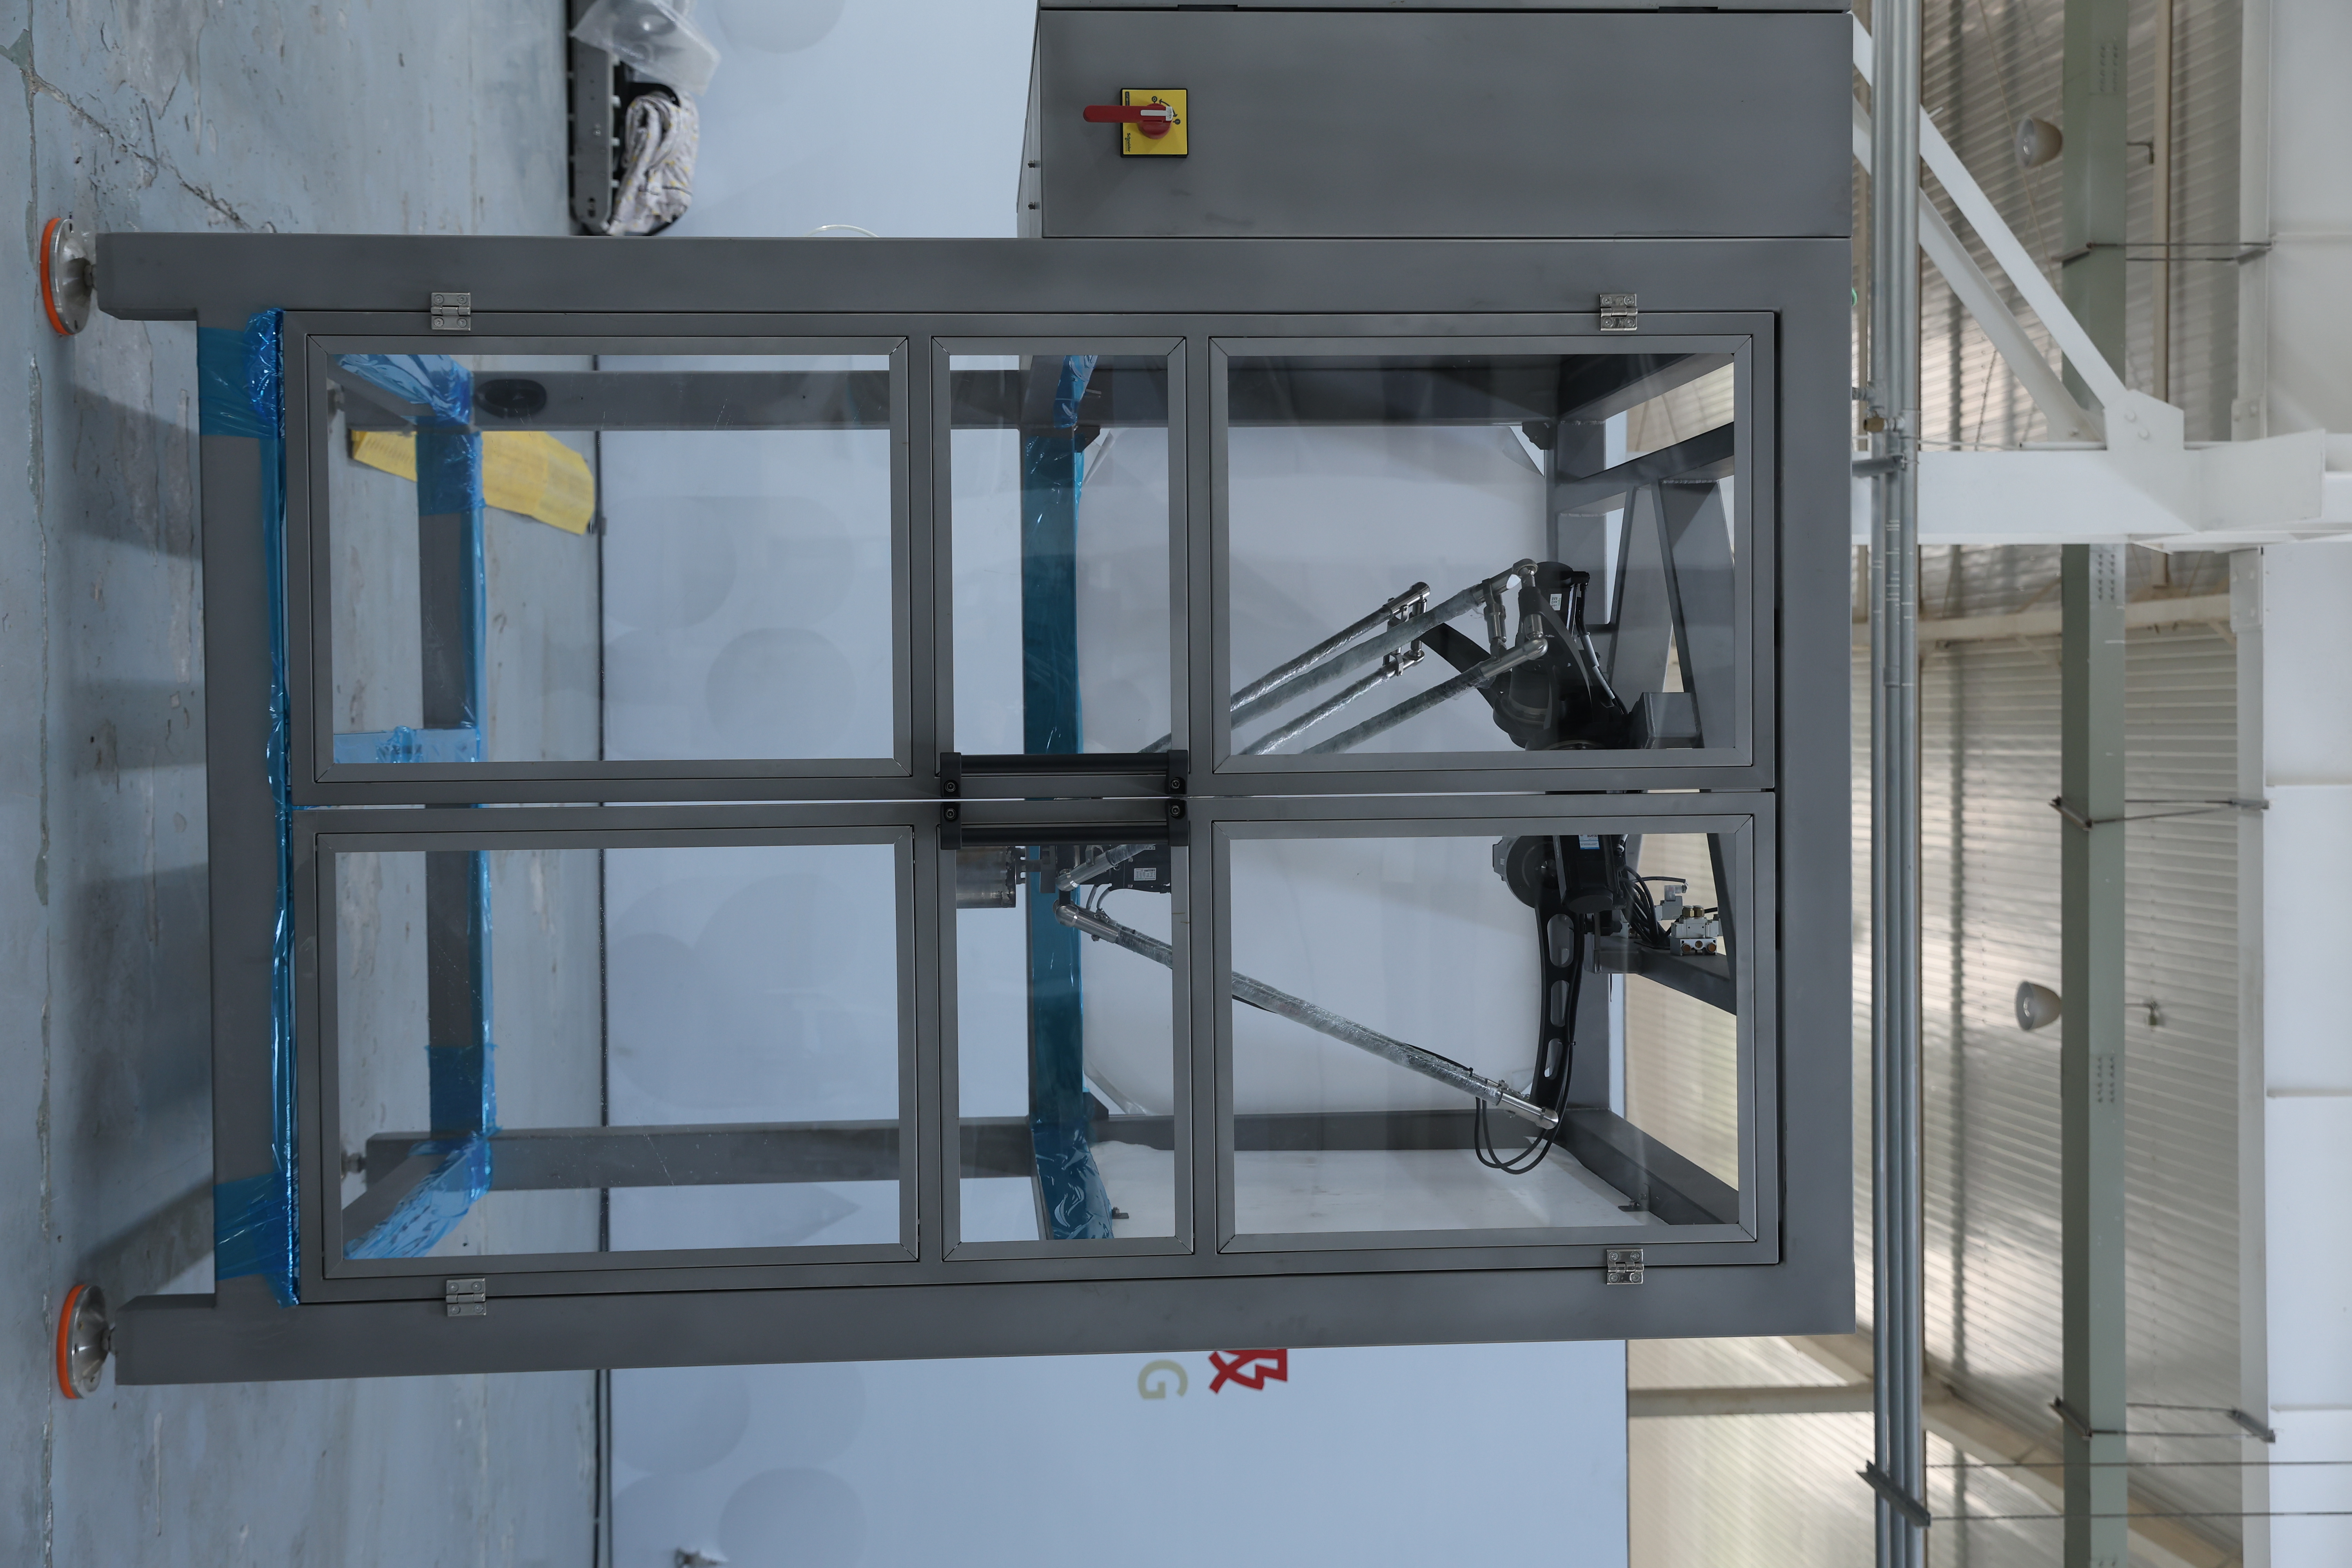
The case packing machine incorporates state-of-the-art automation technology that revolutionizes your packaging operations. Equipped with intelligent servo motors and precision sensors, the case packing machine delivers exceptional accuracy in product placement and case sealing. The case packing machine utilizes real-time monitoring systems that detect anomalies instantly, preventing defective cases from reaching customers. The technological sophistication of a case packing machine enables seamless integration with your existing production infrastructure. Programmable parameters allow operators to customize packing patterns, case configurations, and speed settings without extensive downtime. Vision systems embedded within the case packing machine verify product presence and positioning, ensuring quality standards are consistently met. This technological foundation makes the case packing machine an intelligent investment that adapts to your evolving business needs, delivering reliable performance throughout extended production runs while minimizing maintenance requirements.
Significant Cost Savings and ROI

Significant Cost Savings and ROI

Implementing a case packing machine generates immediate and long-term financial benefits that justify the investment quickly. Labor cost reduction stands as the primary financial advantage, as the case packing machine handles repetitive tasks previously requiring multiple employees working multiple shifts. The case packing machine operates continuously, delivering consistent output while reducing your permanent staffing requirements significantly. Material efficiency improvements further enhance the financial case for case packing machine adoption. Optimized product placement within cases reduces packaging material consumption, lowering per-unit costs substantially. The case packing machine minimizes product damage during packing, reducing returns and warranty claims. These combined savings create impressive return on investment timelines, typically achieved within 18-24 months depending on production volume and product type. The case packing machine transforms packaging from an expense center into a profit-generating operational improvement.
Flexibility and Scalability

Flexibility and Scalability

A case packing machine provides unprecedented operational flexibility for businesses managing diverse product portfolios and varying demand fluctuations. Quick-change tooling systems enable rapid transitions between different case sizes, product types, and configurations without requiring significant downtime or technical expertise. The case packing machine adapts instantly to production changes, supporting seasonal variations and promotional requirements effortlessly. Scalability represents another critical advantage of case packing machine technology. As your business grows, the case packing machine scales capacity without requiring complete system replacement. Modular design elements allow capacity expansion through additional modules or upgraded components. The case packing machine accommodates new product lines, expanded distribution channels, and increased customer demands seamlessly. This scalability ensures your packaging investment protects future growth while maintaining profitability across expanding operations.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000