robotic sorting system
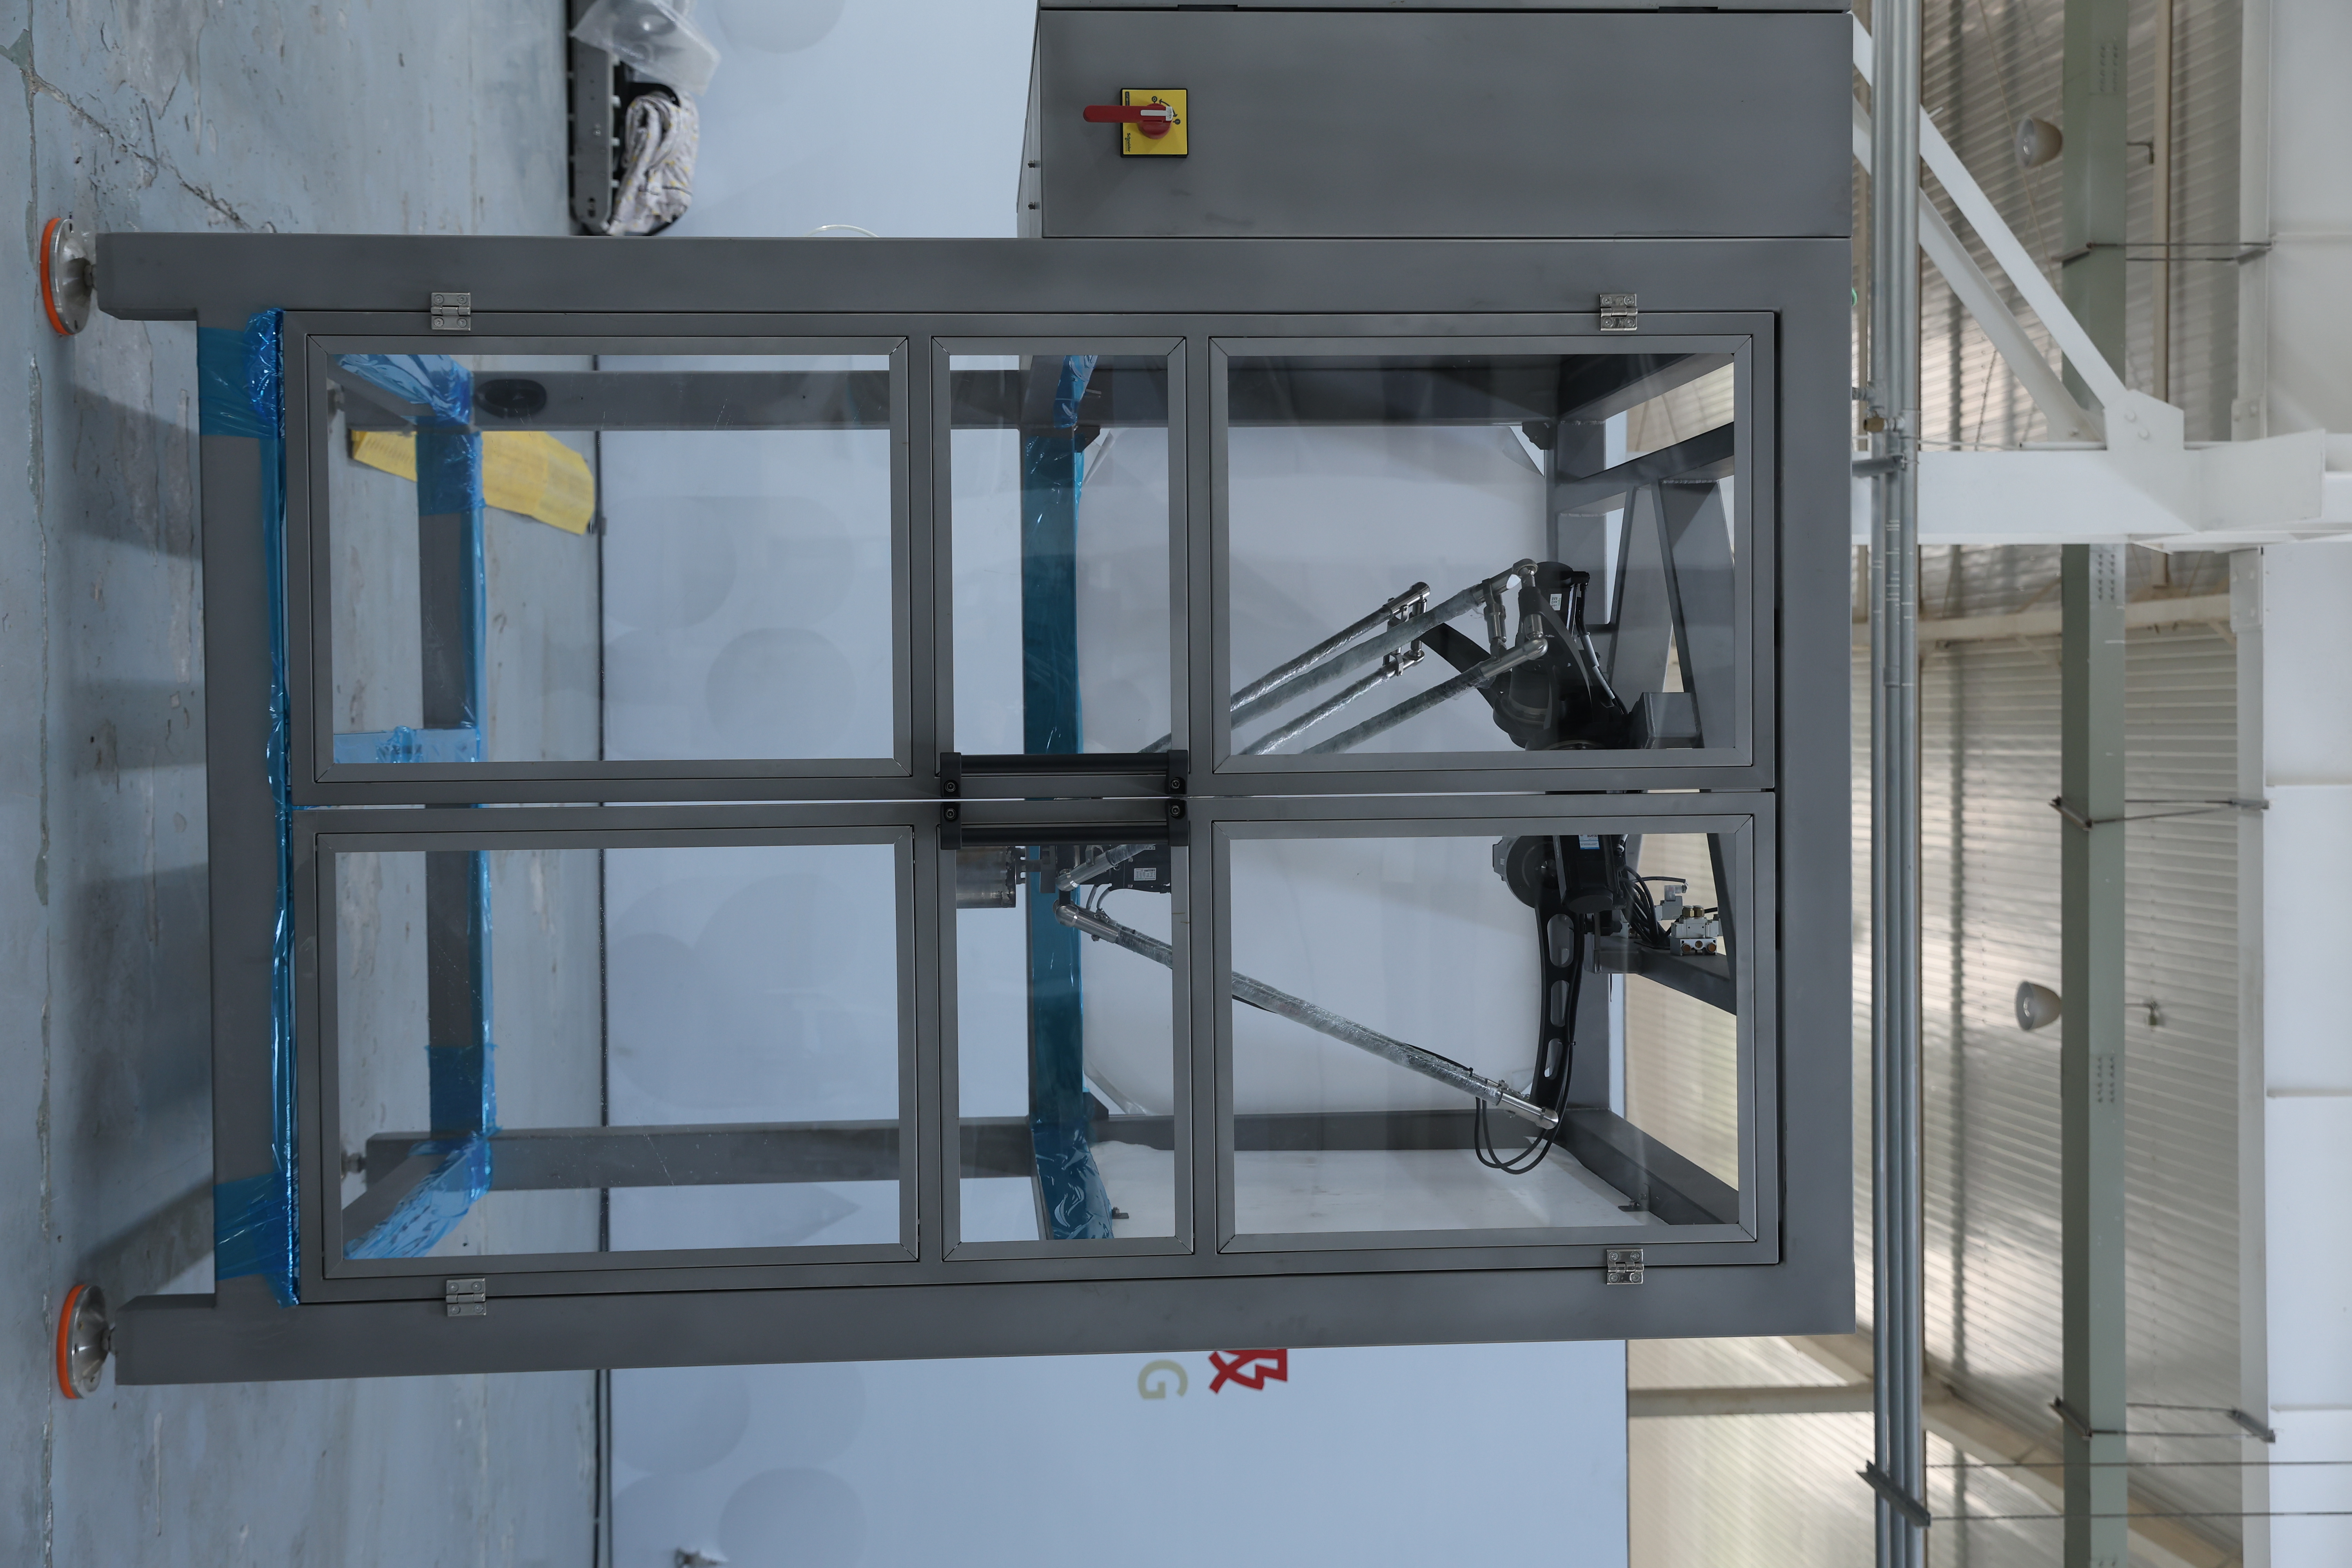
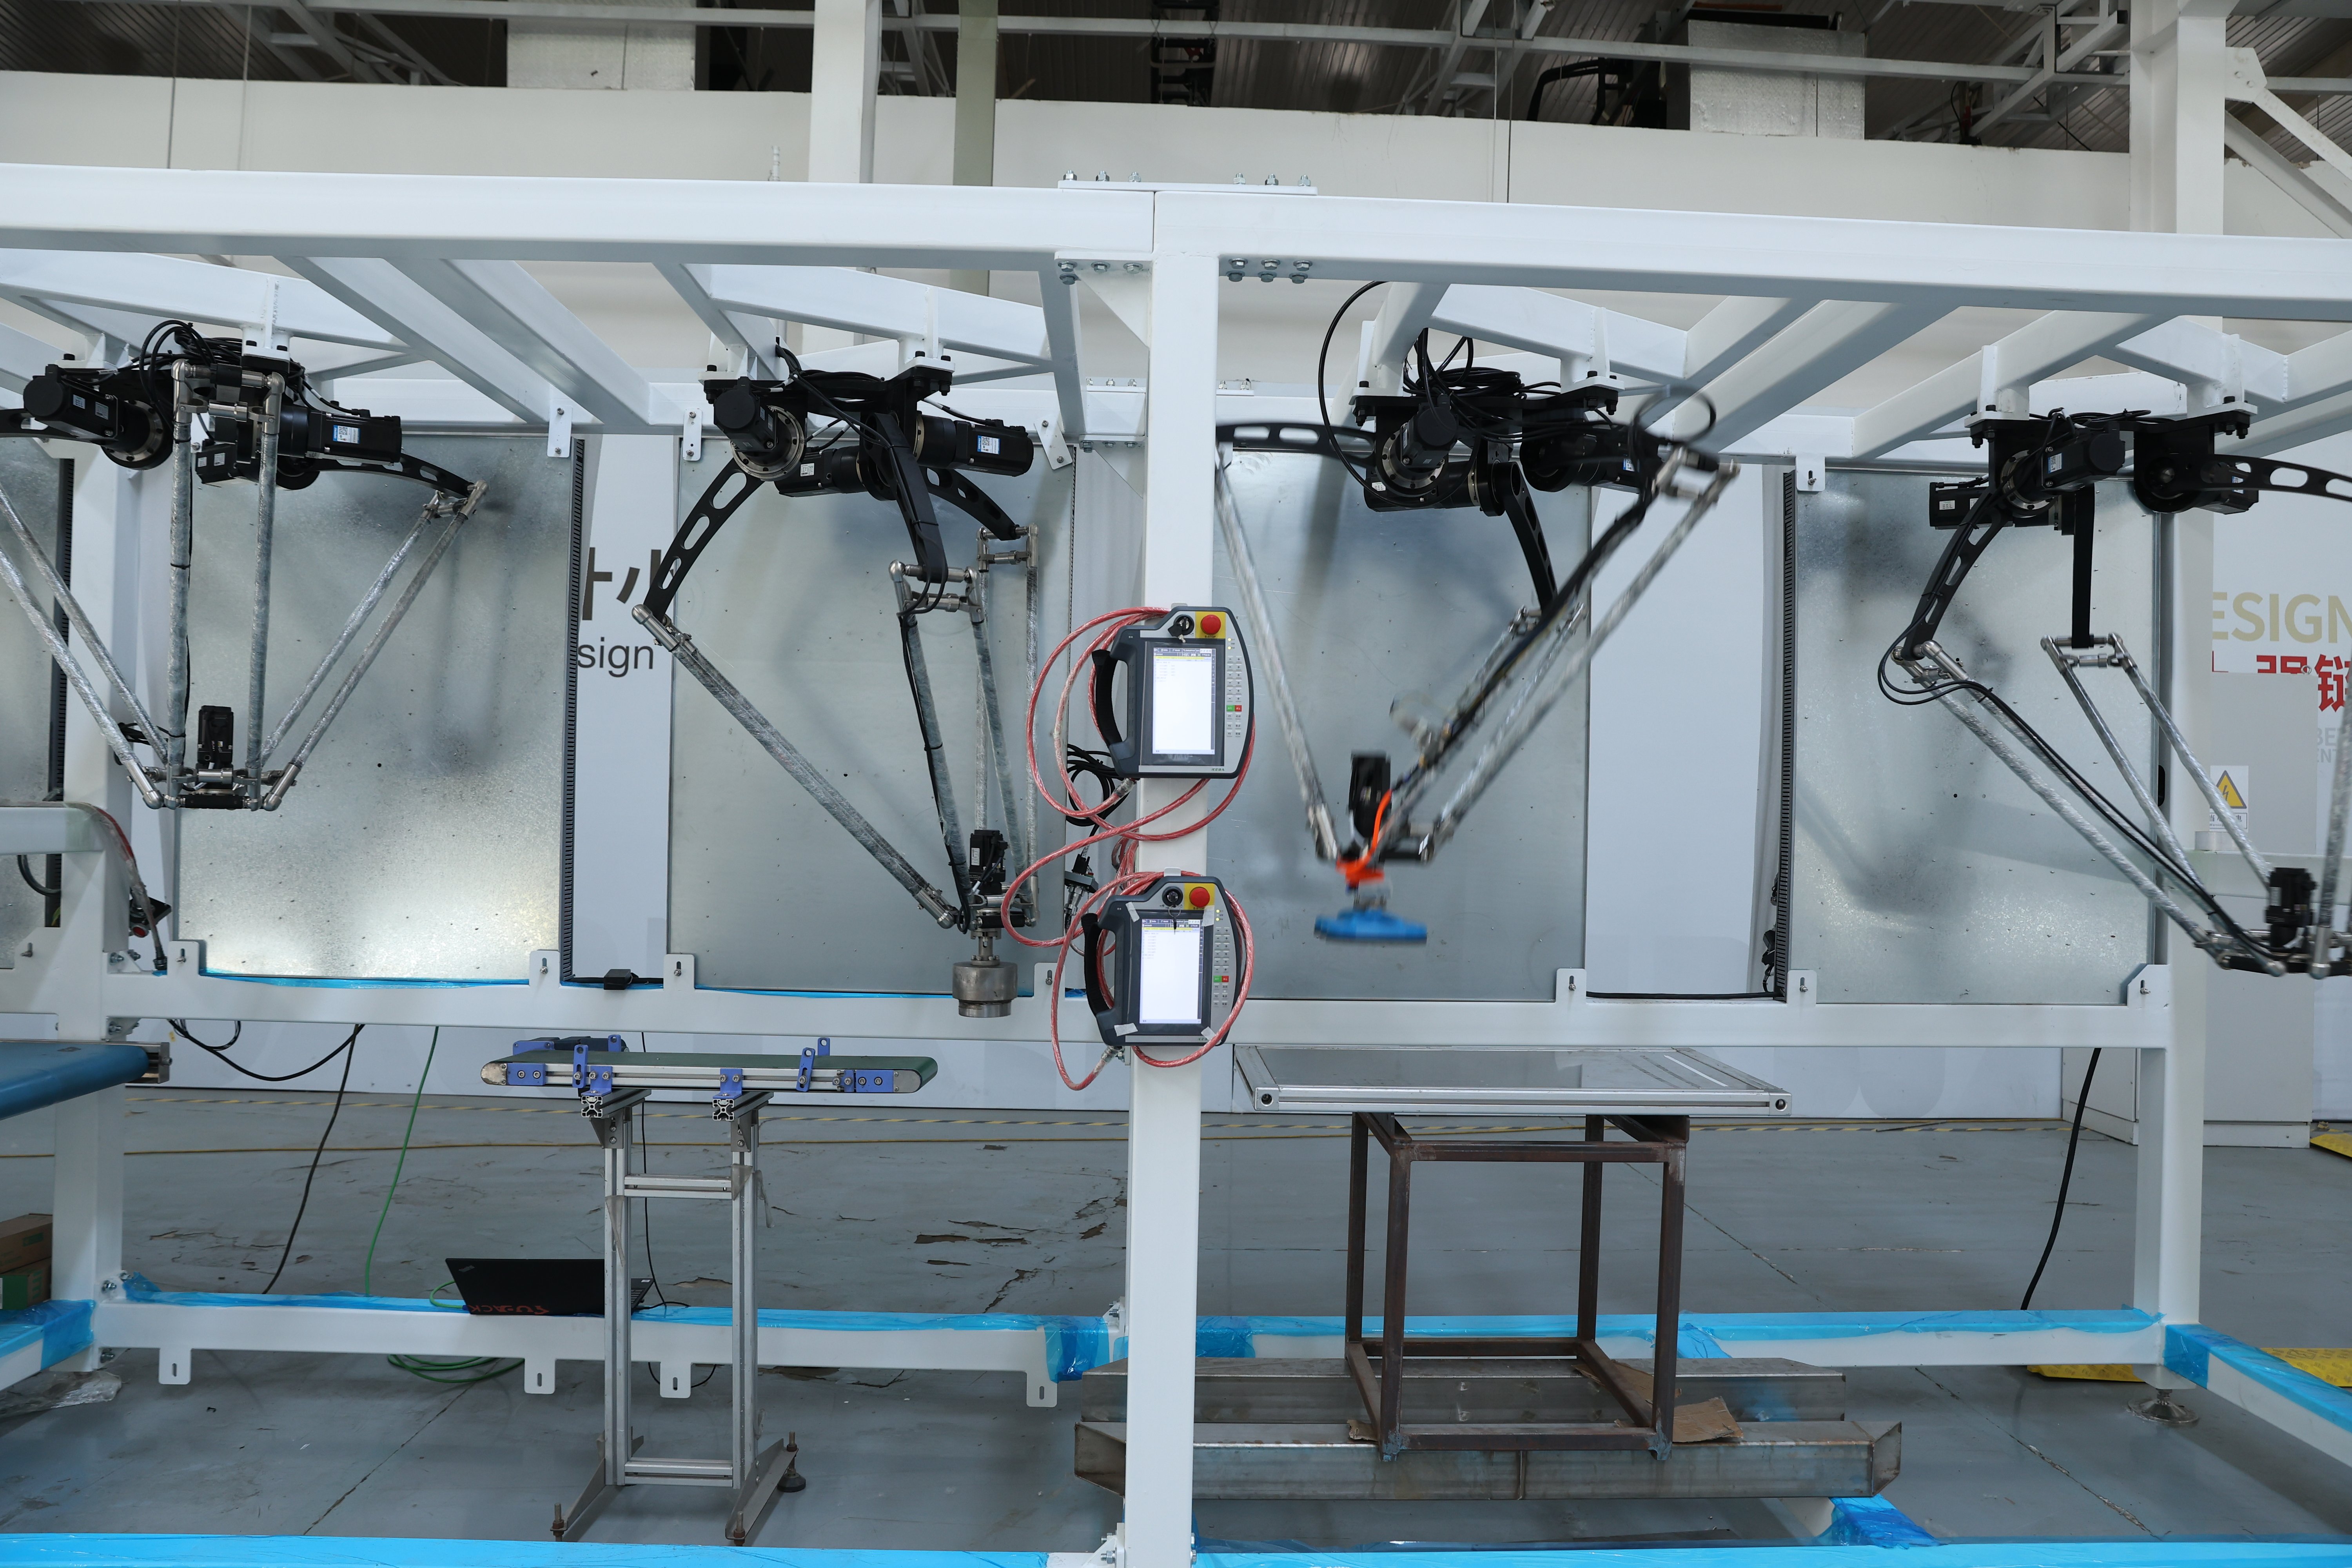
A robotic sorting system represents a transformative solution for modern material handling and logistics operations. This advanced technology uses artificial intelligence, computer vision, and mechanical automation to rapidly identify, categorize, and direct items with exceptional precision. The robotic sorting system operates by capturing detailed images of each product, analyzing its characteristics, and automatically routing it to the correct destination based on predefined parameters.
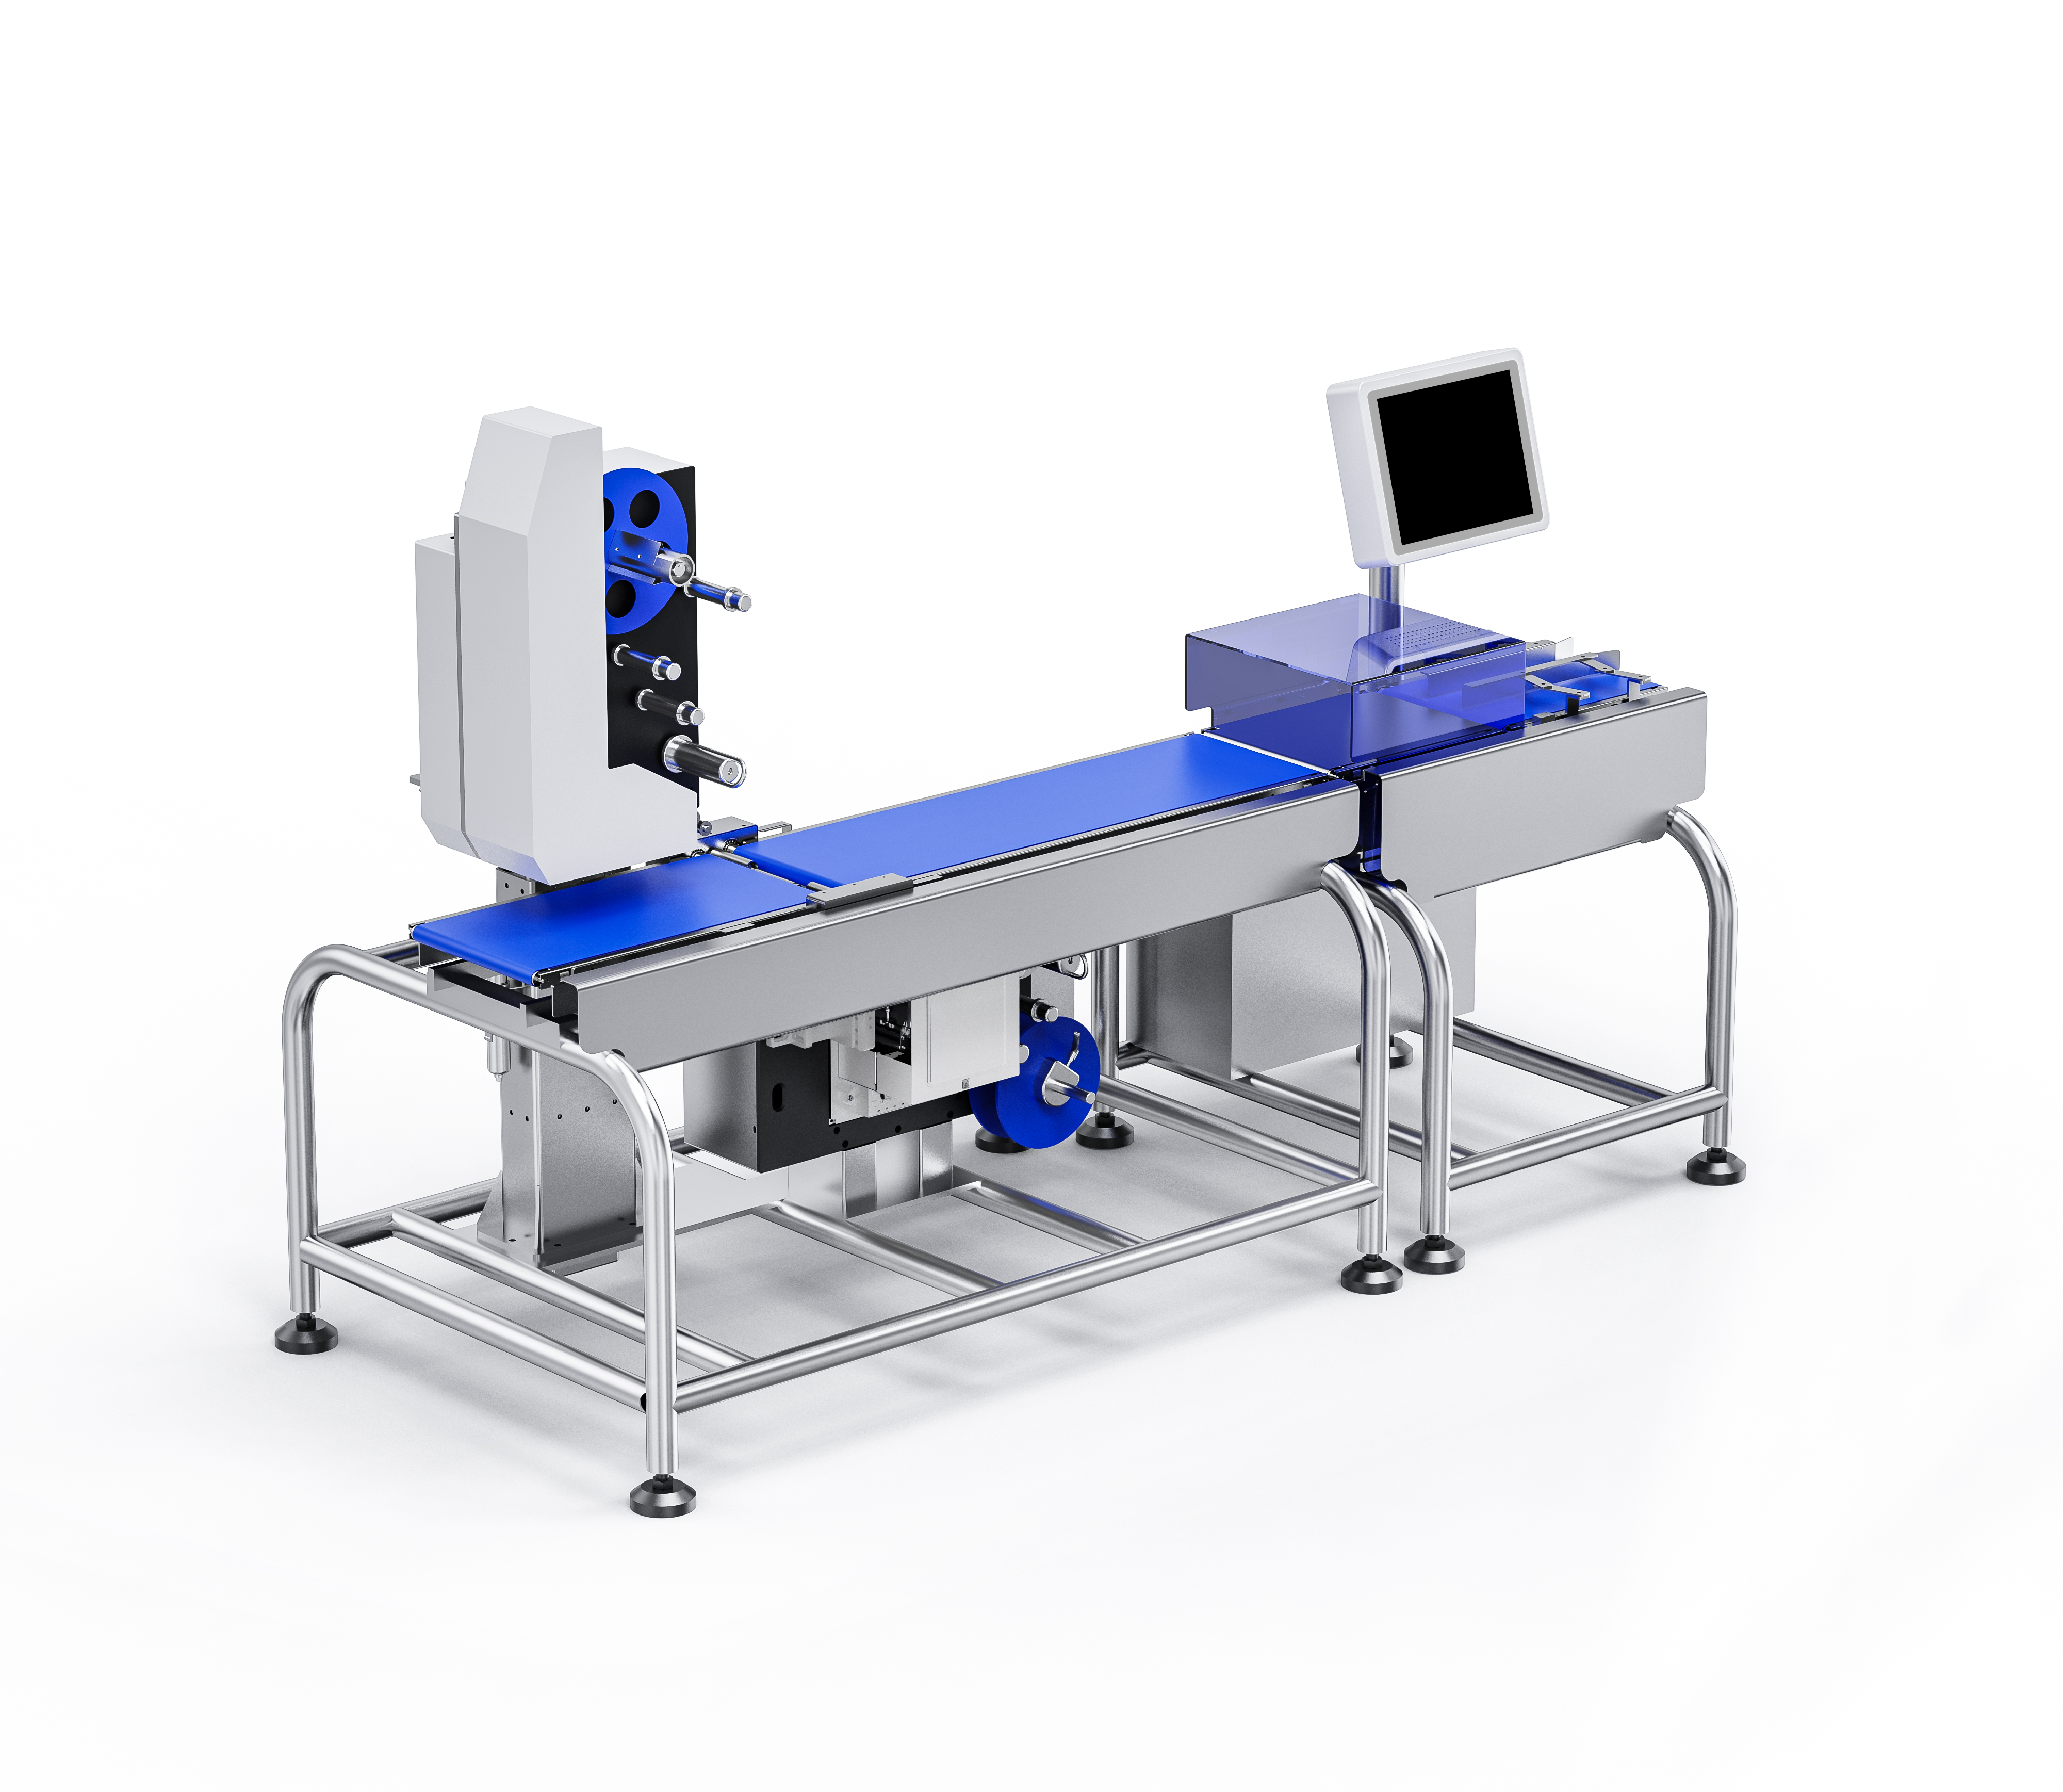
The primary functions of a robotic sorting system include high-speed item recognition, accurate categorization across multiple sorting criteria, and seamless integration with existing warehouse infrastructure. The technological features encompass machine learning algorithms that continuously improve sorting accuracy, real-time data analytics dashboards, and adaptive mechanisms that handle diverse product shapes and sizes. These systems utilize conveyor belt integration, pneumatic or mechanical diverters, and intelligent control software to manage complex sorting operations efficiently.
Applications for the robotic sorting system span numerous industries, including e-commerce fulfillment, postal and parcel services, recycling facilities, food processing, and pharmaceutical distribution. The robotic sorting system excels in environments requiring speed, accuracy, and consistency. Organizations implement these systems to process thousands of items hourly while maintaining minimal error rates. Whether sorting packages by destination, segregating products by type, or organizing items for quality control, the robotic sorting system delivers reliable performance that significantly outpaces traditional manual sorting methods.

 EN


