packaging conveyor systems
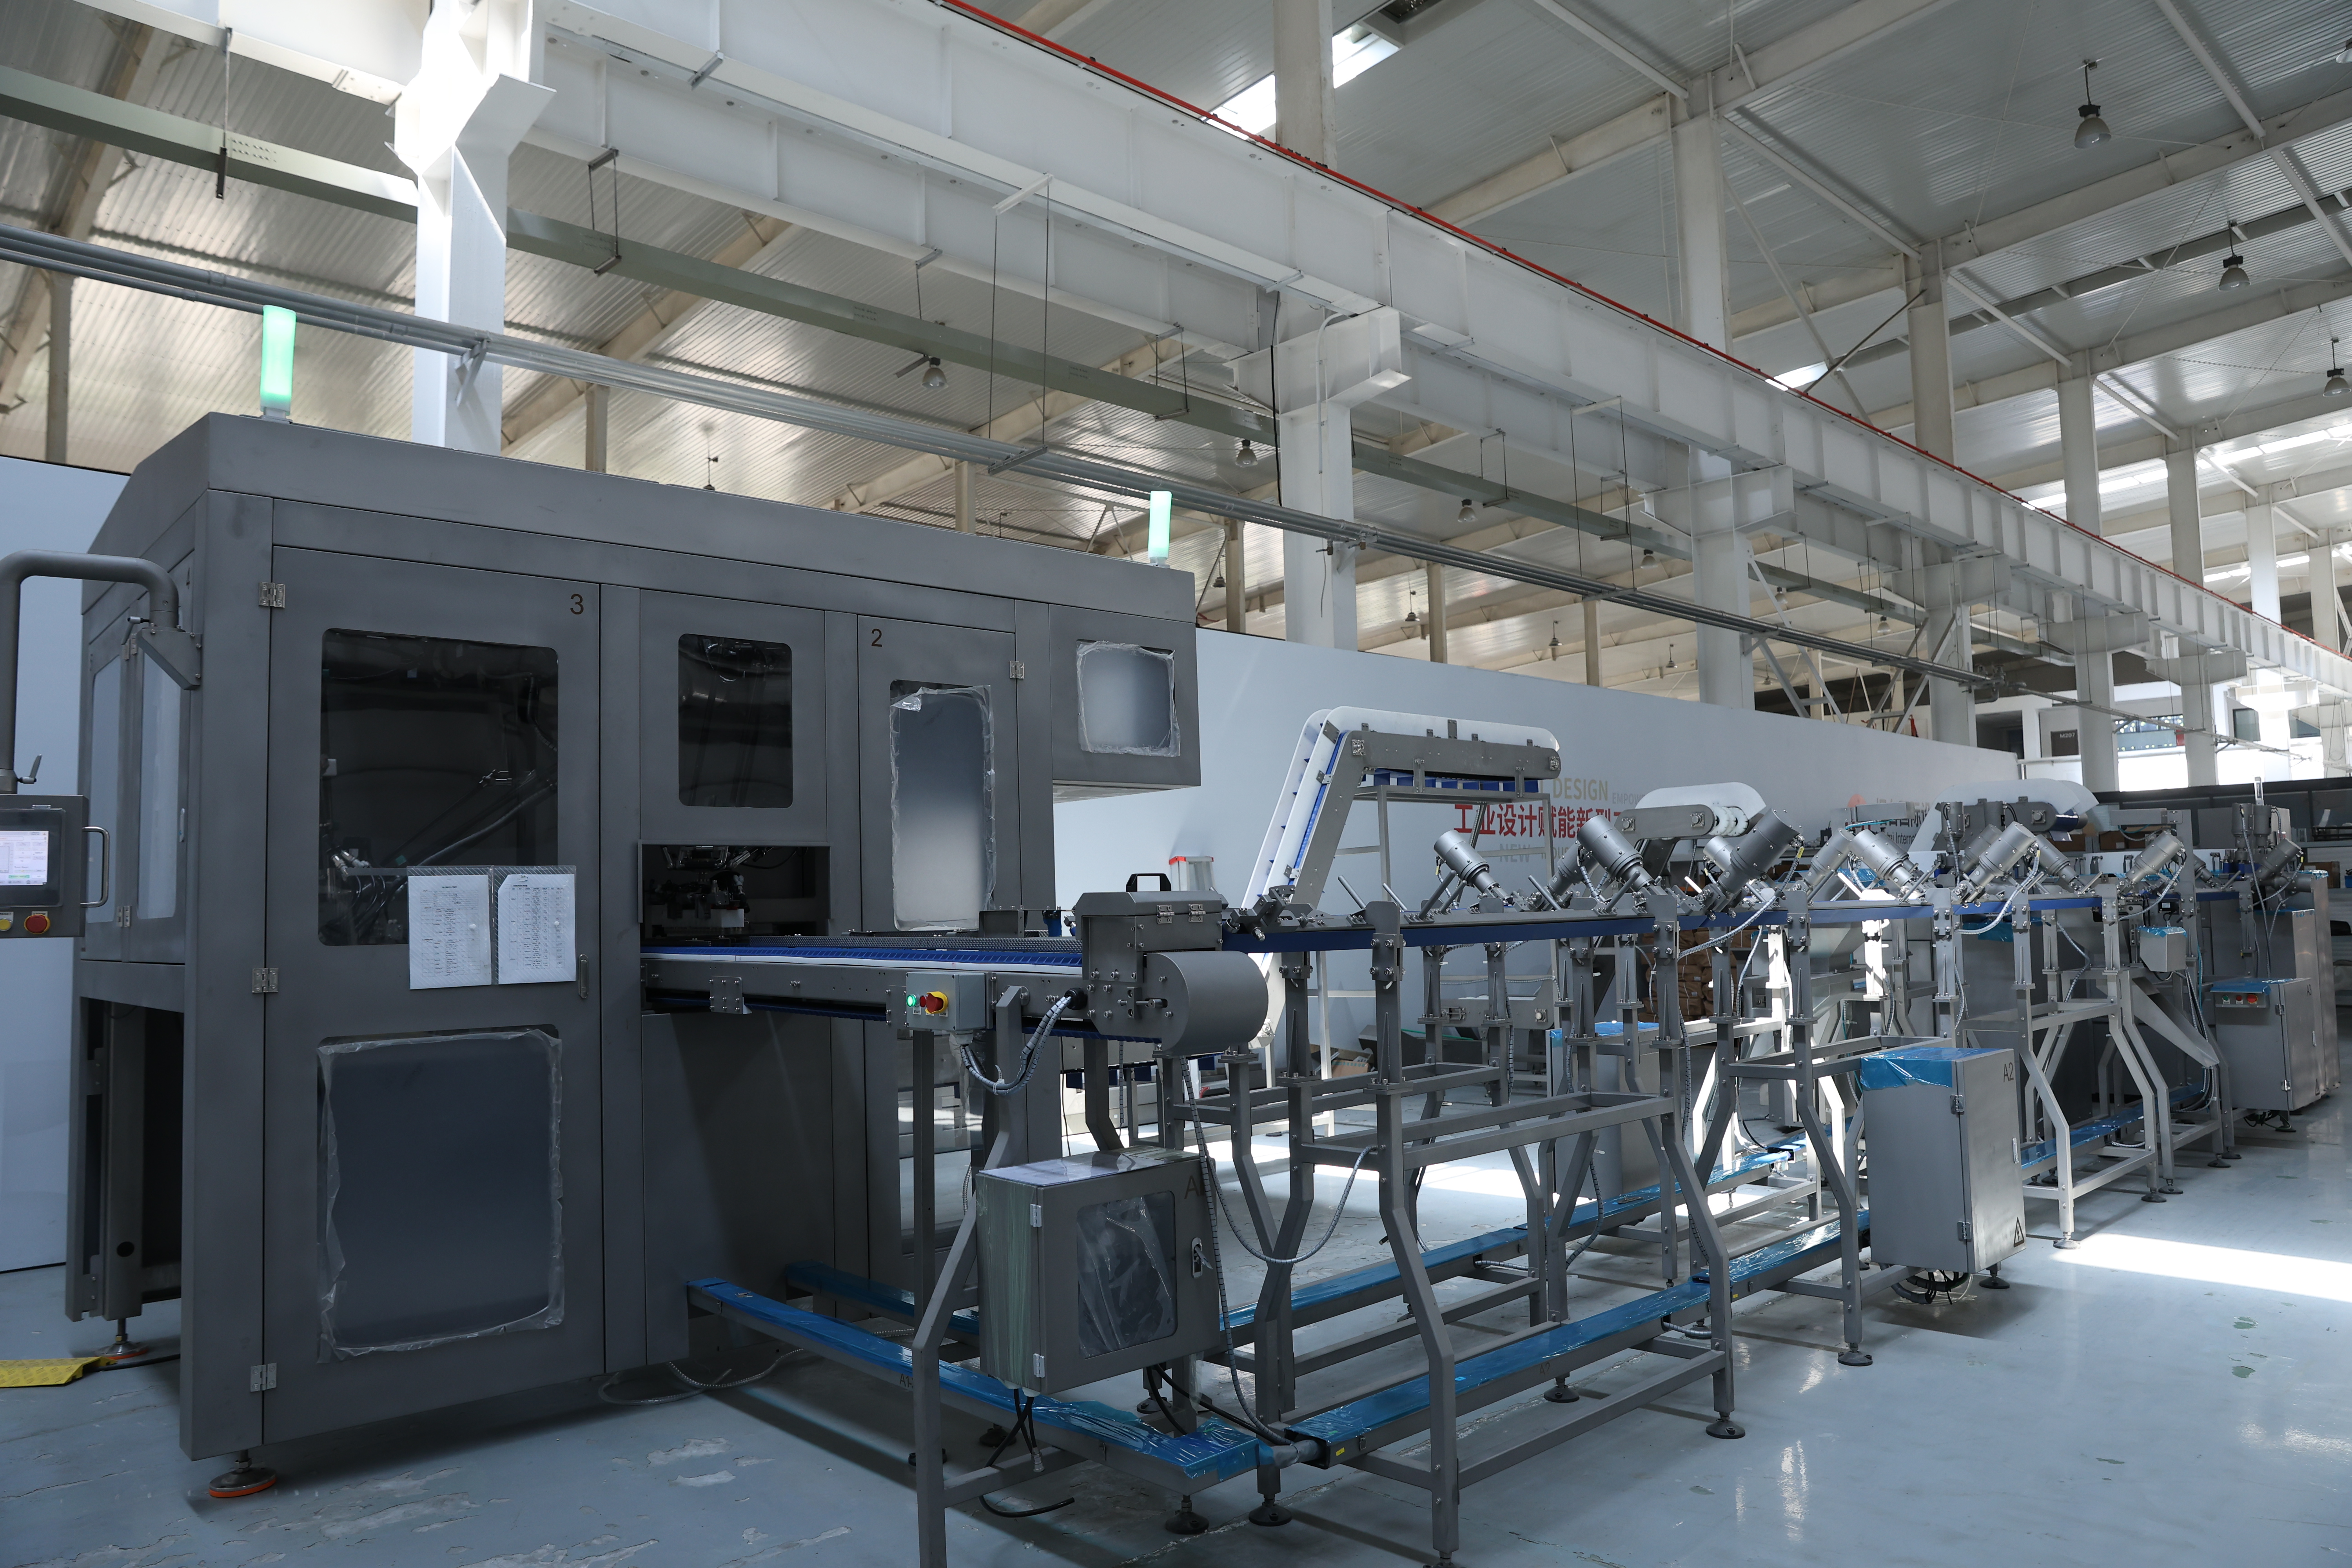
Packaging conveyor systems represent essential machinery designed to streamline the movement and processing of products through manufacturing and distribution facilities. These packaging conveyor systems automate the transportation of items from one station to another, significantly improving operational efficiency. The primary function of packaging conveyor systems involves moving products safely and consistently along predetermined paths while maintaining speed and precision throughout the packaging process.
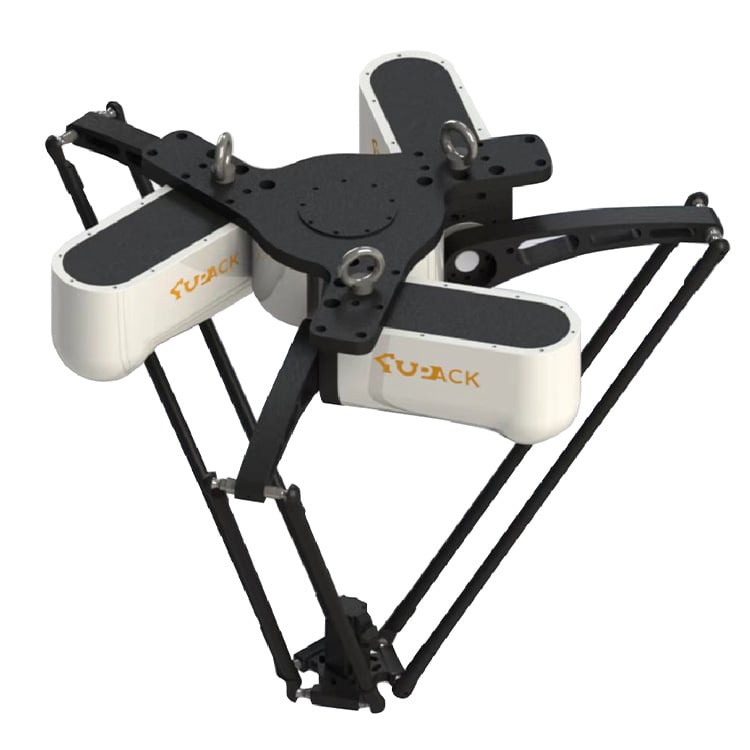
Modern packaging conveyor systems incorporate advanced technological features that enhance their performance and reliability. These systems utilize motorized rollers, belt mechanisms, and intelligent control systems to manage product flow automatically. Packaging conveyor systems employ sensors and automation technology to detect products, adjust speeds, and prevent collisions or jams. The integration of smart controls allows operators to monitor and adjust settings in real-time, ensuring optimal performance.
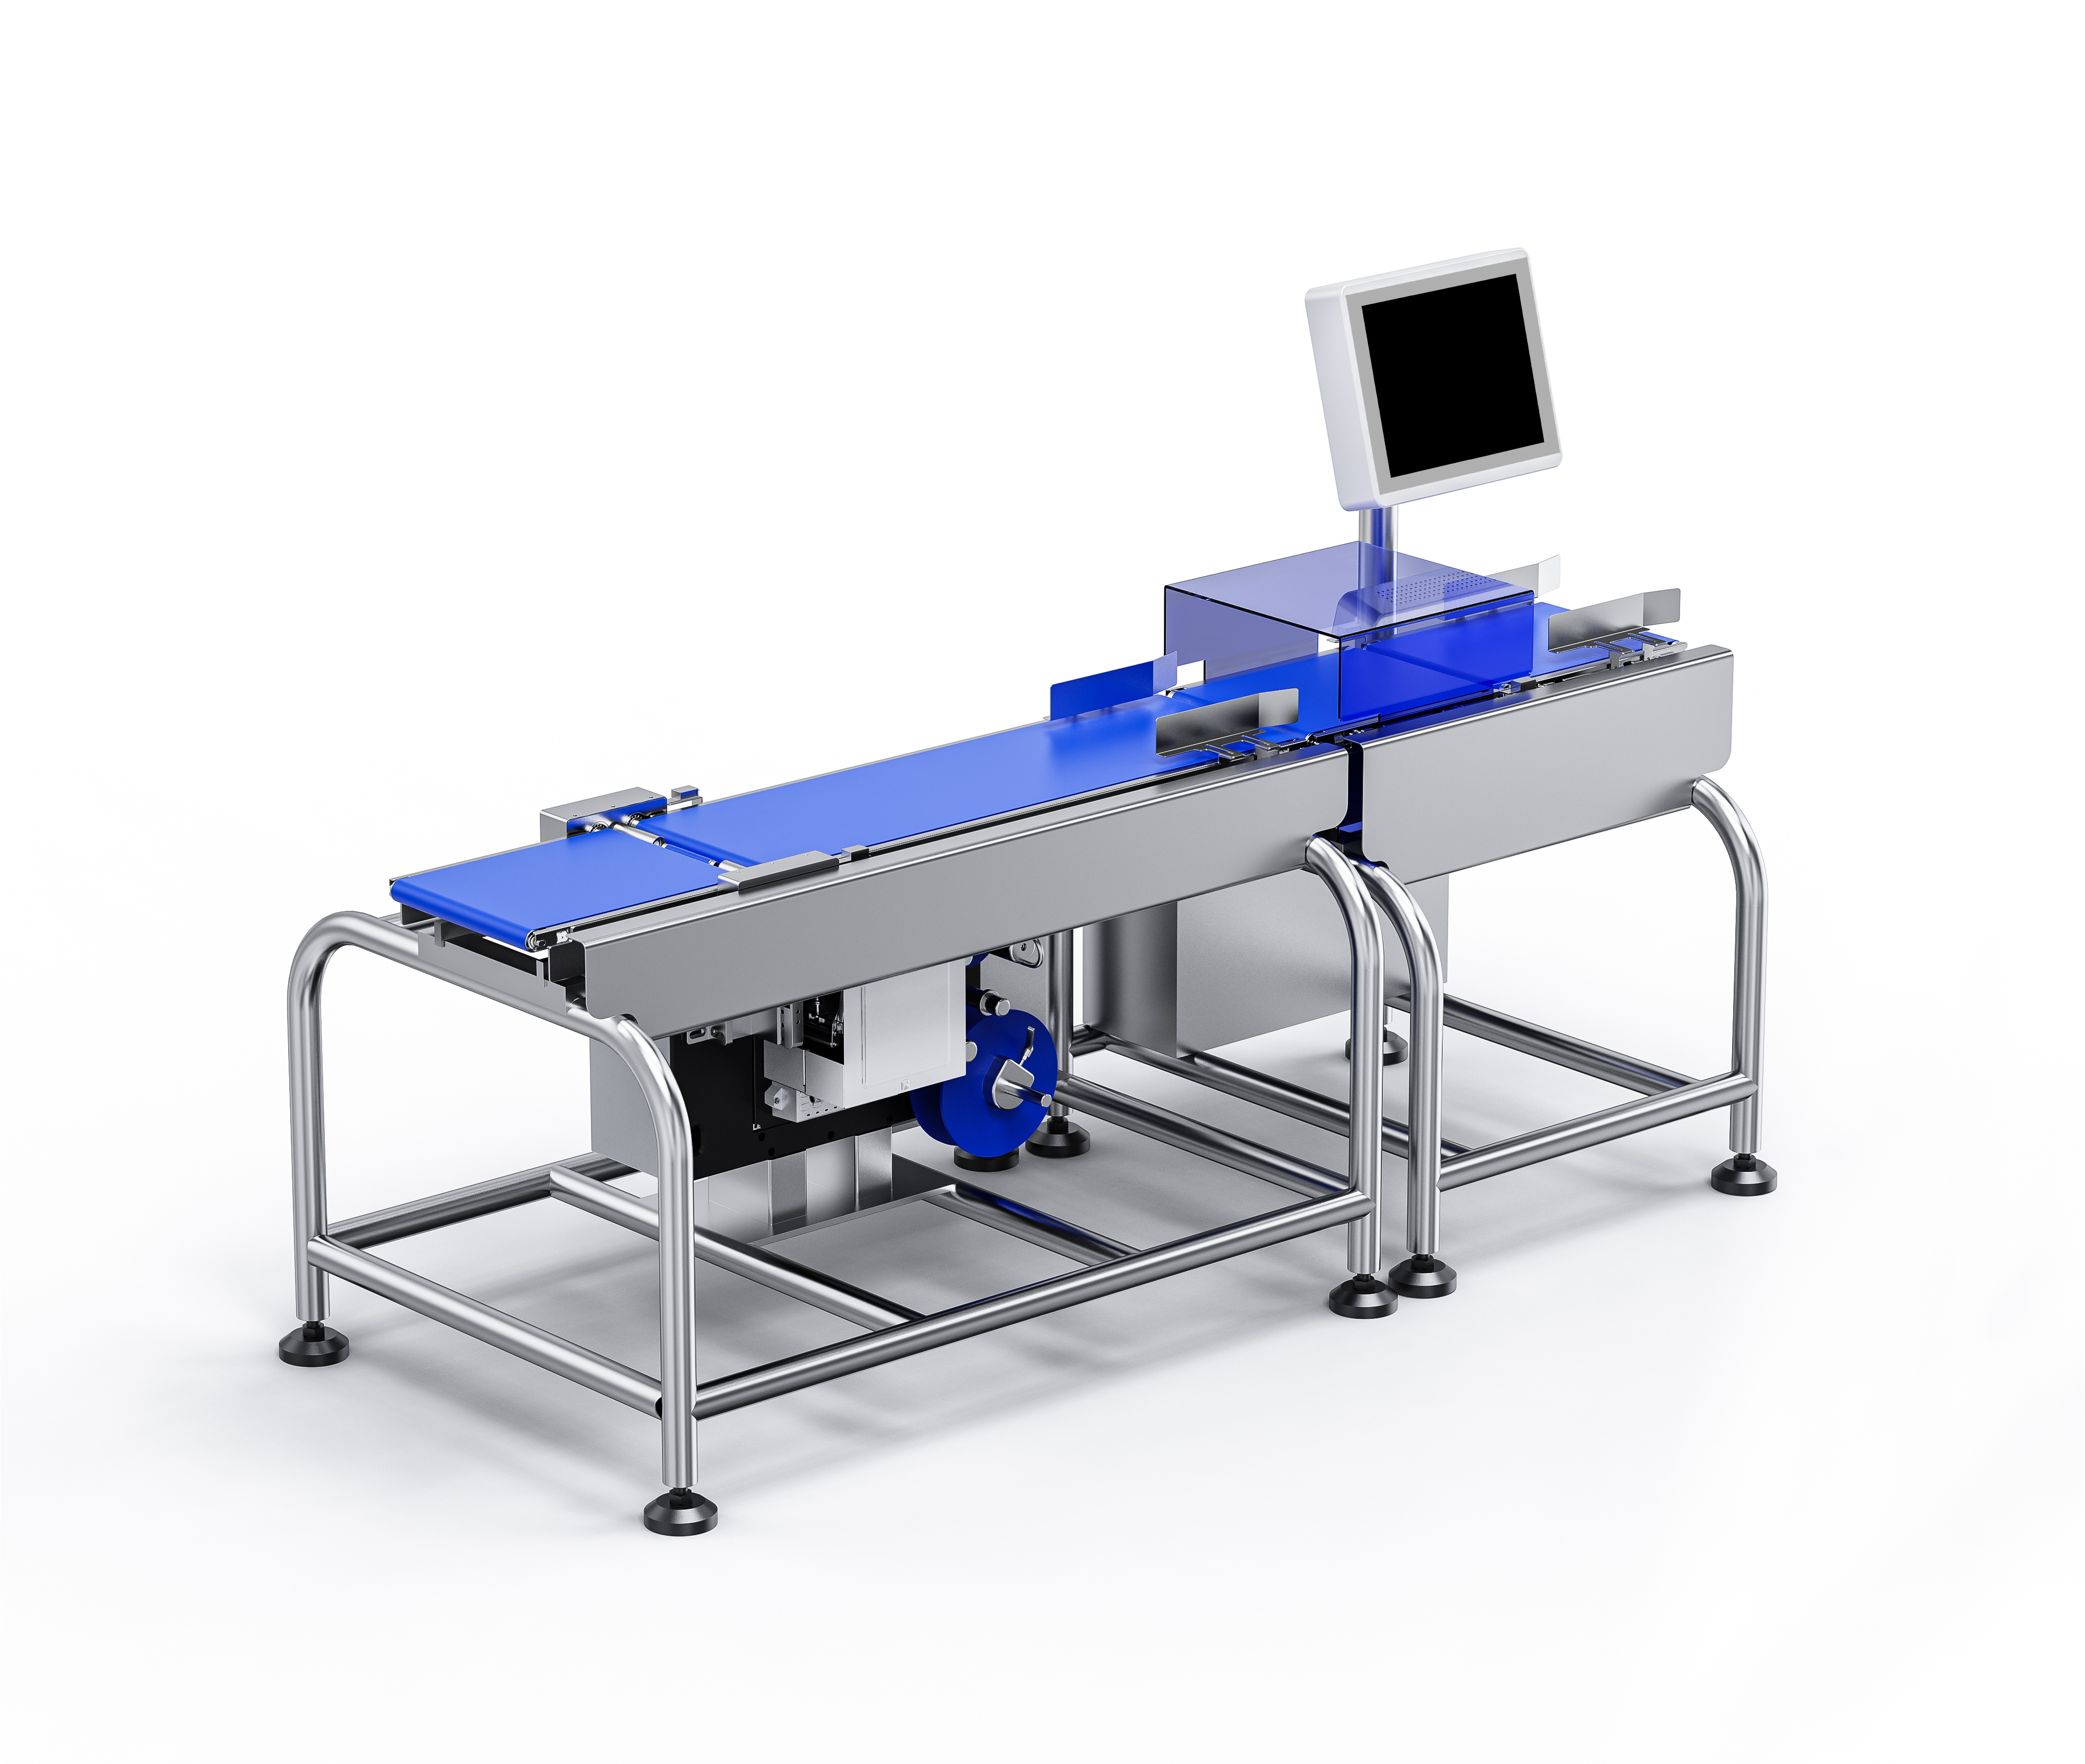
Applications for packaging conveyor systems span numerous industries including food and beverage, pharmaceuticals, consumer goods, and e-commerce fulfillment. These systems handle diverse product types, from fragile items to heavy containers. Packaging conveyor systems serve critical roles in sorting, labeling, palletizing, and transporting products. Whether businesses require simple linear conveyor setups or complex modular configurations, packaging conveyor systems provide scalable solutions that adapt to specific operational requirements and production volumes.

 EN


